No heat-affected zone
Mechanical cut preserves the parent metallurgy — safe for sour service, stainless, duplex and Inconel.

Every machine here is built in our Shenzhen workshop and shipped factory-direct. Cold-cutting beveling, facing, cutting and orbital welding equipment — engineered to ASME, API and EN standards. Browse the family that fits your application, or send your spec and we will recommend the matching unit within one working shift.
A tungsten-carbide tool cuts the bevel, face or seam — leaving the parent metallurgy intact. The same principle runs through all ten families.
Mechanical cut preserves the parent metallurgy — safe for sour service, stainless, duplex and Inconel.
Eliminates the hot-work permit on offshore platforms, operating refineries and Zone 1 / 2 environments.
V, Y, J and compound bevels to ASME B16.25, EN ISO 9692-1 and API 1104 — first part to last.
Sealed drives, IP-rated cabinets and split-frame assembly for in-situ work on installed lines.
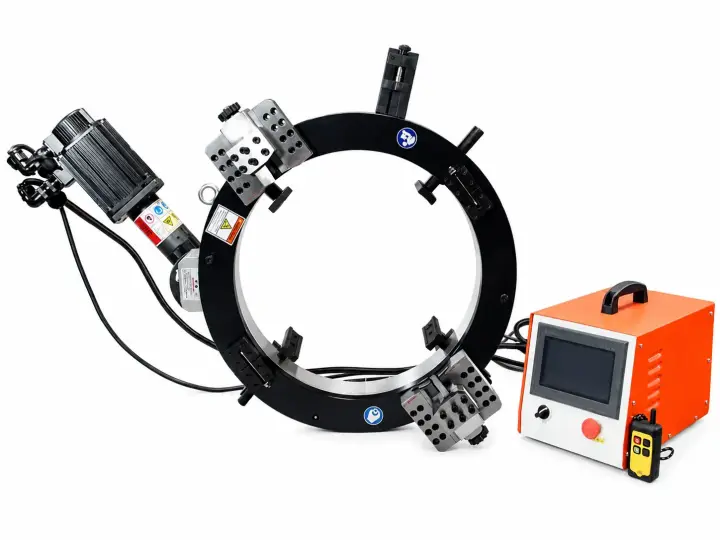 7 models
On-site V/J bevels for pipeline construction
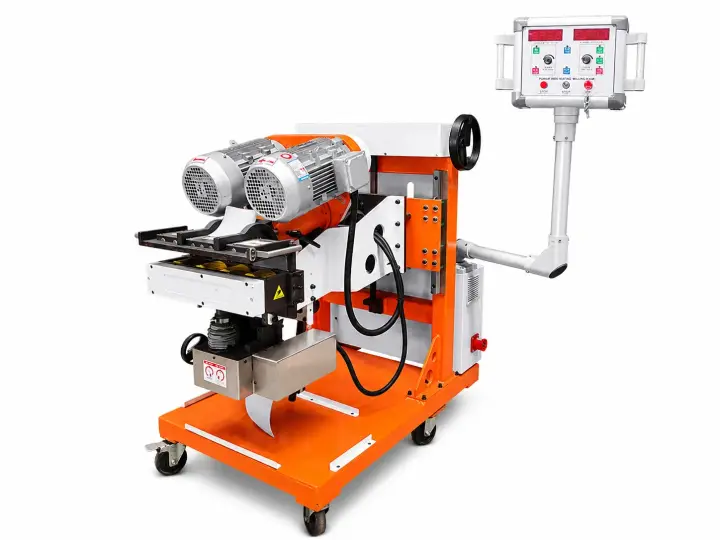 12 models
Edge milling for shipbuilding & heavy fabrication
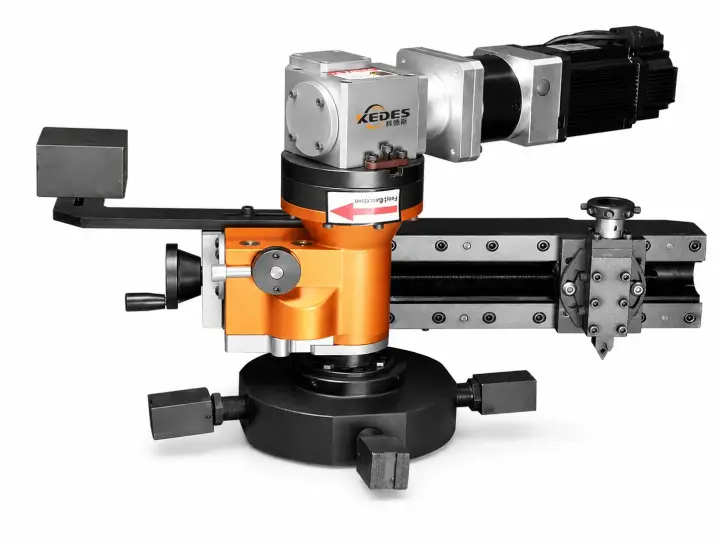 1 model
In-situ flange sealing-face refurbishment
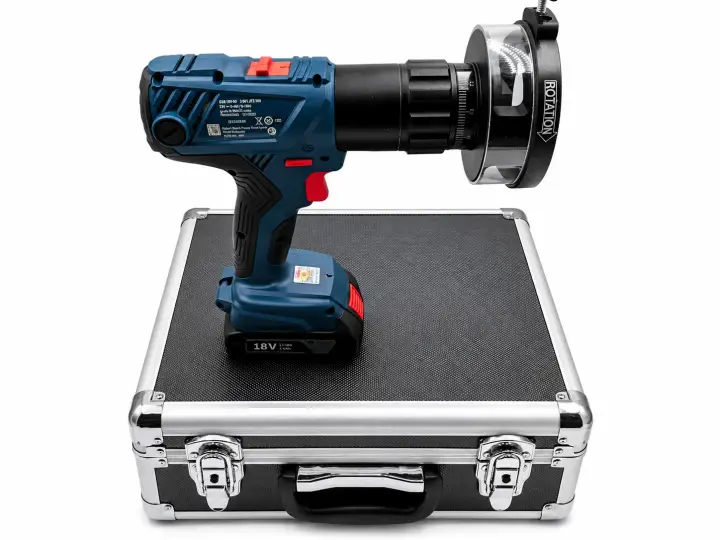 3 models
End squaring for orbital / sanitary welding
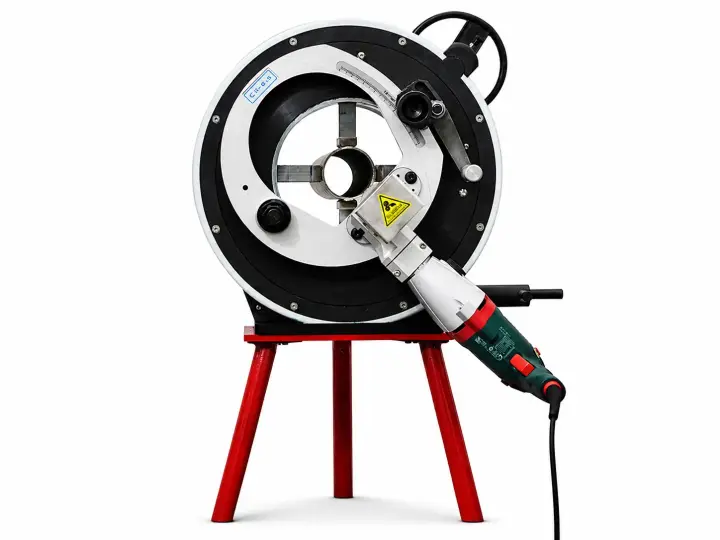 2 models
Cold cutting — no HAZ, no distortion
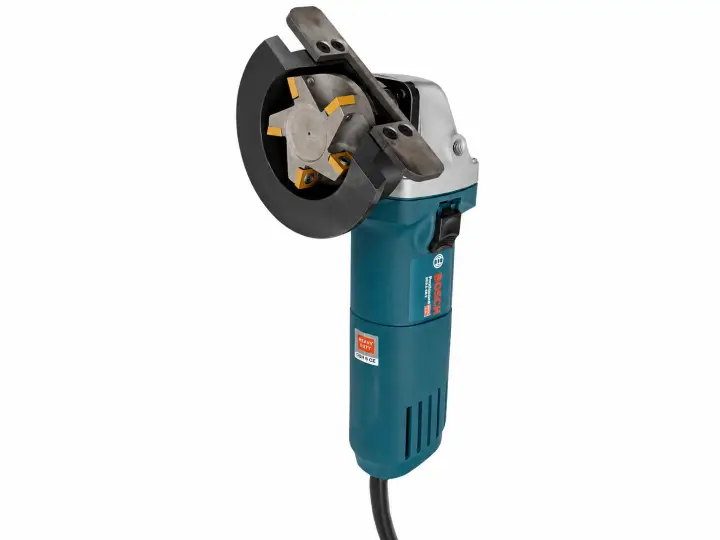 1 model
Flush reinforcement without grinding
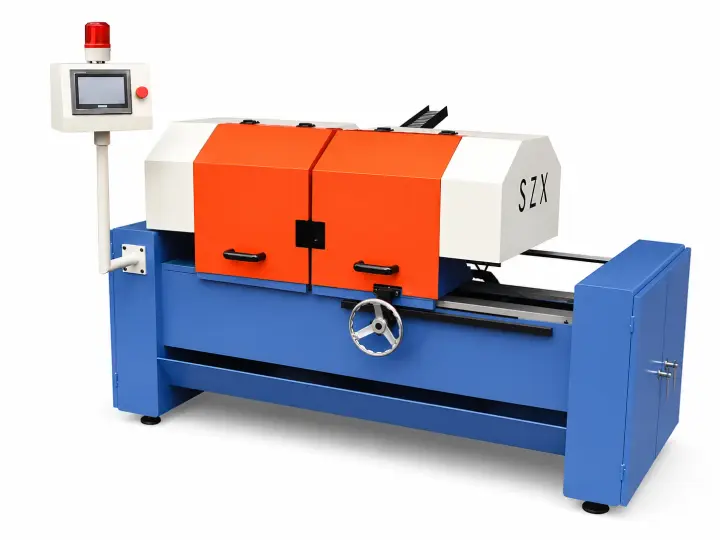 2 models
High-speed production chamfering
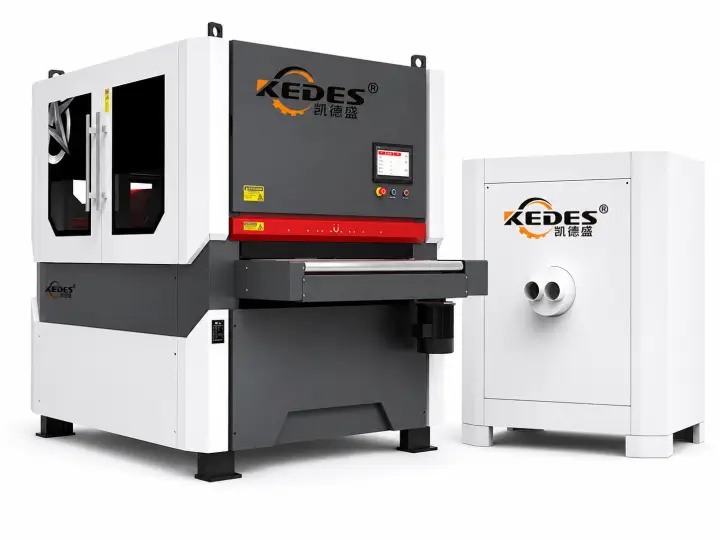 2 models
Deslag laser / plasma cut parts
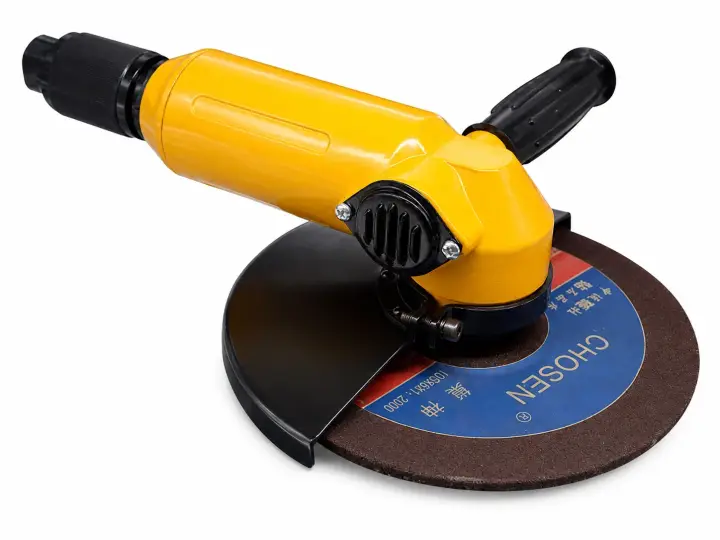 9 models
Air-driven grinding & assembly tools
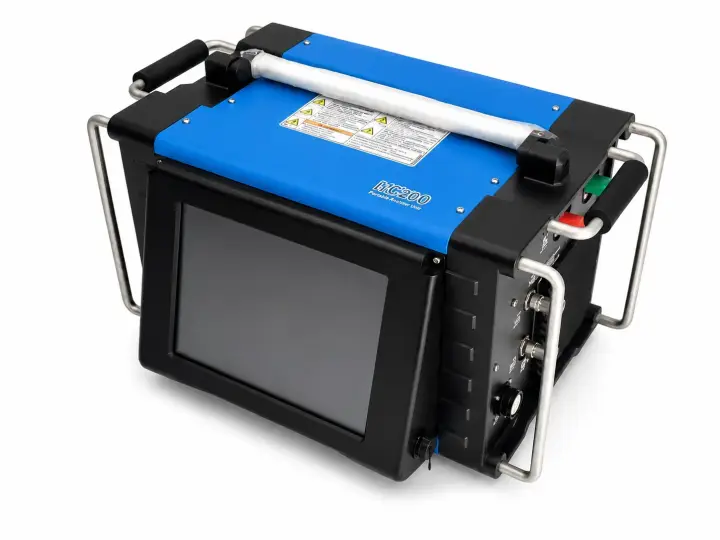 1 model
M200 series — air- & water-cooled closed heads
A starting point if you are evaluating a class of machine. Full ranges live on each family page.
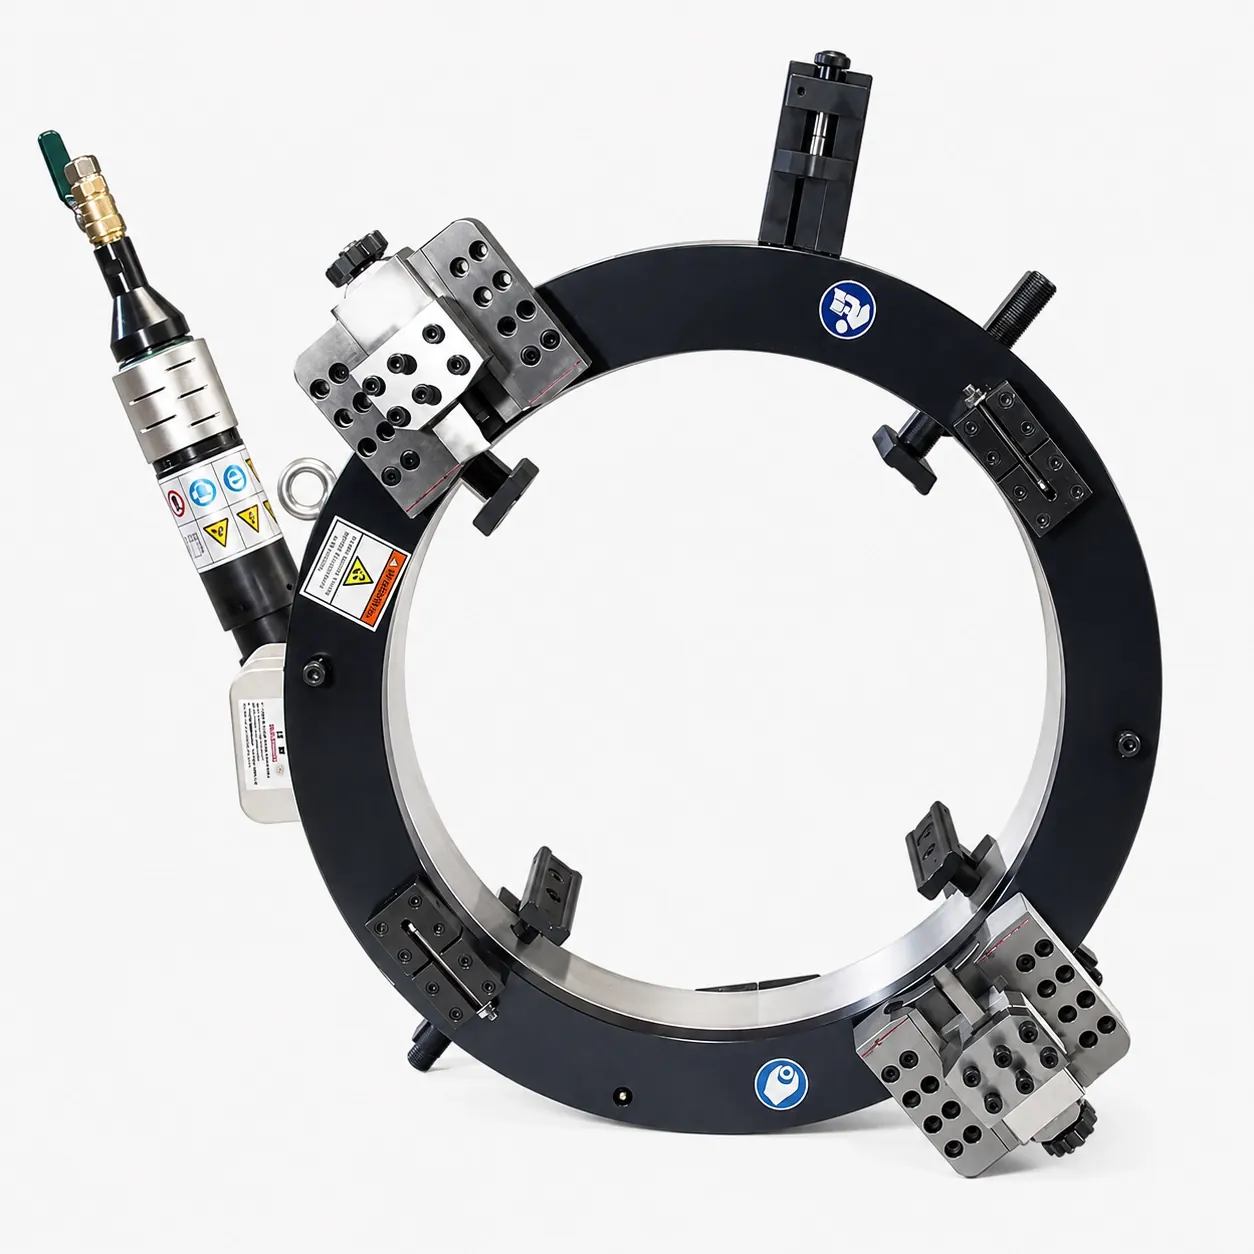
OD-mounted split-frame (clamshell) cold cutter and beveler for in-situ pipe Ø 25 – 1230 mm (3/4" – 48"), 20 sizes. Light and compact with a small radial footprint — the two-piece frame closes around installed pipe and parts and bevels it in a single pass, with no heat-affected zone. Electric (OCE) or pneumatic (OCP) drive for wall ≤ 35 mm; hydraulic (OCH) for heavy wall up to 150 mm and pipe beyond Ø 1230 mm.
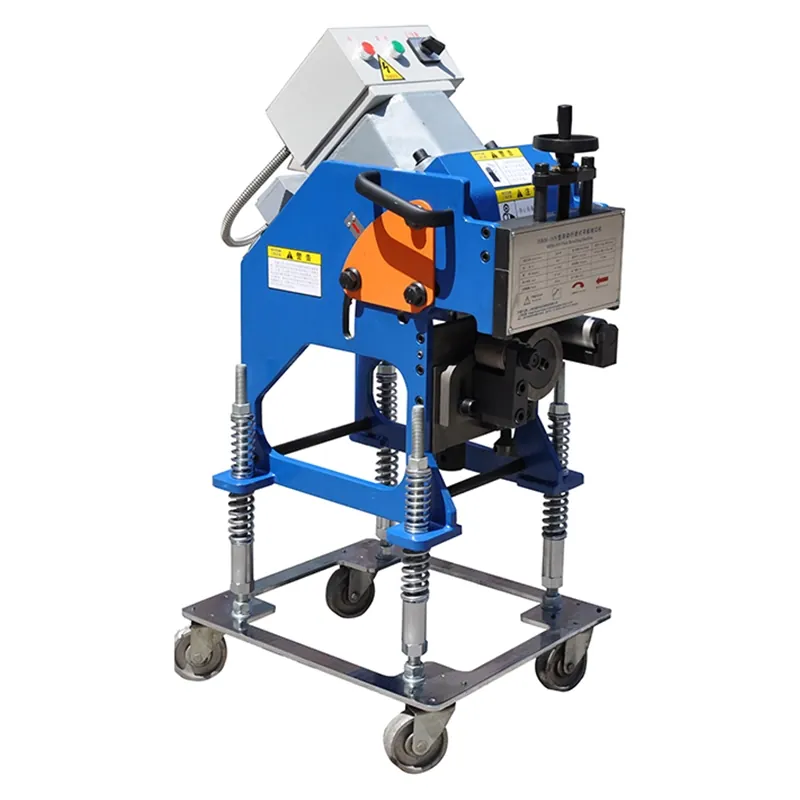
Self-propelled cold-shear plate beveler that uses a rotating shear disc instead of a milling cutter — beveling speed 2.0 – 3.0 m/min, roughly 4 – 8× faster than carbide-insert milling on equivalent plate. Lowest consumable cost in the line (one wear disc, no inserts). Standard tool for high-volume V-bevel preparation in steel-construction and shipbuilding.
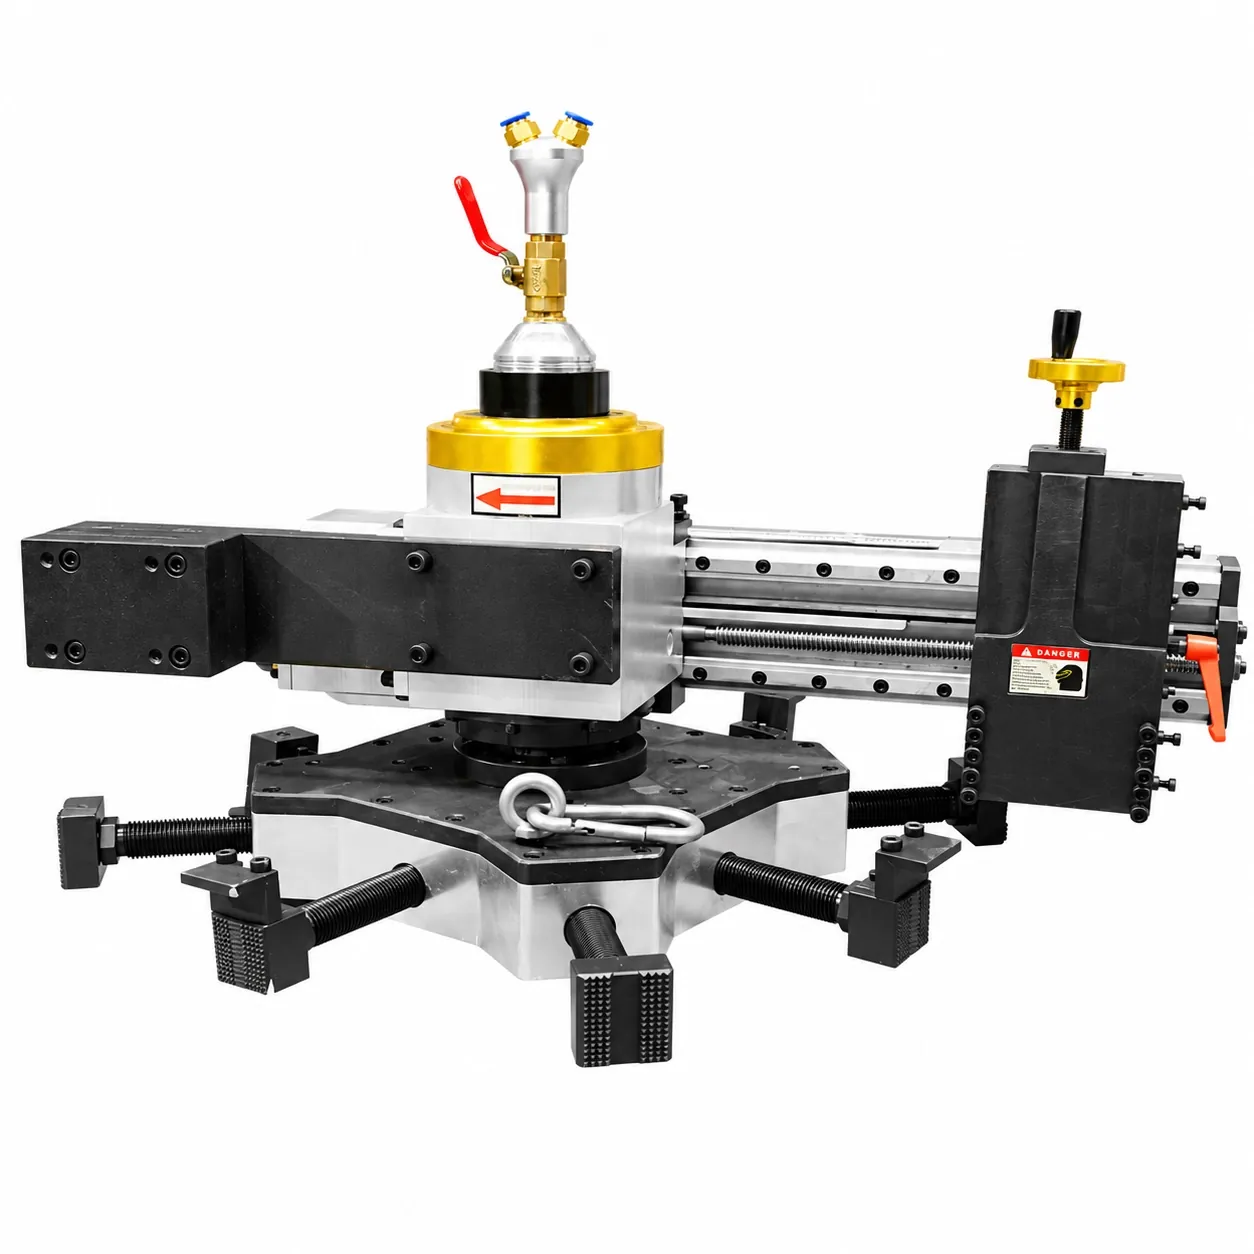
ID-mounted portable flange facer that resurfaces damaged sealing faces in situ — without removing the flange from the pipe. Cuts RF spiral serration, FF flat finish and RTJ grooves per ASME B16.5. Pneumatic, hydraulic or CNC servo drive across 5 size frames Ø 50 – 3000 mm.
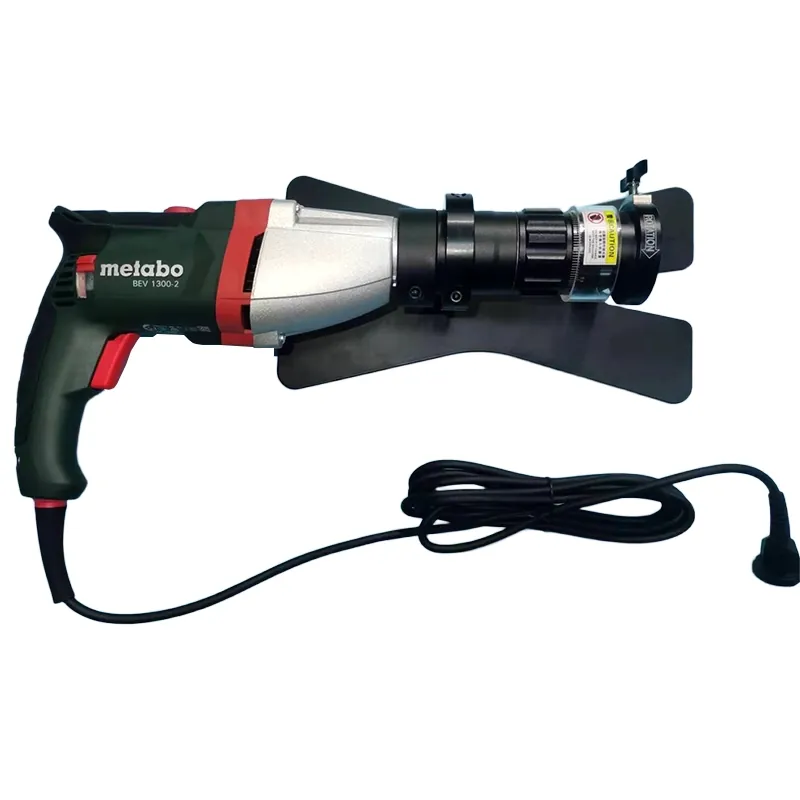
1300 W Metabo-driven benchtop tube facer for sustained production. Constant torque indefinitely, planetary gear reduction on larger models for low-RPM finish on thick-wall sanitary tube. Faces tube Ø 3.17 – 114.3 mm with wall up to 5 mm — the production-shop standard for high-purity tube fabrication.
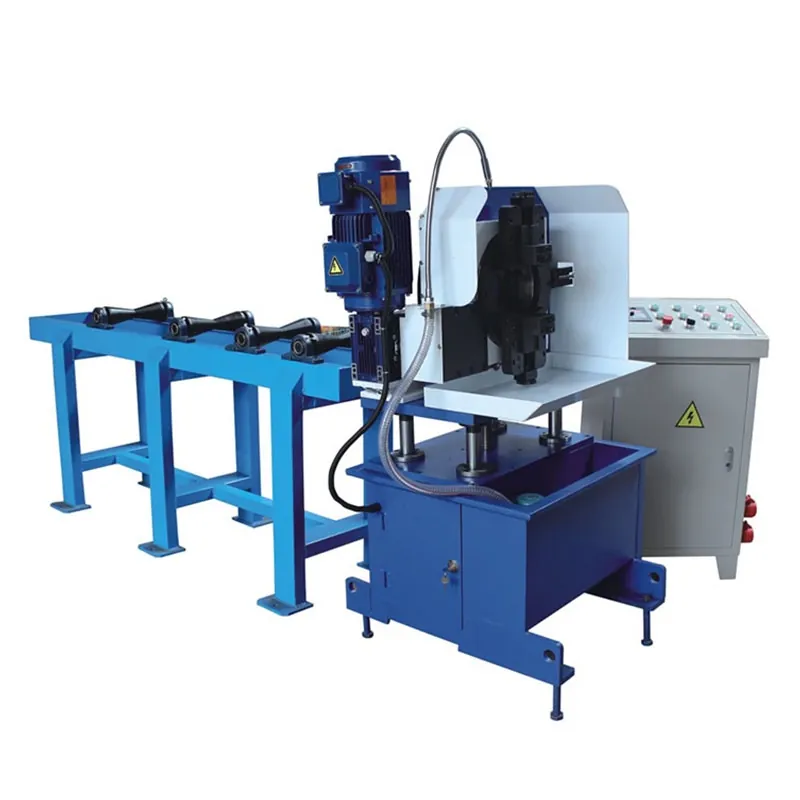
Floor-standing pipe spool cutting and beveling station. Holds the pipe stationary in a 4- or 6-jaw electric self-centering clamp while the tool head orbits around it — cutting and beveling in a single pass for pipe Ø 50 – 630 mm, wall up to 38 mm. The workhorse for prefab shop production.
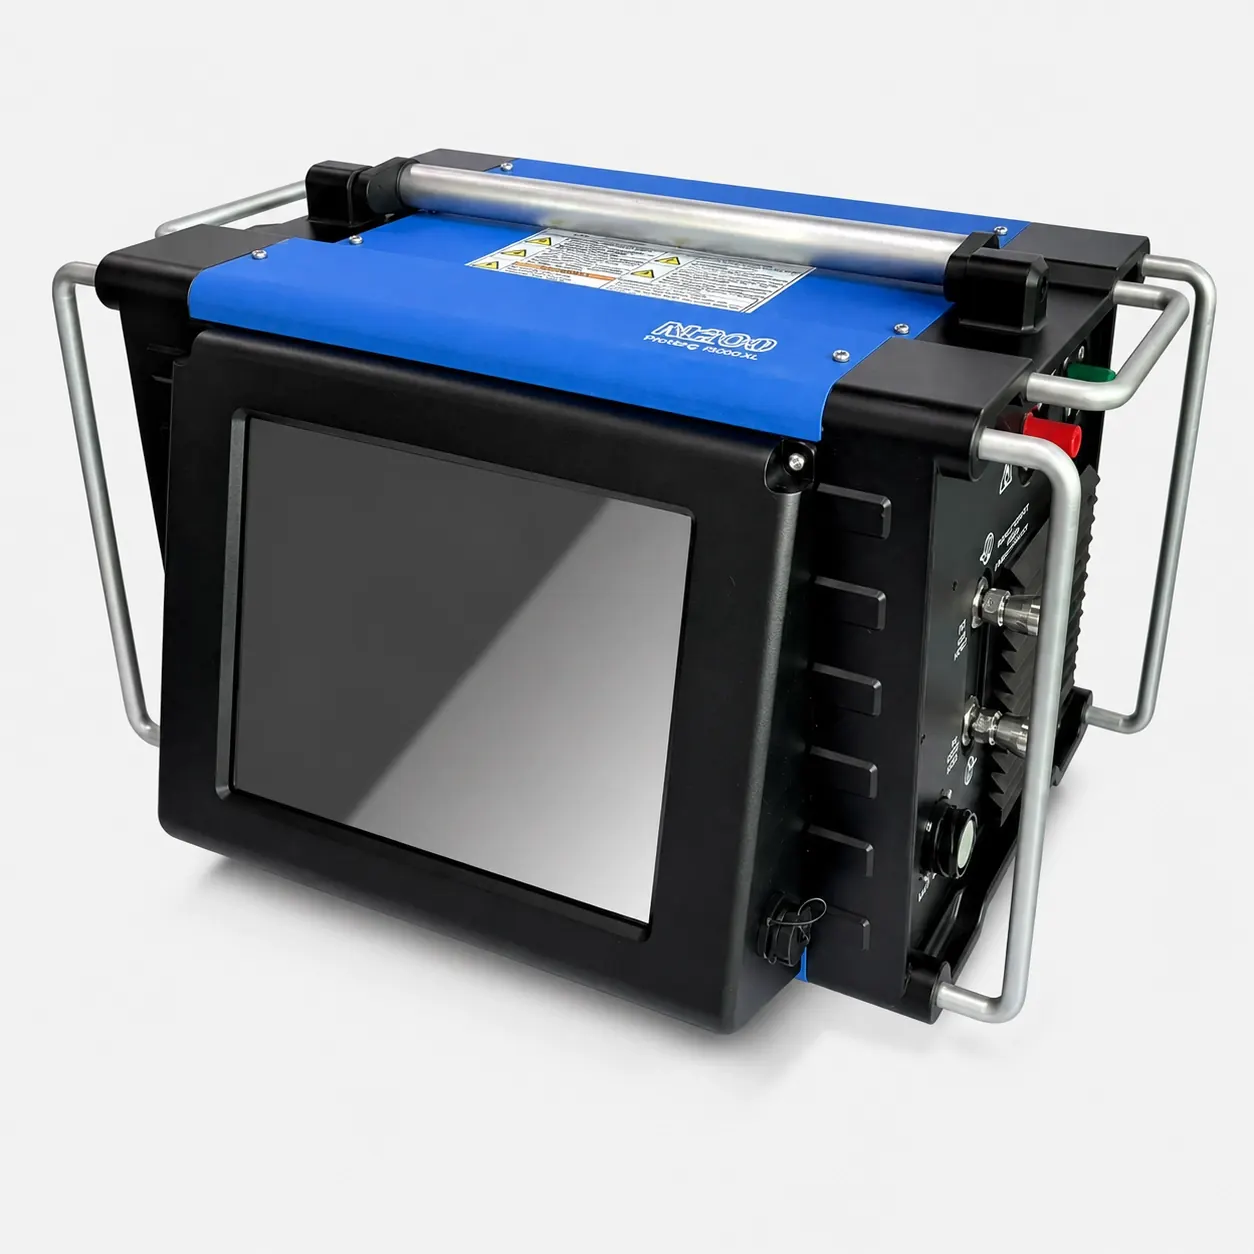
200 A enclosed orbital TIG welding power source — drives all five Astra Arc weld-head families (ND, MC, H, 8H benchtop and micro) across OD 6.35 – 152 mm. Mechanically and electrically compatible with U.S.-brand M200-family welders, so existing collets, fixturing and validated weld procedures transfer directly. Air-cooled for portable / intermittent work; water-cooled for 100% duty continuous production.
If your question is not covered, email contact@kedesmachine.com or open WhatsApp — engineers reply during Shenzhen working hours.
Every machine on this page is manufactured in our Shenzhen workshop — fixtures, gearboxes, electrical cabinets and final assembly all under one roof. No trading-company markup, and engineering questions are answered by the people building your unit.
Send pipe OD / wall thickness, material (carbon, stainless, duplex, Inconel), bevel geometry and whether the job is in-situ or shop-based. Our engineers reply within one working shift with the matching family and one or two sized models. If you are unsure, start from the Solutions pages — they group machines by industry.
Cold-cutting tools remove material mechanically with tungsten-carbide inserts, leaving no heat-affected zone, no sparks and no thermal distortion. That keeps the parent metallurgy intact (essential for sour service, stainless, duplex and Inconel) and meets HSE rules for hot-work-restricted zones offshore and in operating refineries.
Yes. We adapt voltage (110 / 220 / 380 / 440 V, 50 / 60 Hz), HMI language, branding and tooling heads to spec. Lead time on custom configurations is typically 4–6 weeks; standard catalogue units ship in 2–3 weeks.
Bevel geometry follows ASME B16.25, EN ISO 9692-1 and API 1104. Pressure-test rigs and electrical cabinets are CE-compliant. Certificate copies (material, dimensional inspection, electrical) ship with each unit.
Wear parts (carbide inserts, drive belts, seals, brushes) are stocked for the life of the unit and ship within 72 hours from Shenzhen. English technical support runs Mon–Sat, 08:00–22:00 GMT+8 via WhatsApp, email and video call.
Send pipe diameter, wall thickness, material and bevel angle — or your full drawing. Our engineers reply within one working shift with sized models, FOB / CIF pricing and lead time.