
Pick the right tool.
Process explainers, standard references and selection guides written by our field machining engineers. New articles published as the workshop runs into questions worth answering.
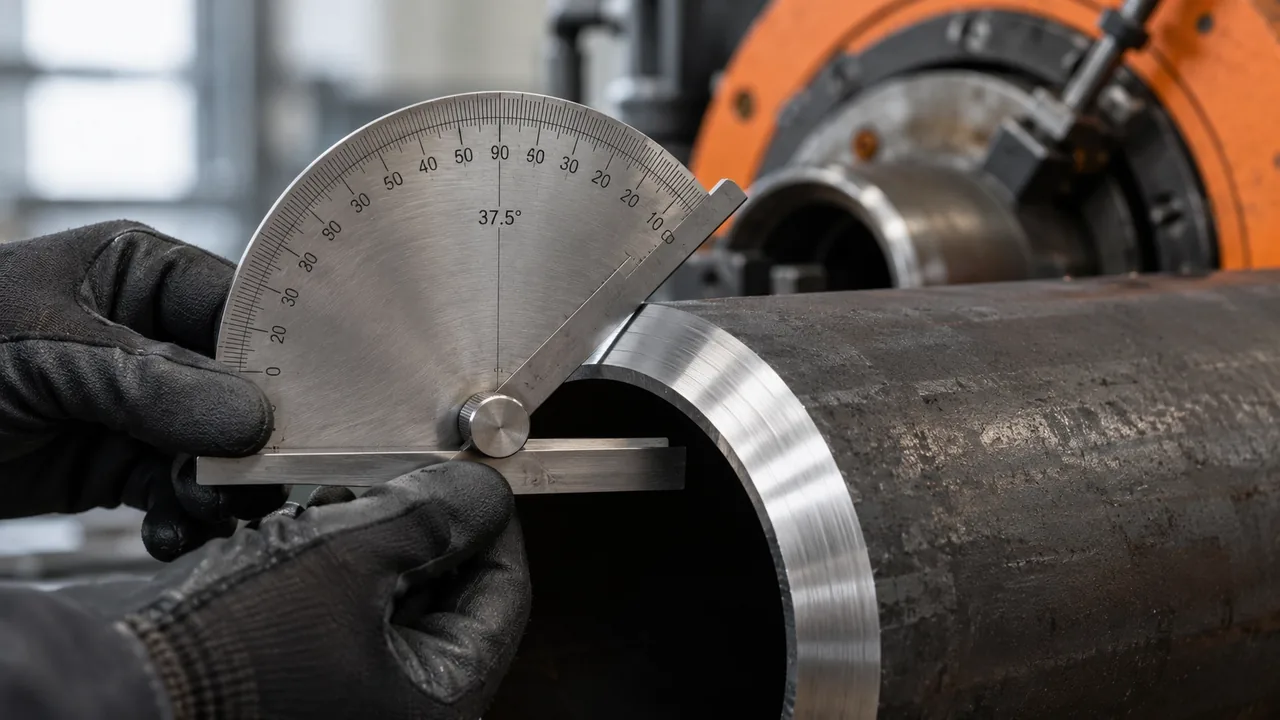
How to Measure a Pipe Bevel: Gauges, Formulas & Tolerances
A bevel that measures wrong fails twice — once at fit-up, once at inspection. Here's how to check bevel angle, root face, and width with the right gauge (or no gauge at all), plus a calculator that does the trig for you.
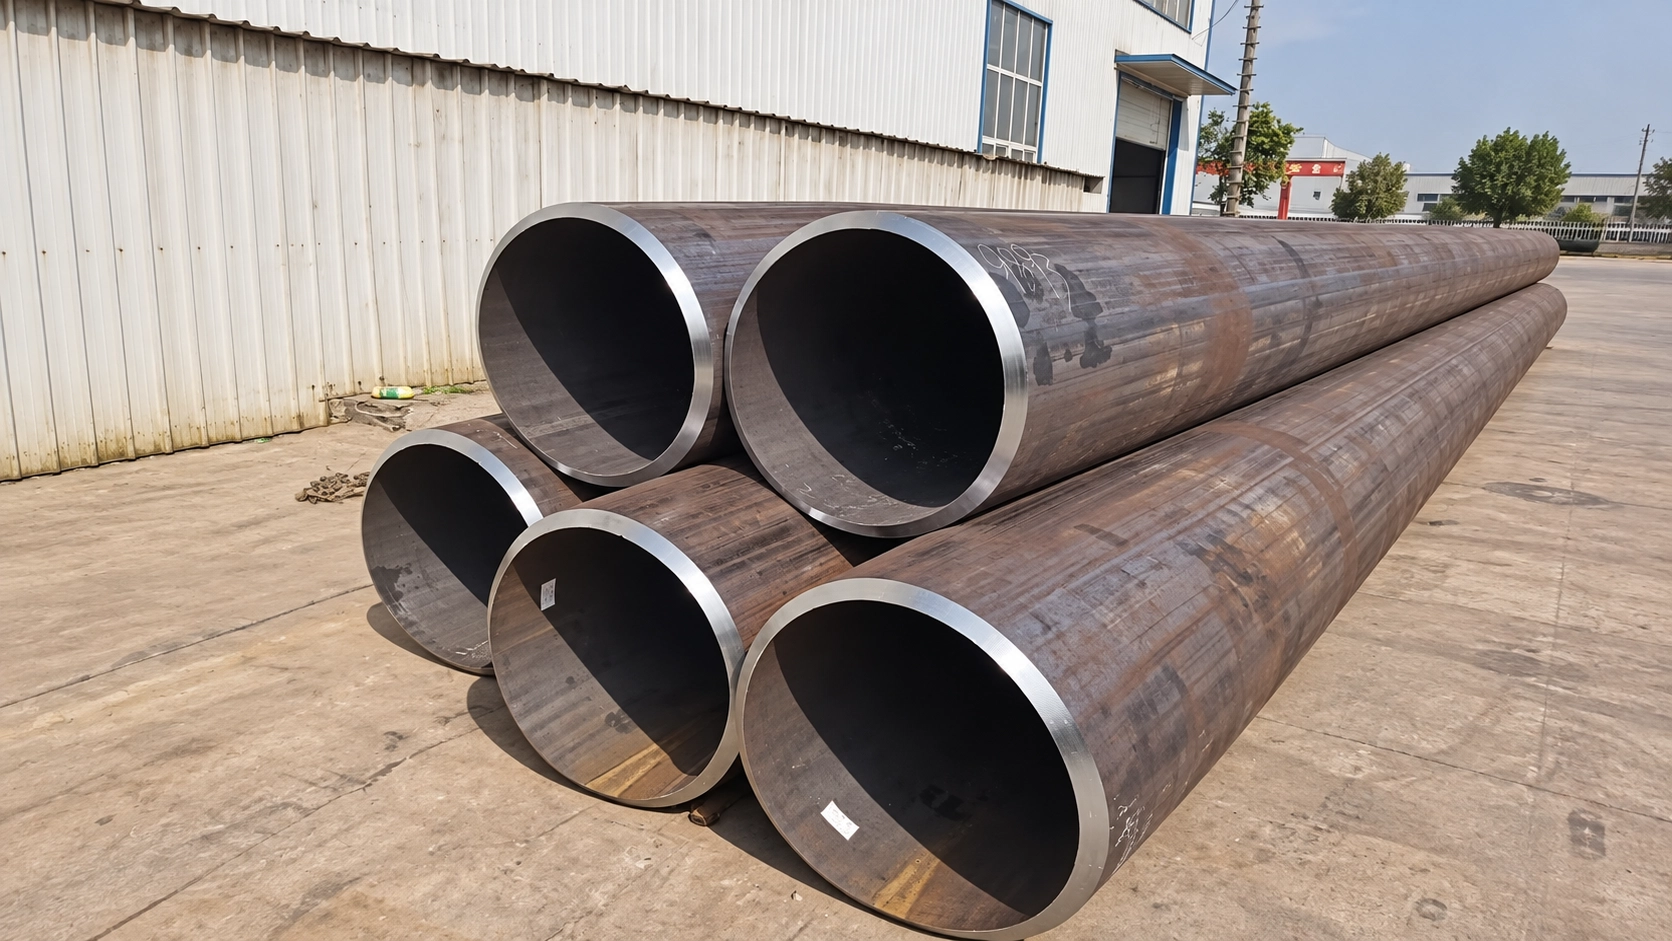
Compound Bevel on Pipe: Angles, Dimensions & When to Use It
A compound bevel isn't a fancy V — it's two angles doing two different jobs: 37.5° to keep the root open, 10° to stop the groove ballooning. Skip either and you've missed the point.
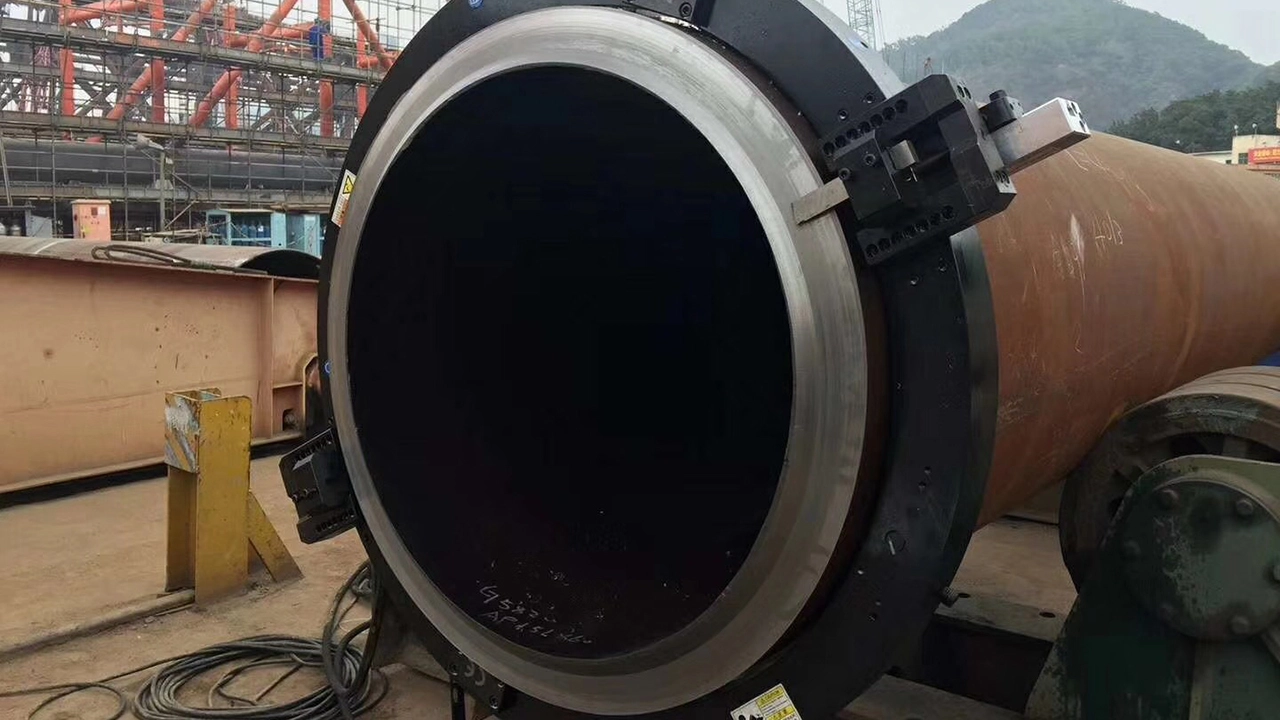
J-Bevel on Pipe: Dimensions, Angles & When to Use It (2026)
Everyone asks me for the 'standard J-bevel angle.' There isn't one — there's a dimension set: groove angle, root radius, and root face. Get all three right or don't bother switching from V.
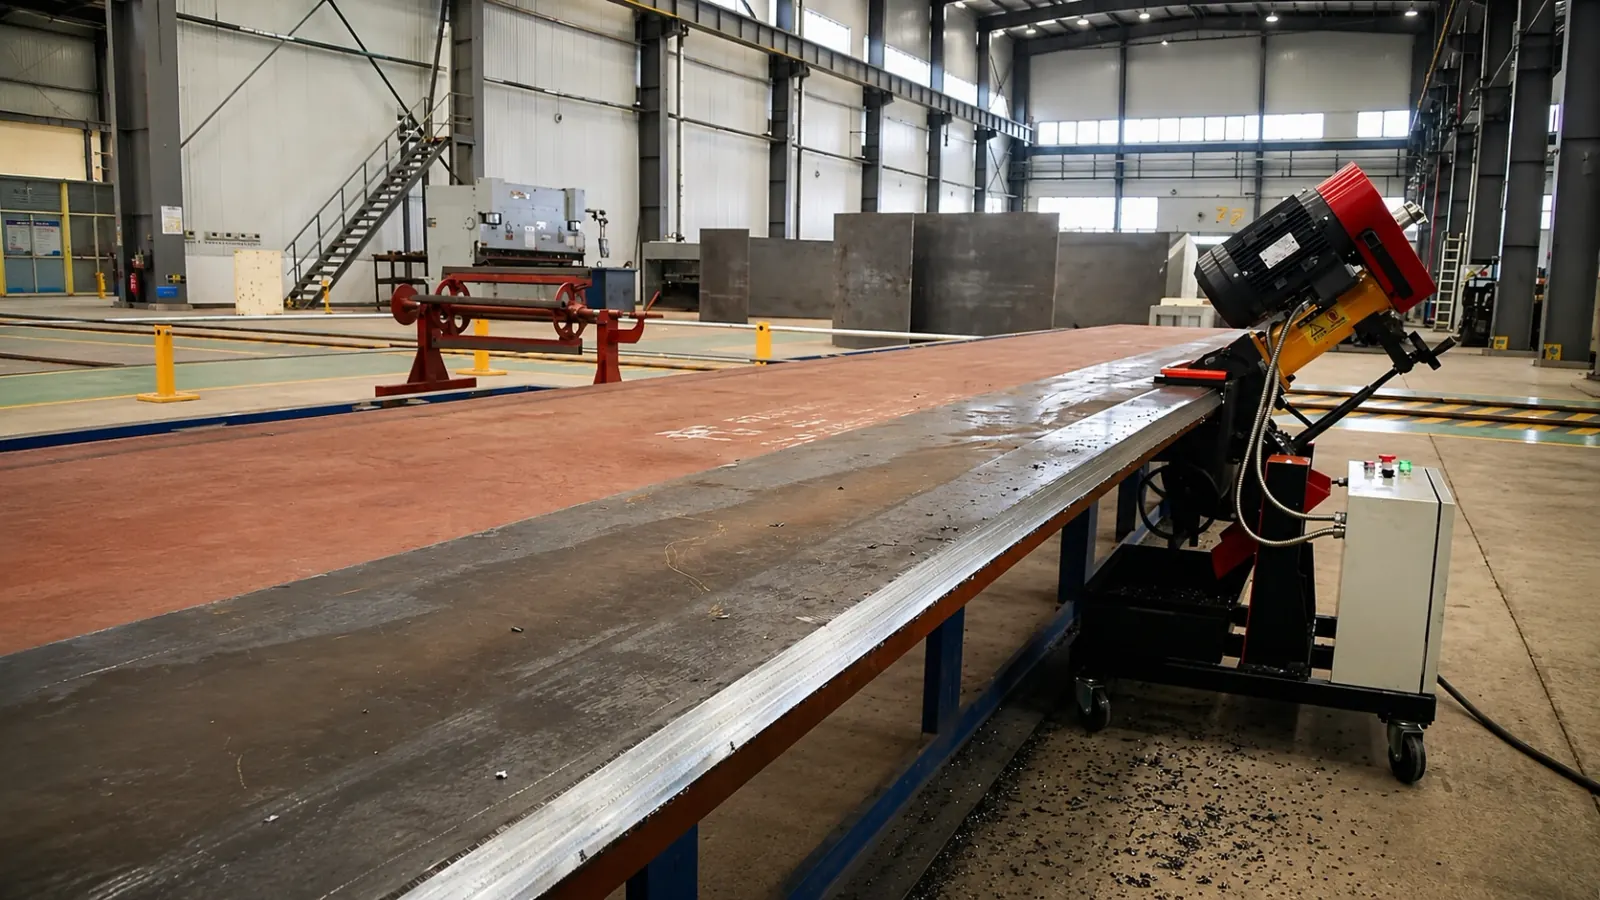
Double-Sided Plate Beveling — X and K Bevel Practice
Above ~20 mm wall, single-V plate prep is the most expensive habit in a fab shop. Here is when X and K bevels actually save money, the distortion story most shops do not measure, and the machine choice that decides whether the saving survives the project.
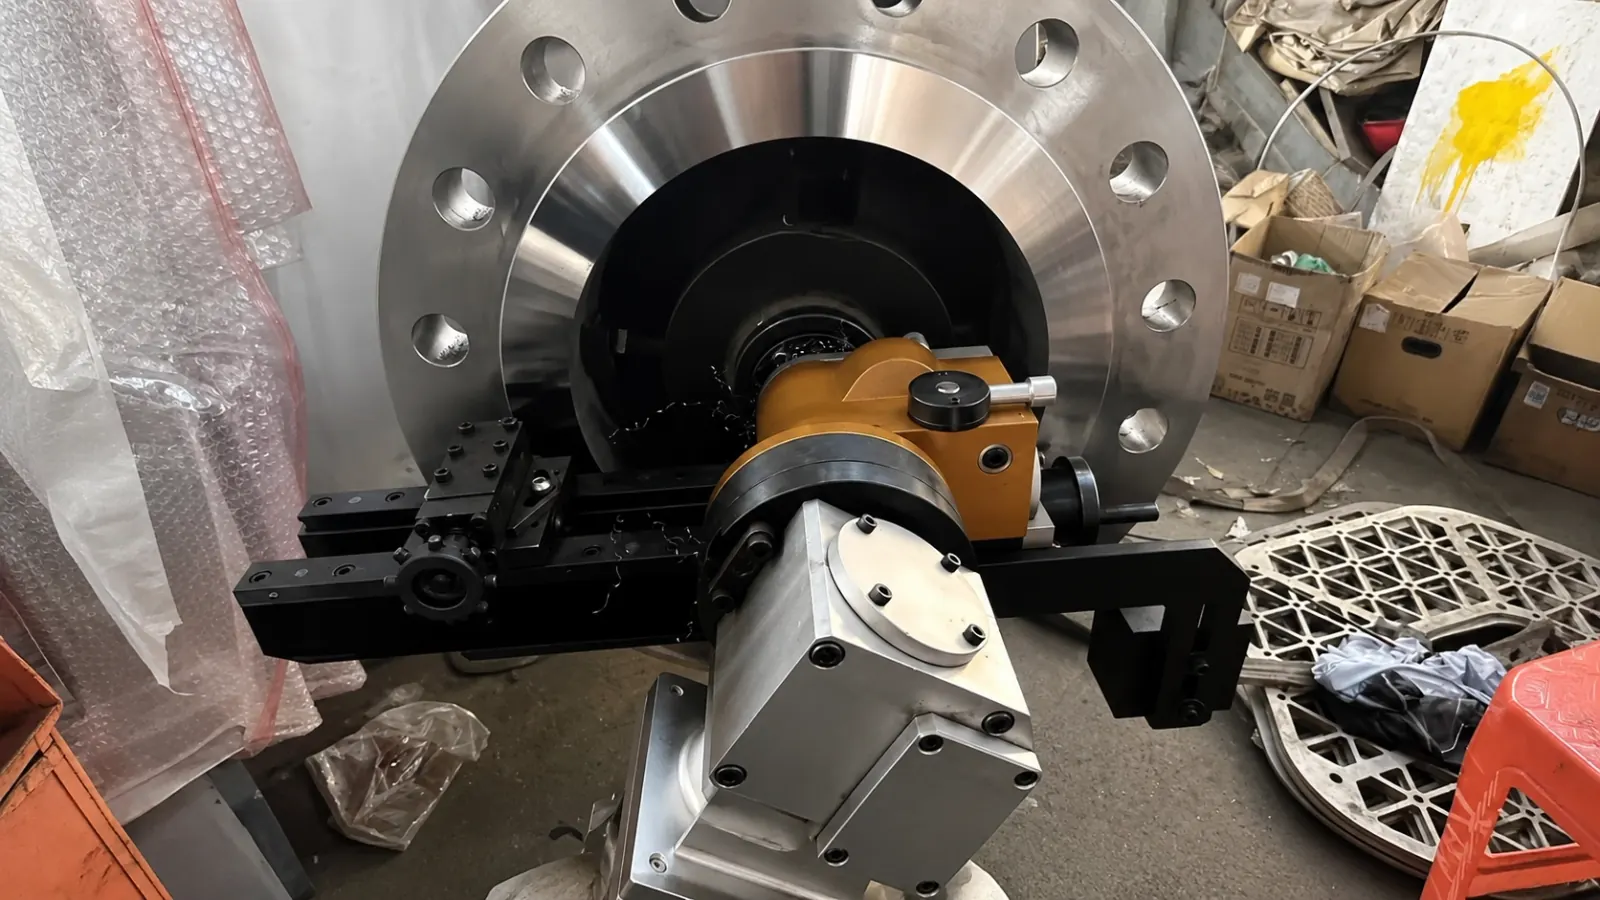
Flange Surface Finish — Stock, Smooth and Spiral Serrated Explained
Flange face finish is not a cosmetic spec. It is the sealing parameter, and matching it to the gasket is what stops the joint leaking. Here are the three finishes you will see on a drawing, the Ra targets that matter, and the failure modes I have seen from getting it wrong.
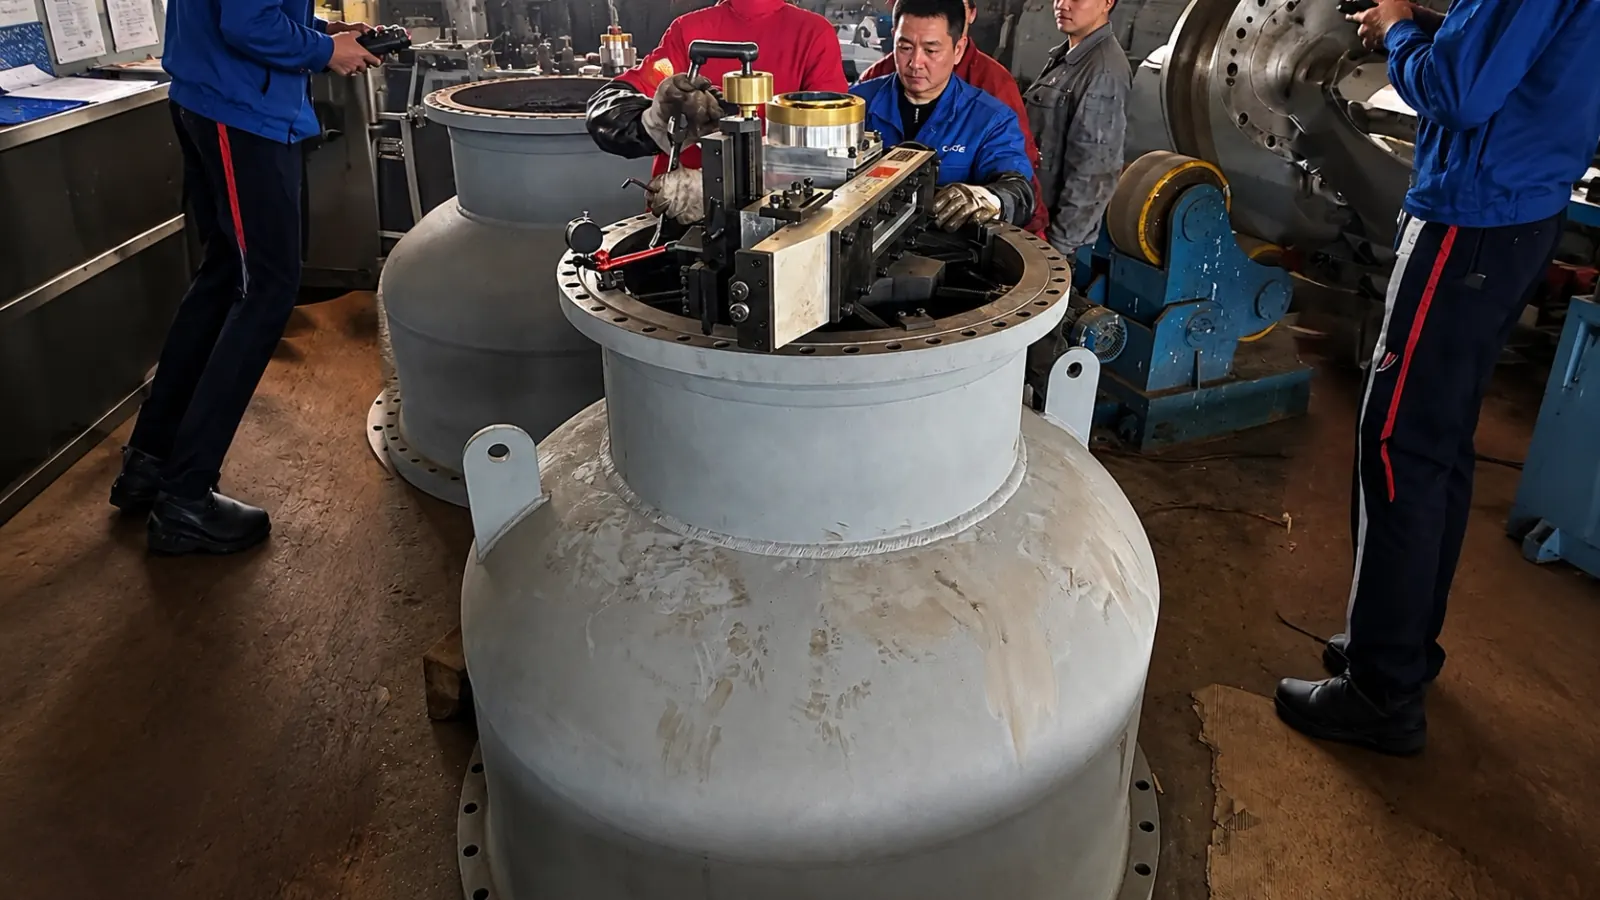
How to Machine RTJ Grooves On-Site (API 6A Field Repair)
RTJ grooves seal by metal-on-metal contact, which is exactly why a small error on depth, angle or surface finish leaks. After two decades of flange-facing call-outs, here is what holds tolerance in the field and the four mistakes I keep watching crews make on R-, RX- and BX-grooves.
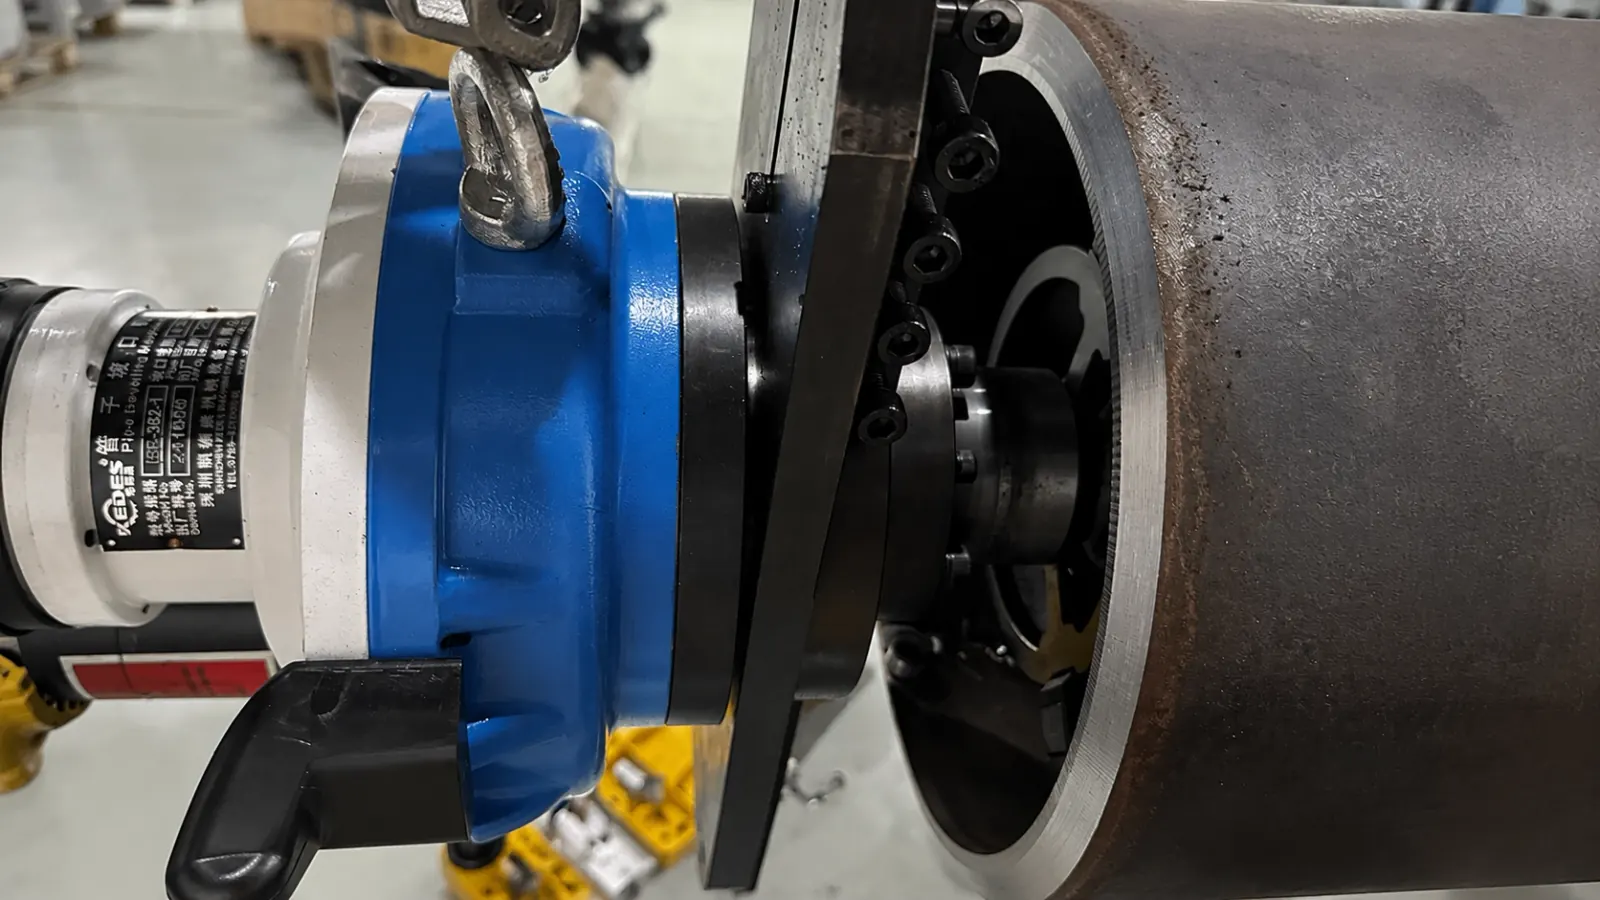
Pneumatic Machining in Hazardous Zones — What It Buys You
Pneumatic drive does not magically make a tool safe in a Zone 1 area. It removes one ignition source — the electric motor — and that single removal is the difference between starting the job at 06:00 and waiting on a hot-work permit. Here is what it actually buys you and what it does not.
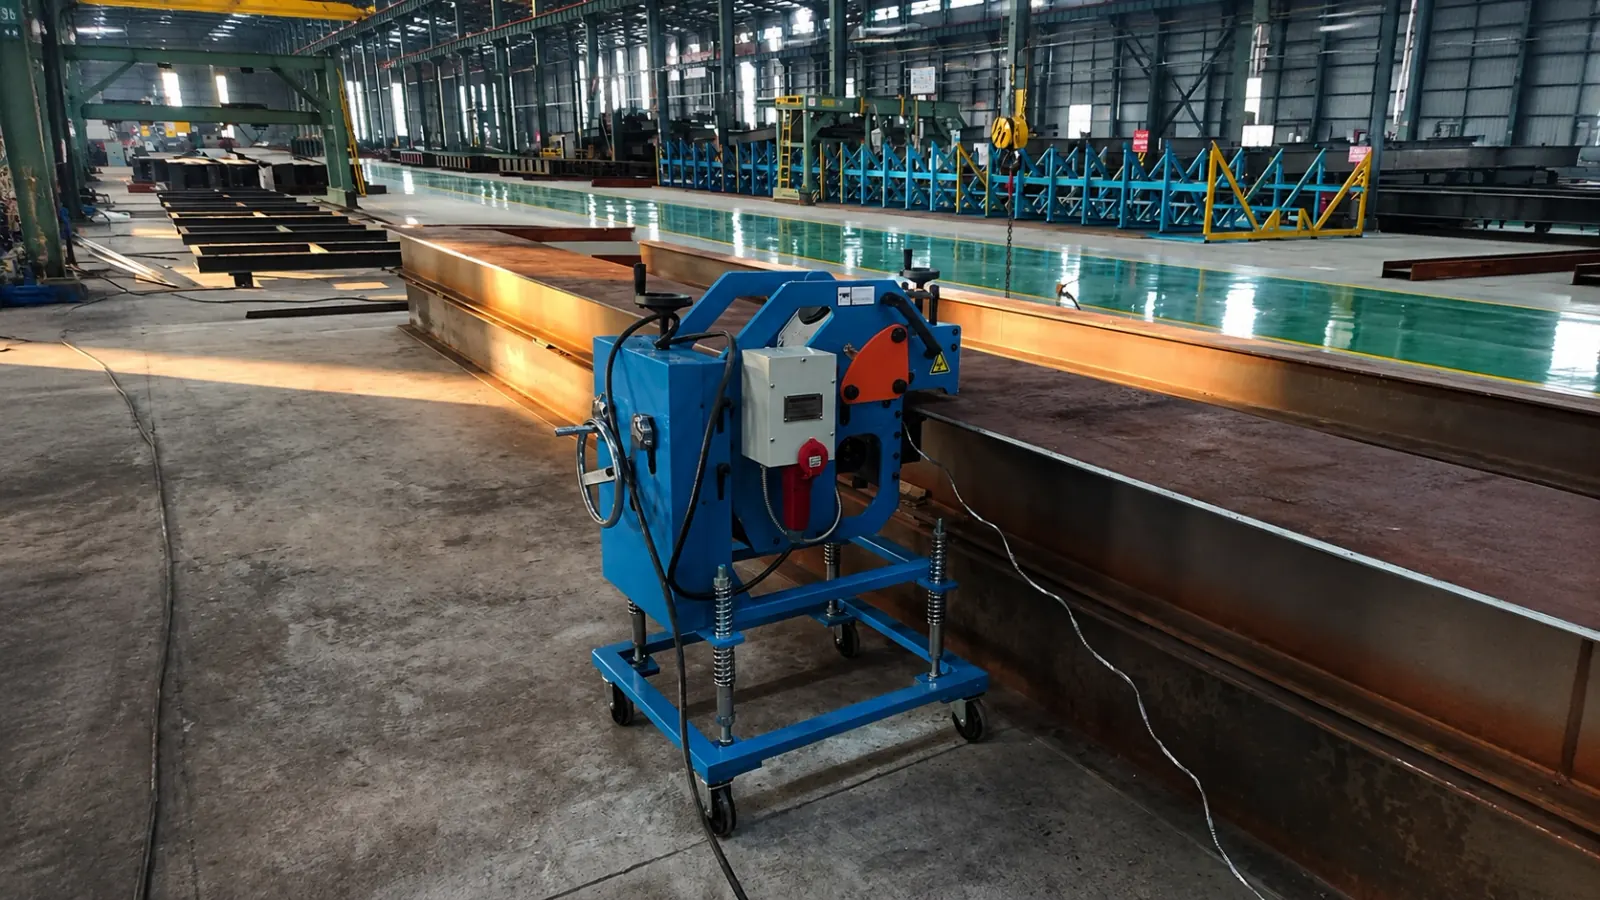
Rolling Shear vs Edge Milling — How to Pick for Plate Prep
Rolling shear is the right answer for long production runs at one angle. Edge milling is the right answer for almost everything else. Here is the break-even, where rolling shear quietly fails on alloy, and the question most shops ask backwards.
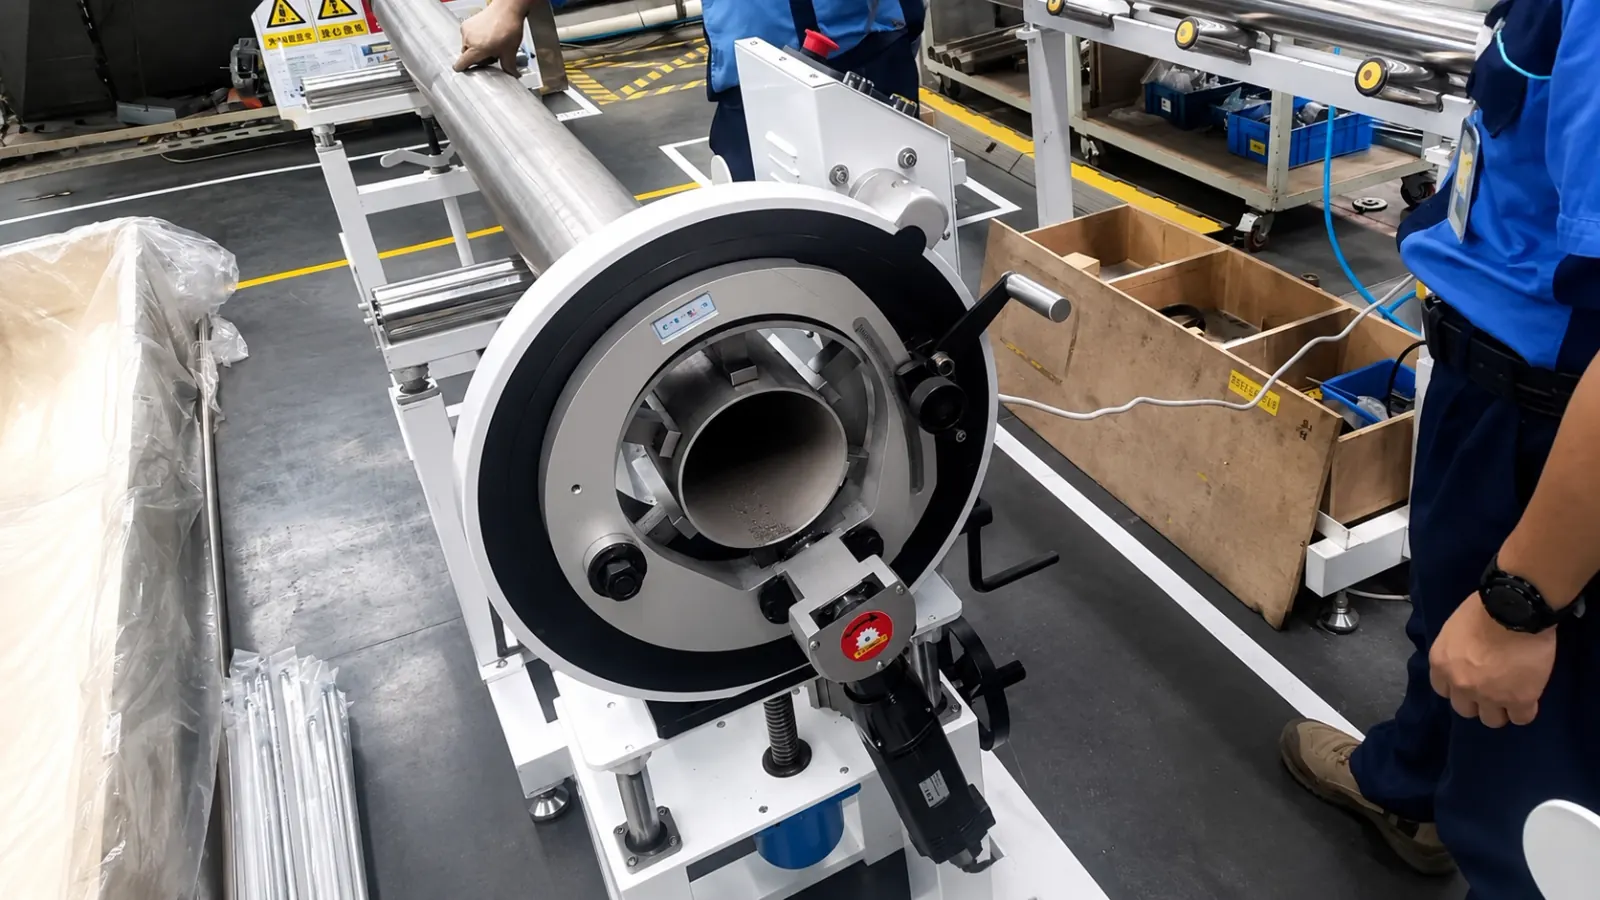
Choosing an Orbital Pipe Cutter — A Field Buyer's Guide
There is no single "best" orbital pipe cutter — there is a right machine for the tube range, the squareness target and the access window you actually have. Here is the decision tree I walk every orbital-welding client through, with the trade-offs the brochures gloss over.
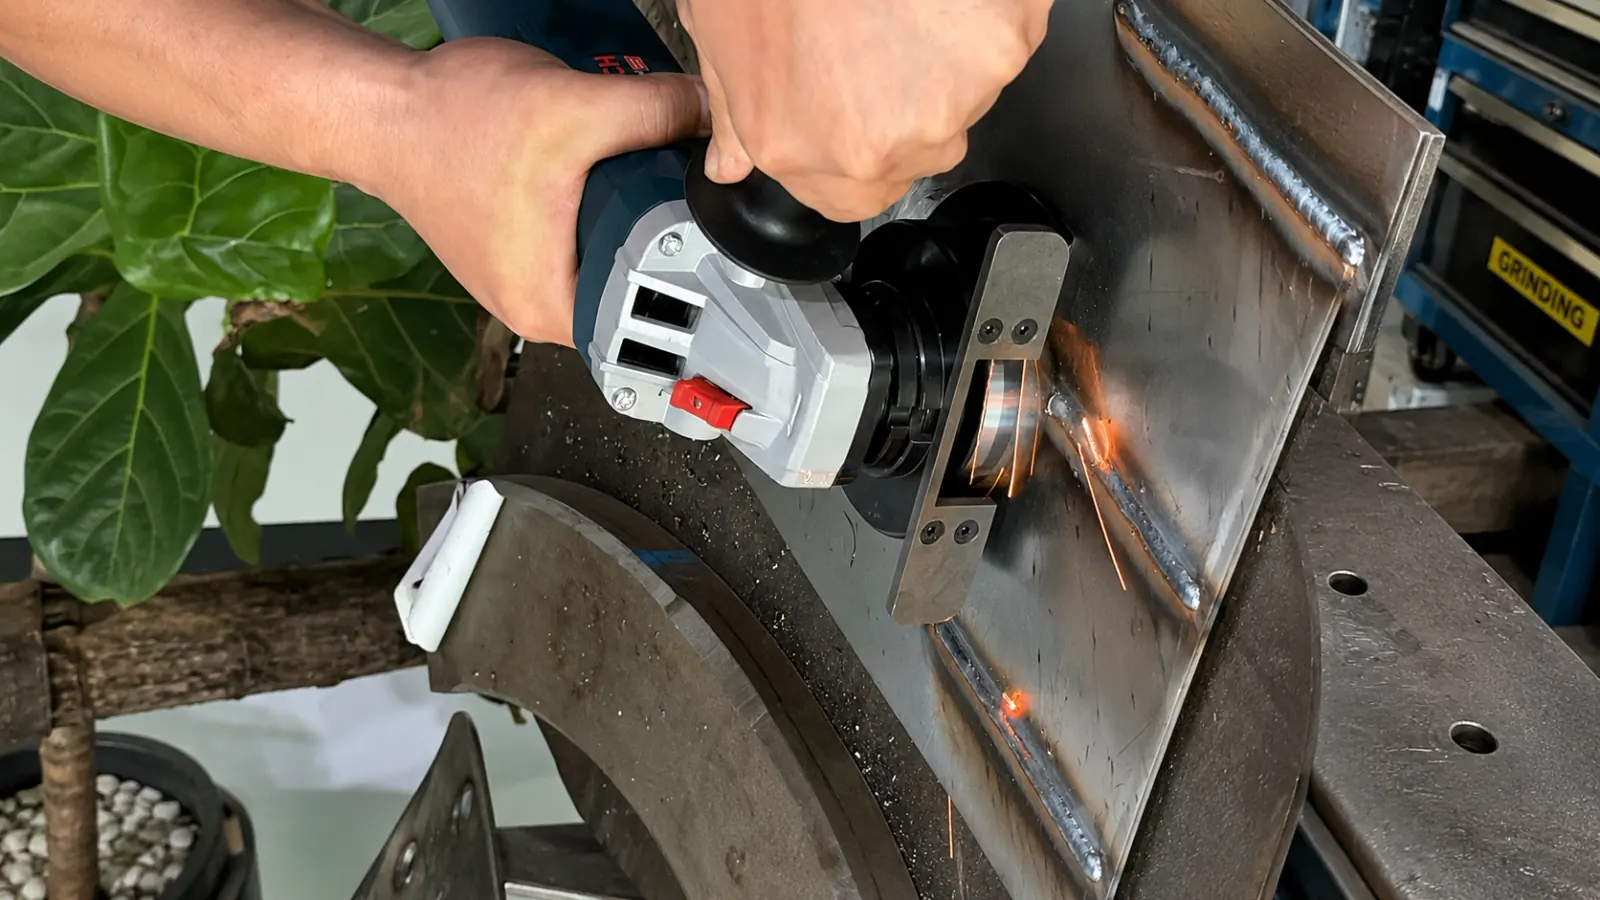
Choosing a Weld Seam Removal Tool — Planer, Miller or Grinder
A grinder will eventually flatten any weld seam. So will a hammer. Neither produces what the spec asks for on long seams or controlled finishes. Here is when a powered planer or miller is the right machine, the height tolerance each method can hold, and the math on switching from a grinder for production work.
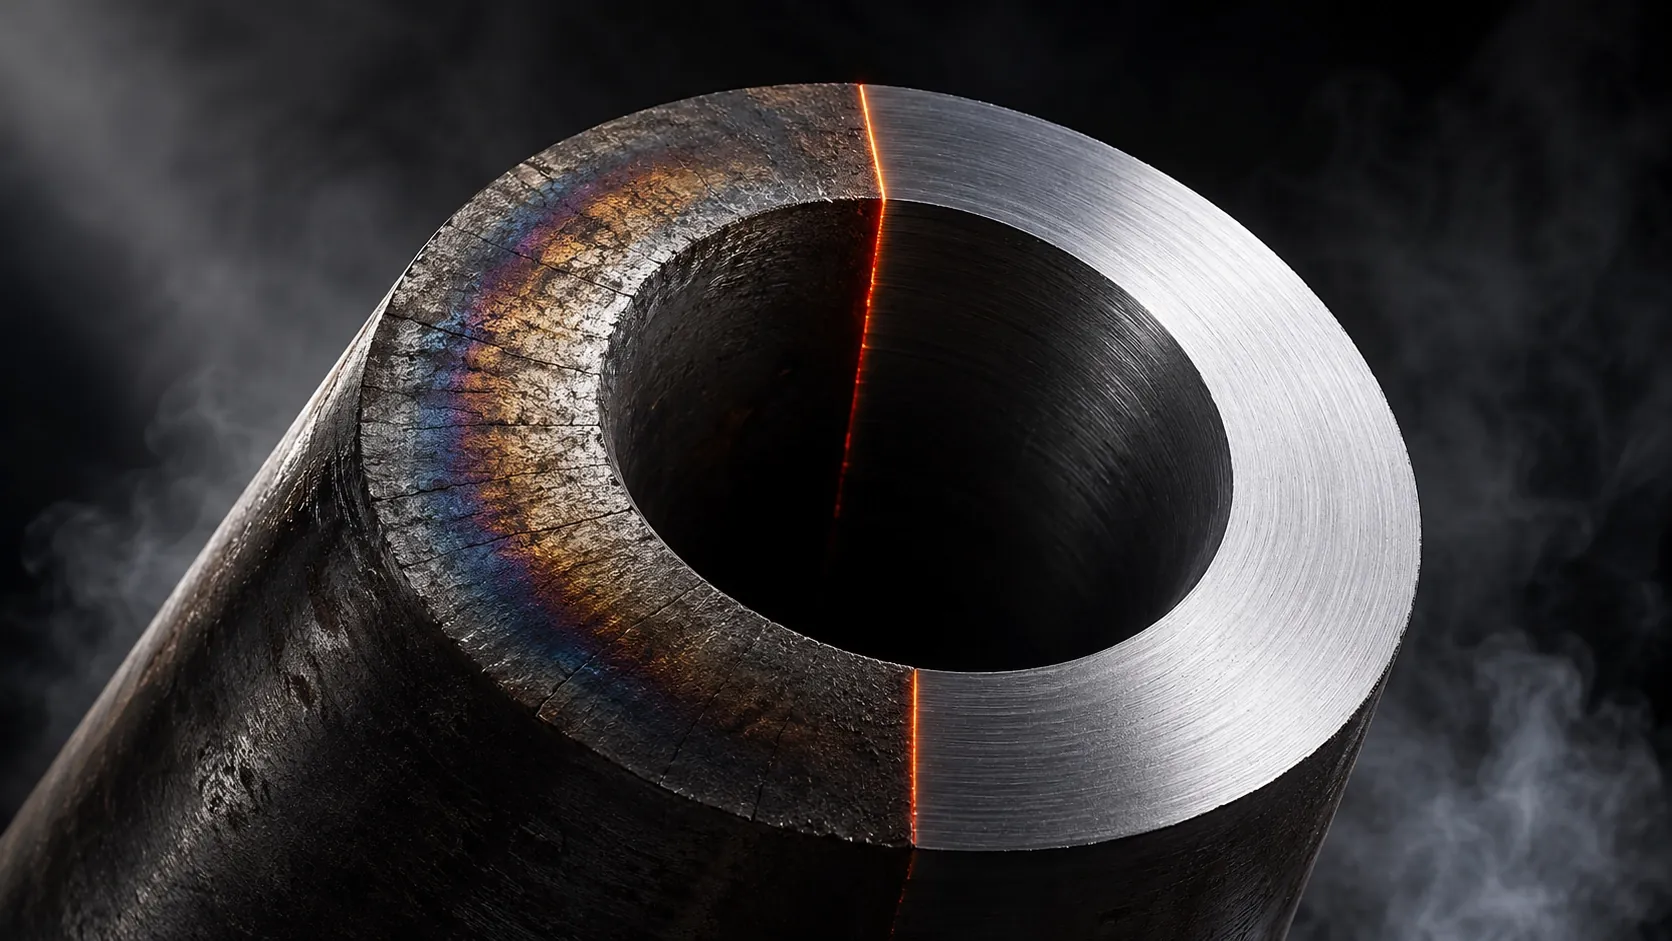
P91 Pipe Beveling: Why Heat Cutting Creates Micro-Cracks
P91 doesn't crack during the cut. It cracks two days later, after PWHT, when the boiler is being pressurized for the first time. Here's why thermal cutting is the single most expensive mistake you can make on chrome-moly pipe.
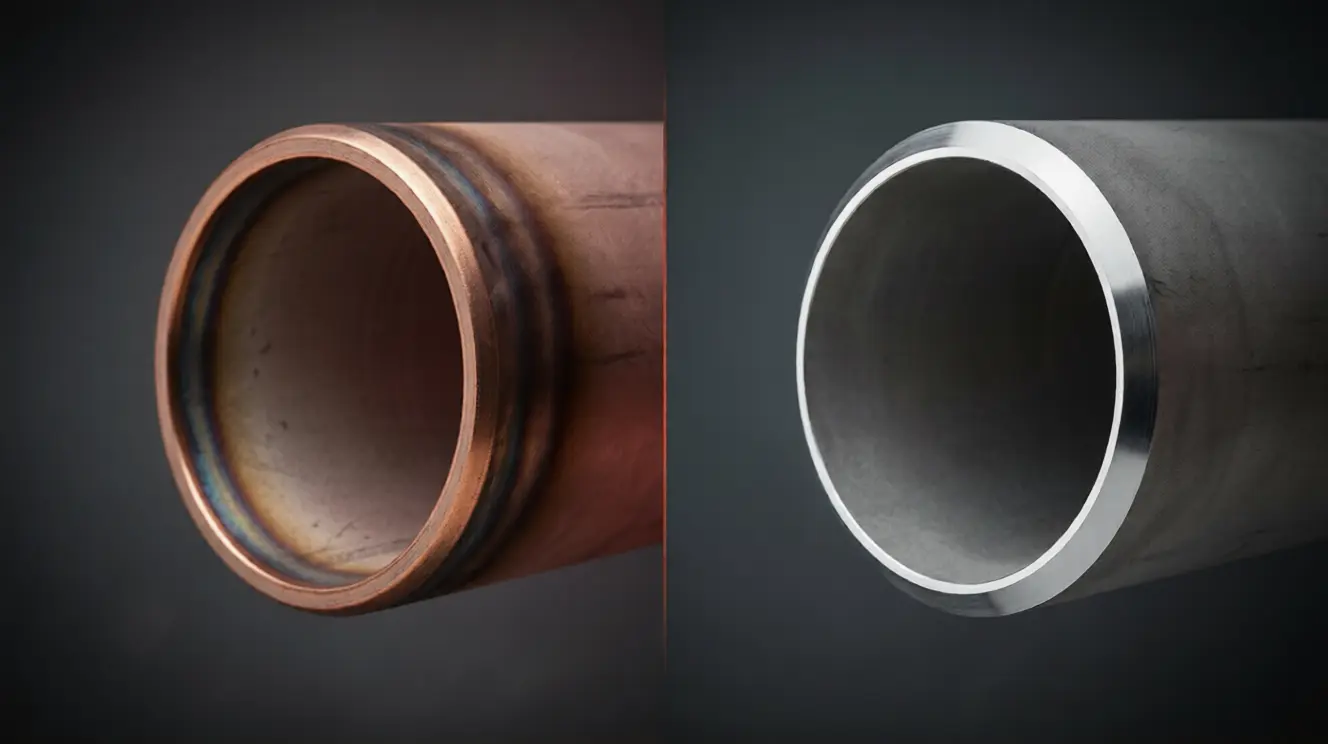
Stainless Steel Pipe Beveling: Why Heat Is Your Worst Enemy
Oxy-fuel can't even cut 316L properly. Plasma leaves a sensitized band that corrodes in 18 months. Angle grinders drag iron into the surface and seed rust. Here's why every 'fast' stainless prep method is wrong — and what actually works.
Orbital Welding Basics for High-Purity Tubing
Orbital welding makes consistent X-ray-quality joints on tubing that is too small or too critical to hand-weld reliably. The process is not the hard part — the tube prep is. Here is how the closed head works, what the prep tolerances really are, and where I see clients waste a head on bad upstream machining.
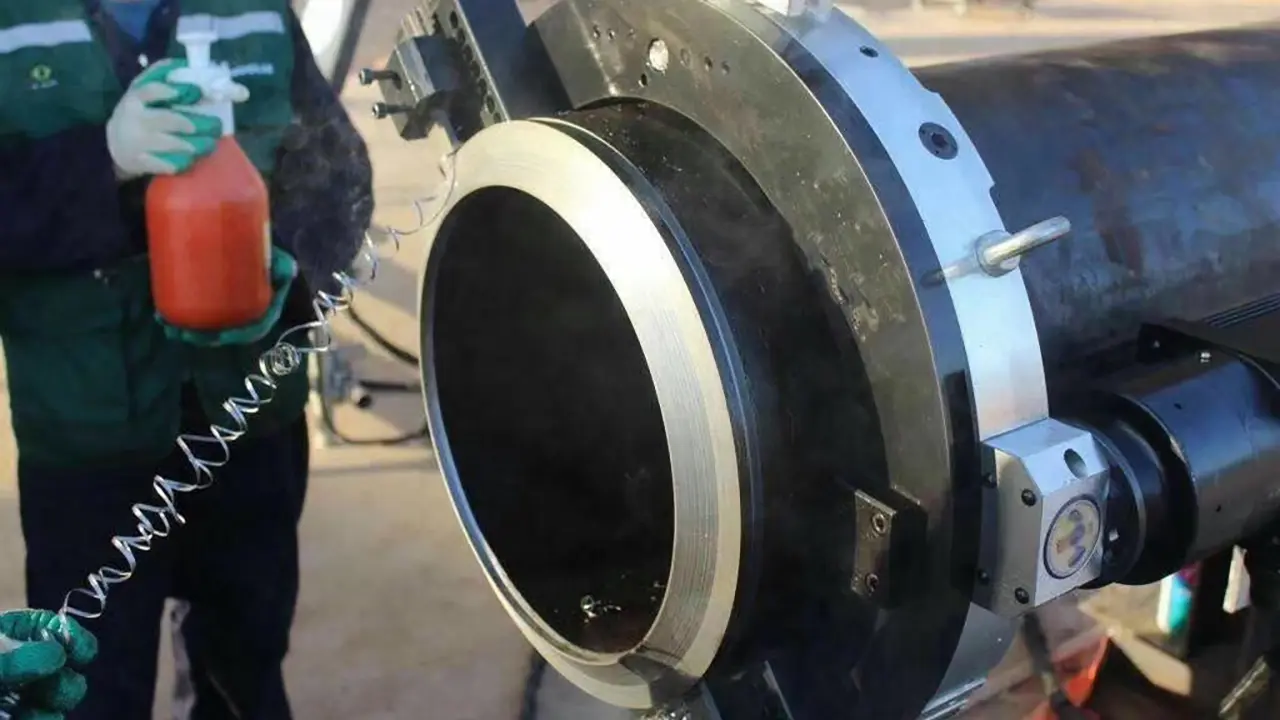
Pipe Cold Cutting Machines: Types, Selection & Applications
Not all pipe cold cutting machines are the same. Clamshell, split frame, planetary — each handles different pipe sizes, wall thicknesses, and job site conditions. Here's how to choose the right one.
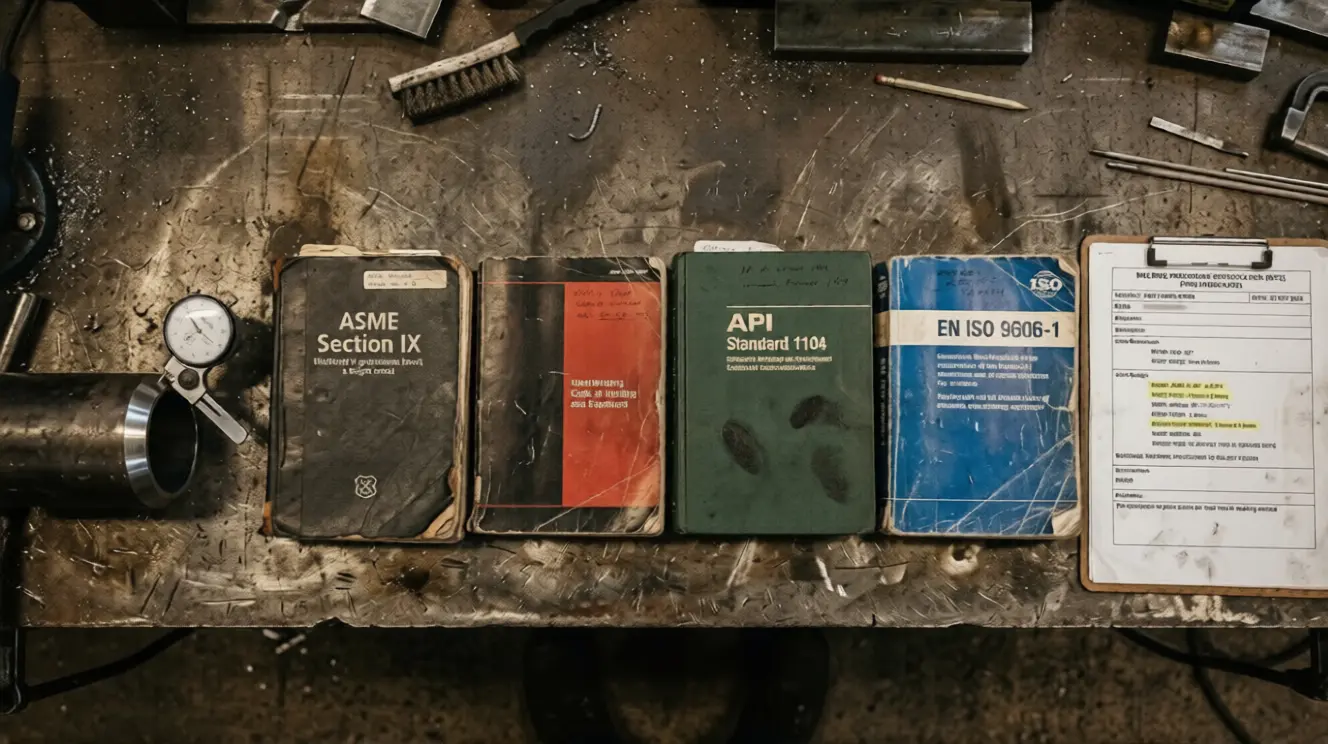
Every Welding Bevel Standard You'll Actually Encounter: ASME, AWS, API, EN — In One Place
I've watched a qualified welder bevel 40 joints to ASME B16.25 specs—on a project governed by API 1104. Nobody caught it until the CWI flagged the included angle on the first fit-up. 40 pipe ends, re-beveled. Two days lost. The welder wasn't incompetent. He'd just come off a refinery turnaround and muscle memory took over. That's what happens when your crew works across multiple codes and nobody has a quick reference that shows the differences at a glance.
API 1104 Bevel Requirements: Angle, Root Face & Gap (2026)
API 1104 looks like the simplest welding code to bevel for—one angle, one root face, one root gap. Then you get a reject call from the RT crew at 2 AM and realize the 'simple' bevel wasn't as consistent as you assumed. The difference between a pipeline that passes 100% radiography and one that hemorrhages repair welds almost always starts at the bevel.
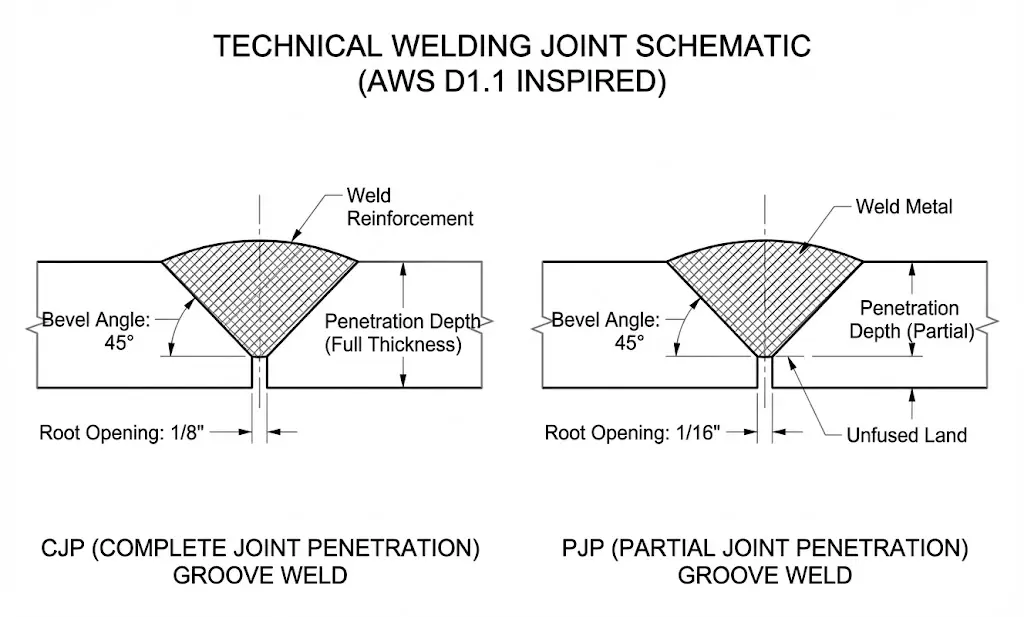
AWS D1.1 Structural Steel Beveling: What the Code Requires vs. What Most Shops Actually Do
Most structural steel shops think AWS D1.1 beveling is simple—until a CWI rejects an entire batch of column splices. The code's tolerances are tighter than people assume, and the gap between 'code-required' and 'shop-floor reality' is where rework hides.
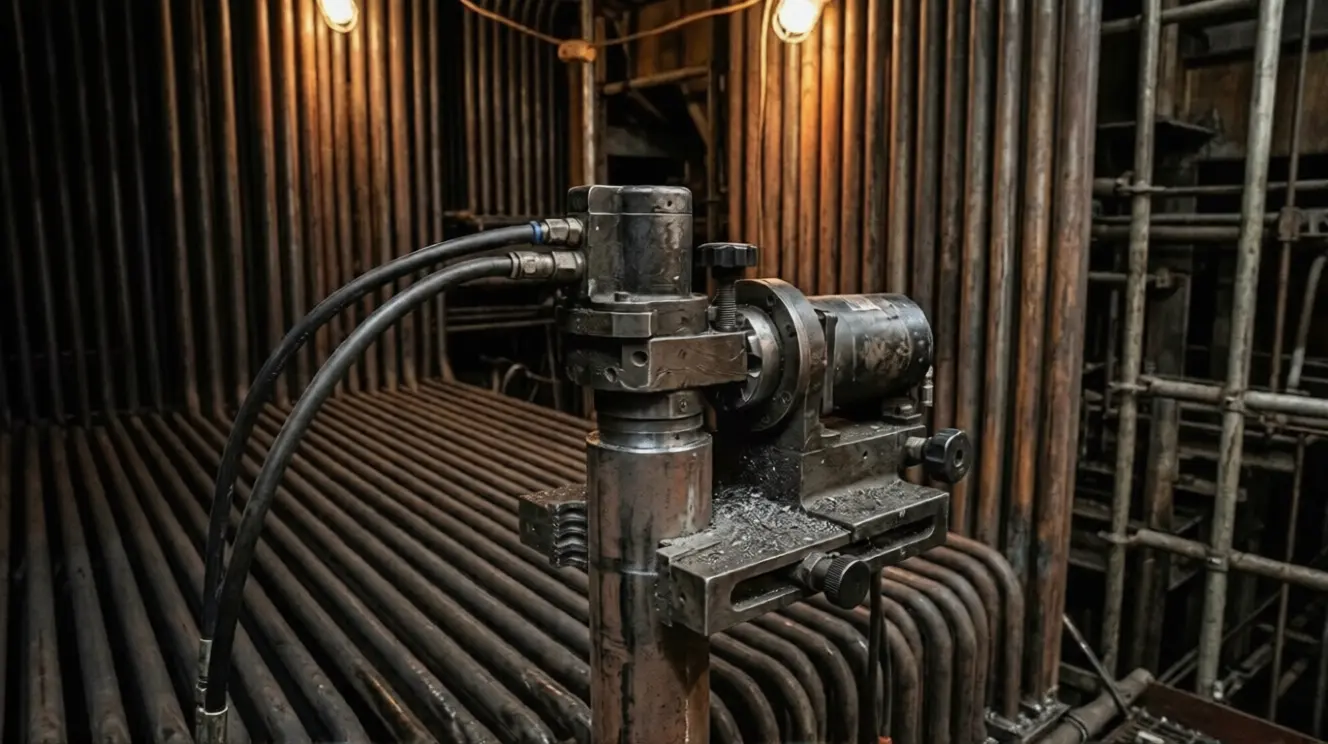
Boiler Tube Beveling: Why Power Plant Contractors Keep Burning Through Carbide (And How to Fix It)
Boiler tube beveling isn't hard in theory—it's hard in practice. Tight spacing, heat-affected material, and 200 tube ends per outage make it the kind of work where wrong tooling costs you the entire shutdown window.
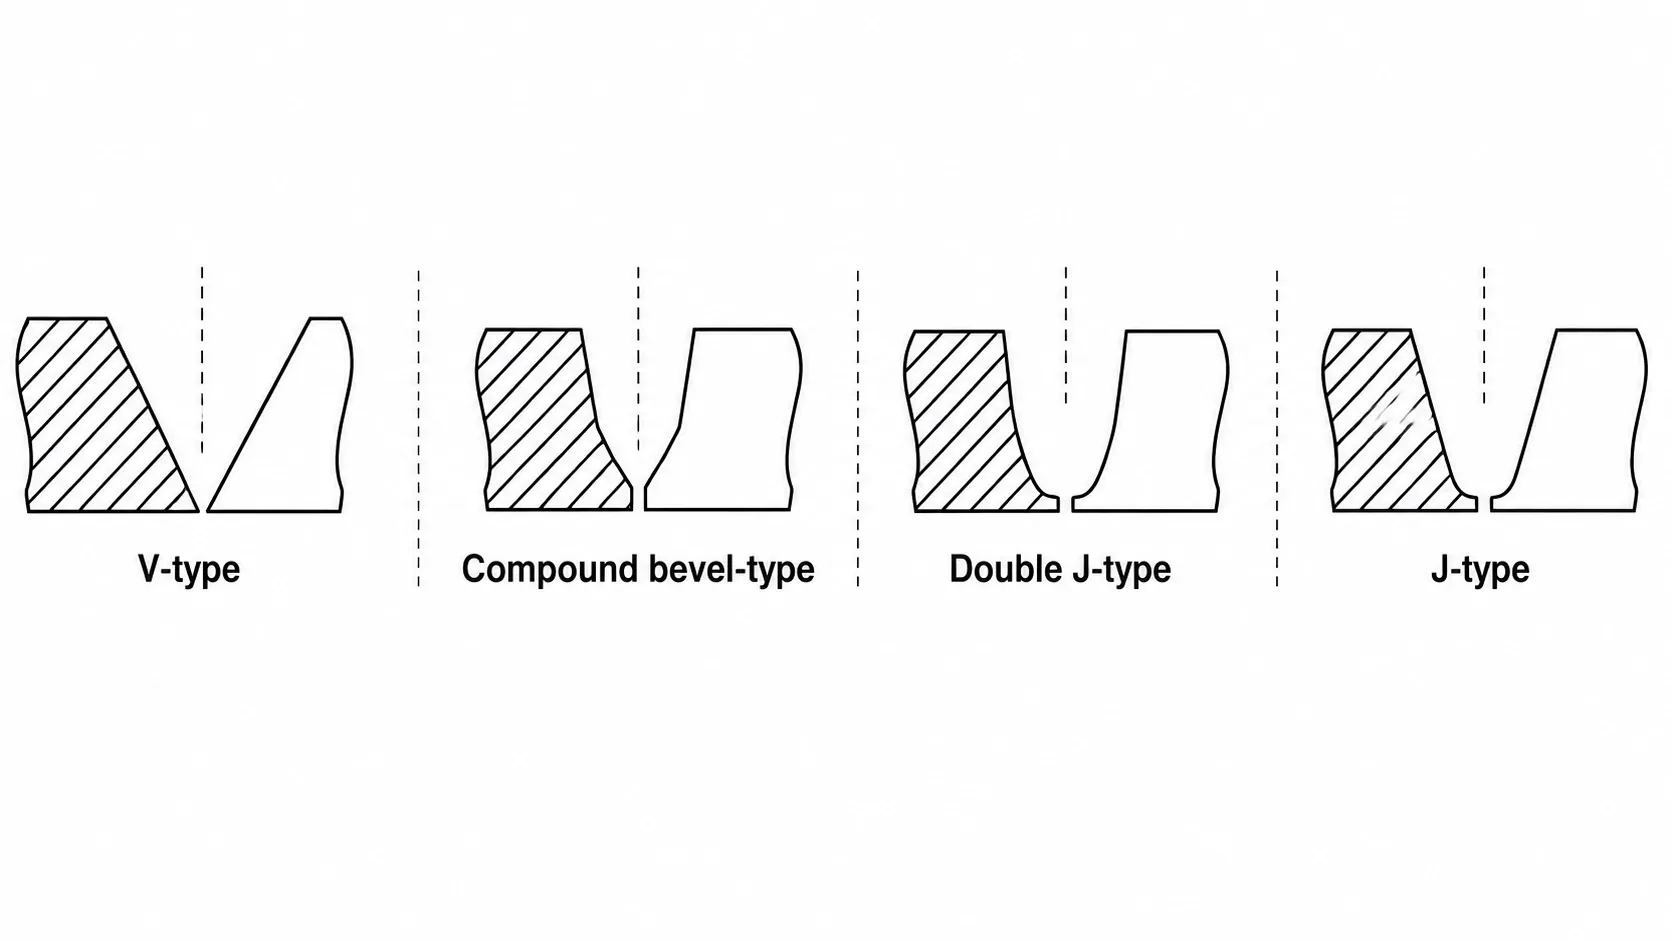
V Bevel vs J Bevel — Geometry, Economics and When the J Pays Back
V is the workhorse. J cuts weld volume by a third to a half on thick walls. Compound is the play when you can weld both sides. Here is how I pick between them on a real job, where the economic break-even actually sits by material, and the two ways J-prep quietly fails to pay back.
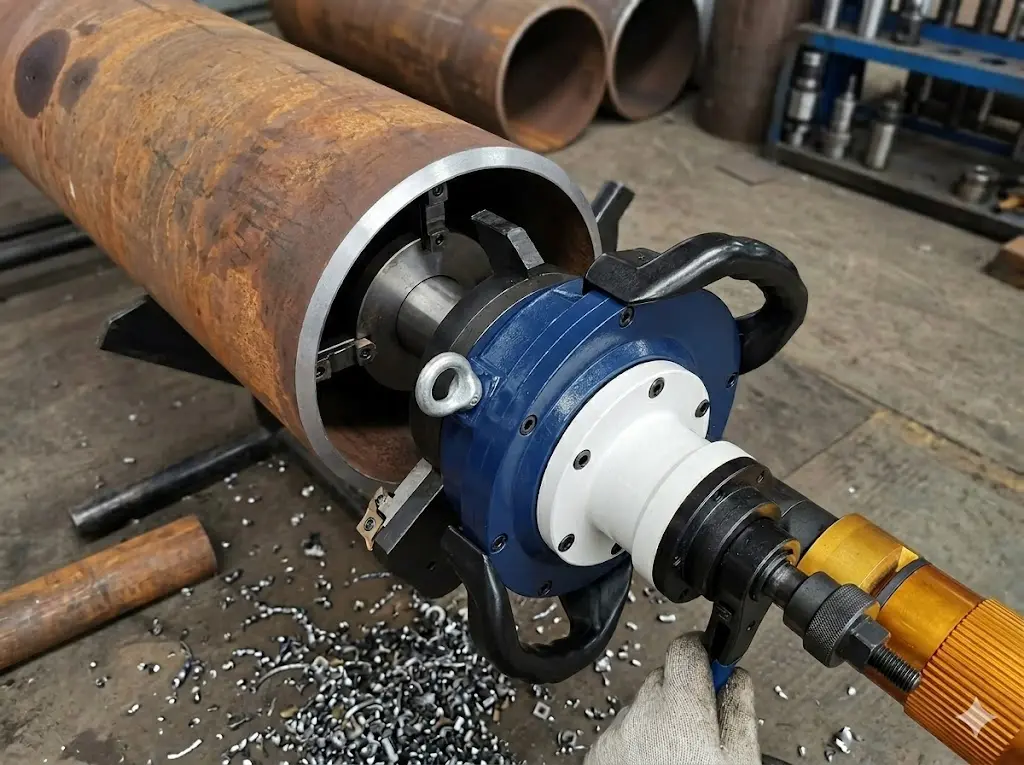
Beveling Machine Maintenance: A 15-Minute Weekly Routine to Prevent Breakdowns
The difference between a beveling machine that lasts 8 years and one that dies in 18 months isn't build quality—it's maintenance. Here's the 15-minute weekly routine that prevents most of the breakdowns I see.
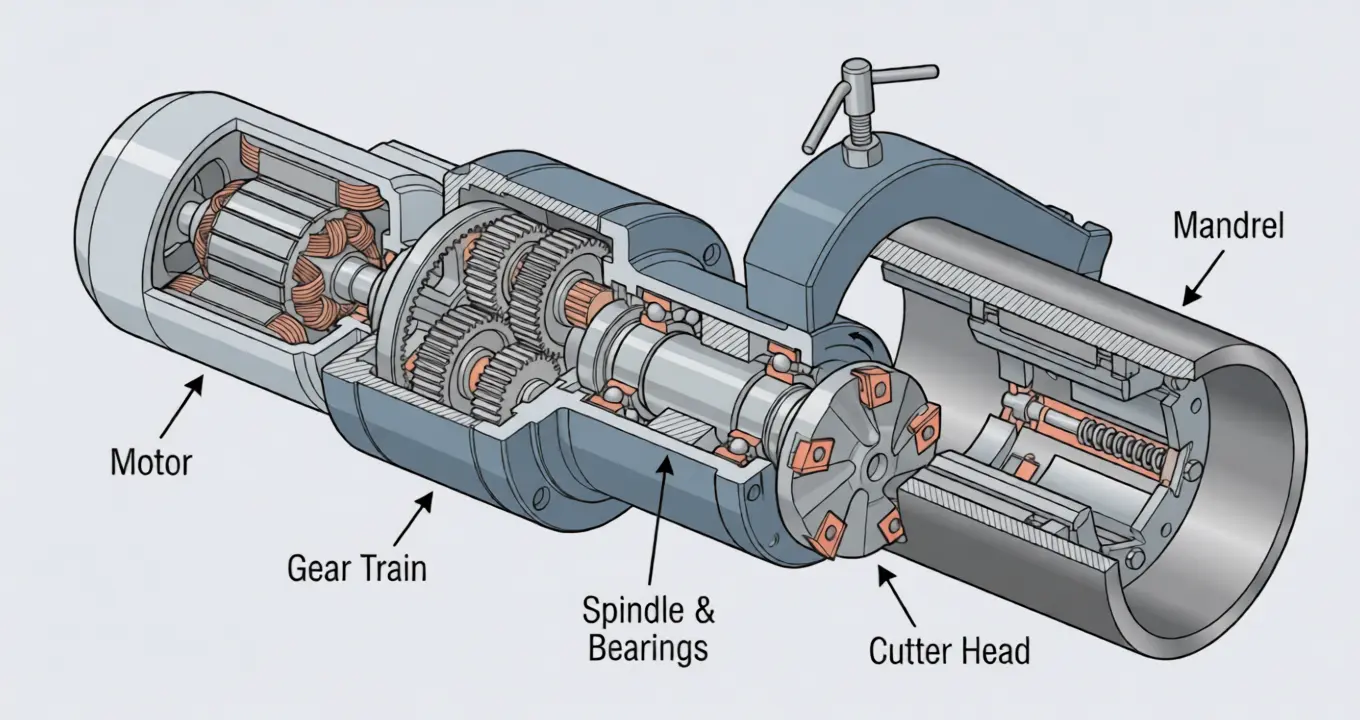
How Beveling Machines Actually Work: A No-BS Explanation for Non-Engineers
You don't need an engineering degree to understand how your beveling machine works. But understanding the basics will make you a better operator, a smarter buyer, and save you from expensive mistakes.
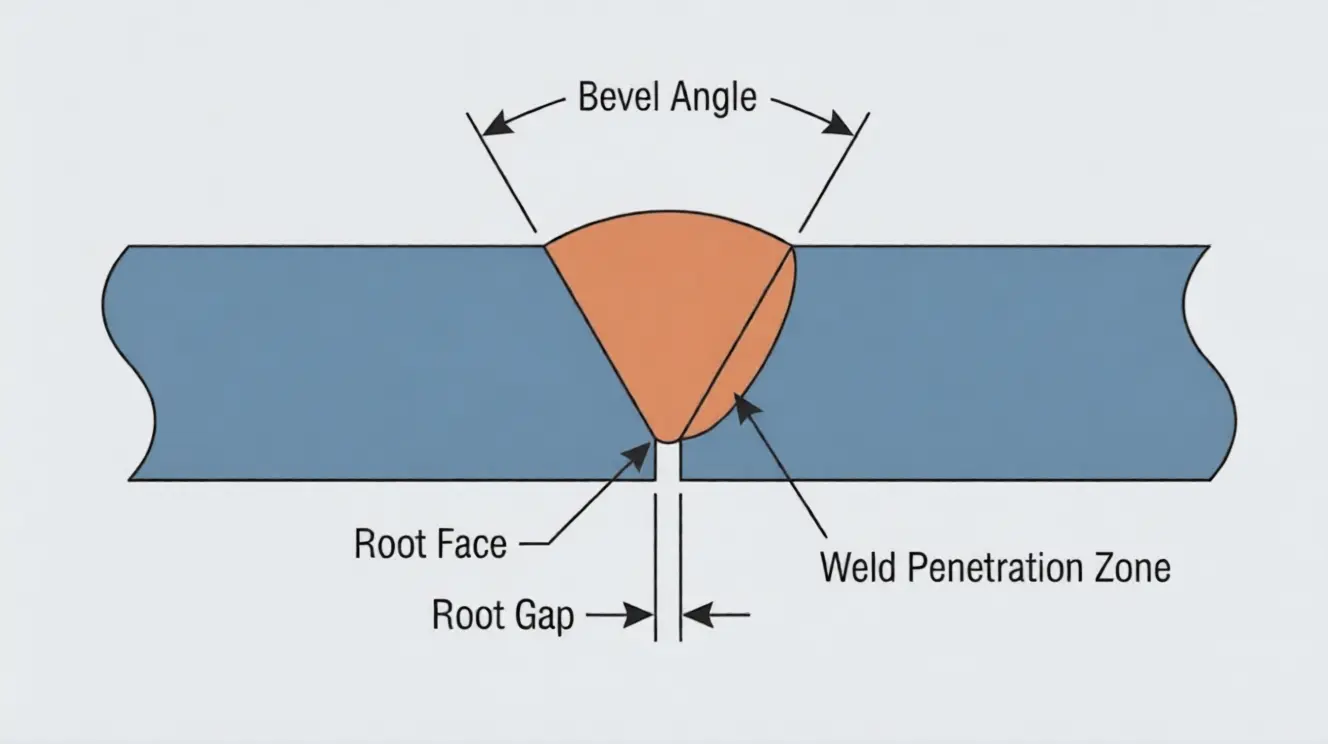
What Is Pipe Beveling and Why Every Welded Joint Depends on It
Everyone learns what pipe beveling is. Almost nobody learns why it matters until they fail an inspection. Here's what beveling actually does to your weld joint—explained by someone who's seen thousands of bevels done right and wrong.
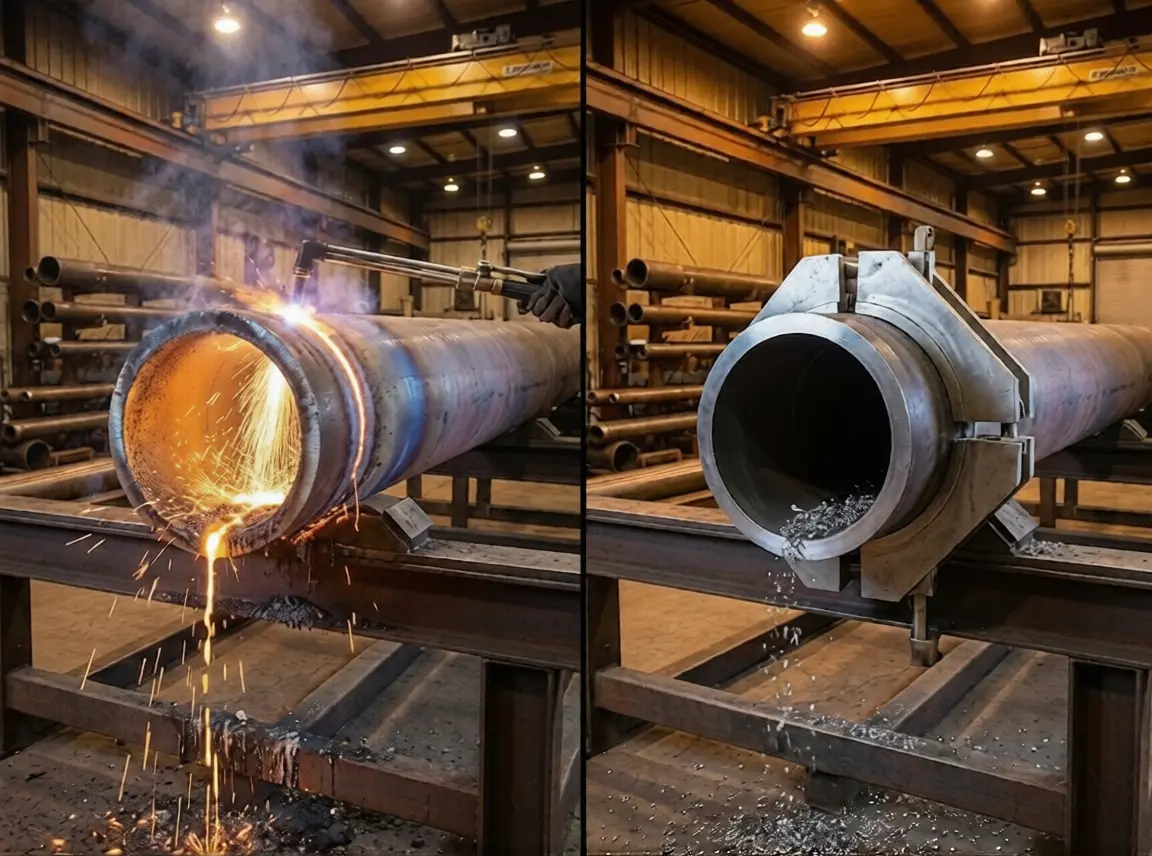
Cold Cutting vs Thermal Cutting: HAZ, Cost & Quality
Thermal cutting is faster to set up and cheaper per cut—until you factor in the grinding, the hardness testing, the rejected welds, and the PWHT that nobody budgeted for. Here's what actually happens to your pipe when you cut it with heat.
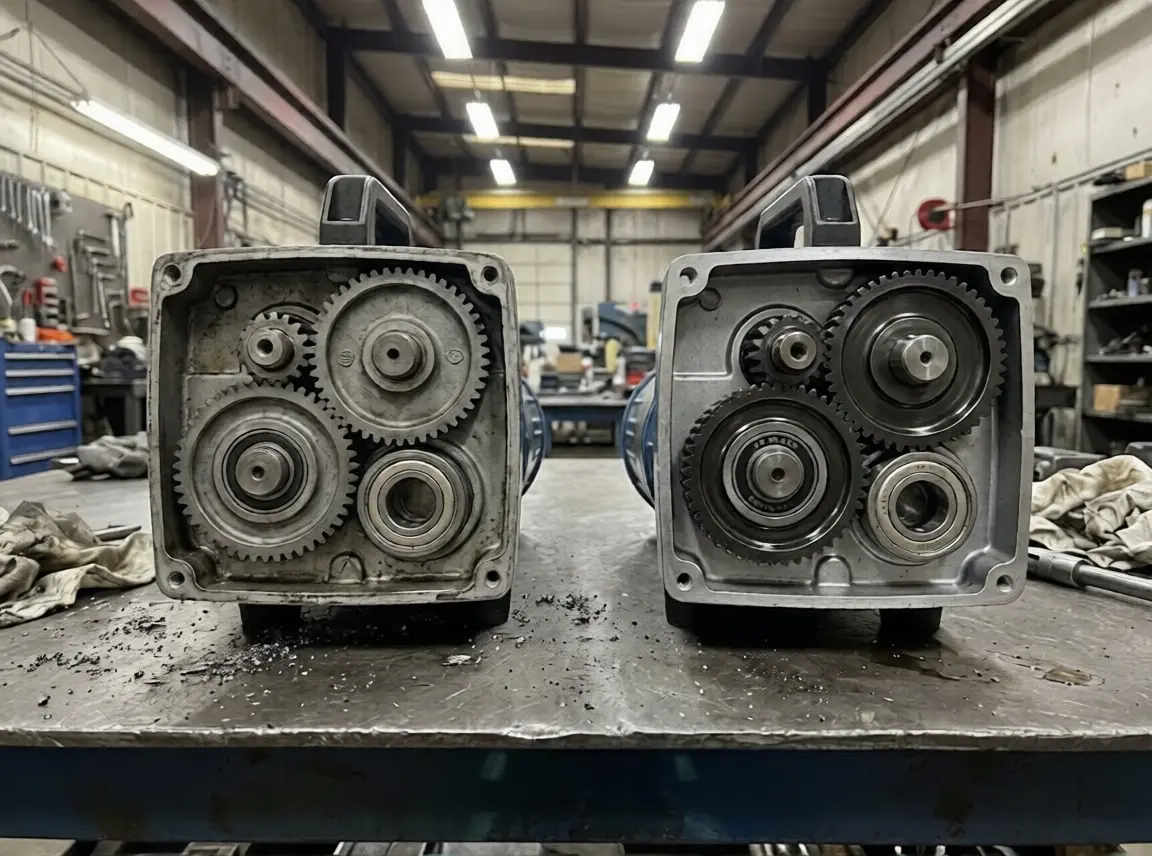
Why Two 'Identical' Beveling Machines Can Cost 3x Different — And How to Avoid Overpaying
You get three quotes for 'the same' beveling machine. One is $4,000, one is $8,000, one is $12,000. They all look identical on paper. Here's what's actually different—from someone who manufactures them.
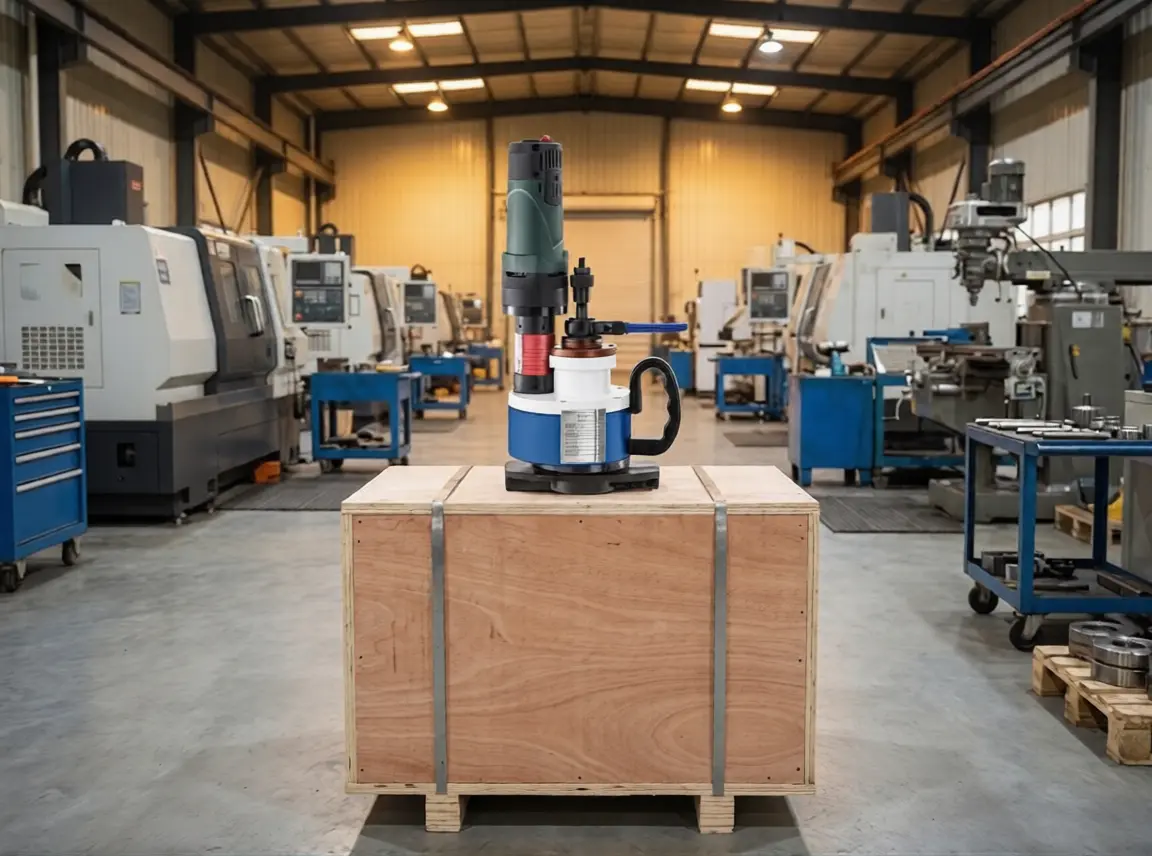
Buying a Beveling Machine from China: What Nobody Tells You About MOQ, Lead Time, and Quality Control
Every 'how to buy from China' article tells you to use Alibaba, negotiate hard, and get a sample. That advice is fine for phone cases. For a $5,000–$50,000 industrial machine that your welders depend on, you need a completely different playbook.
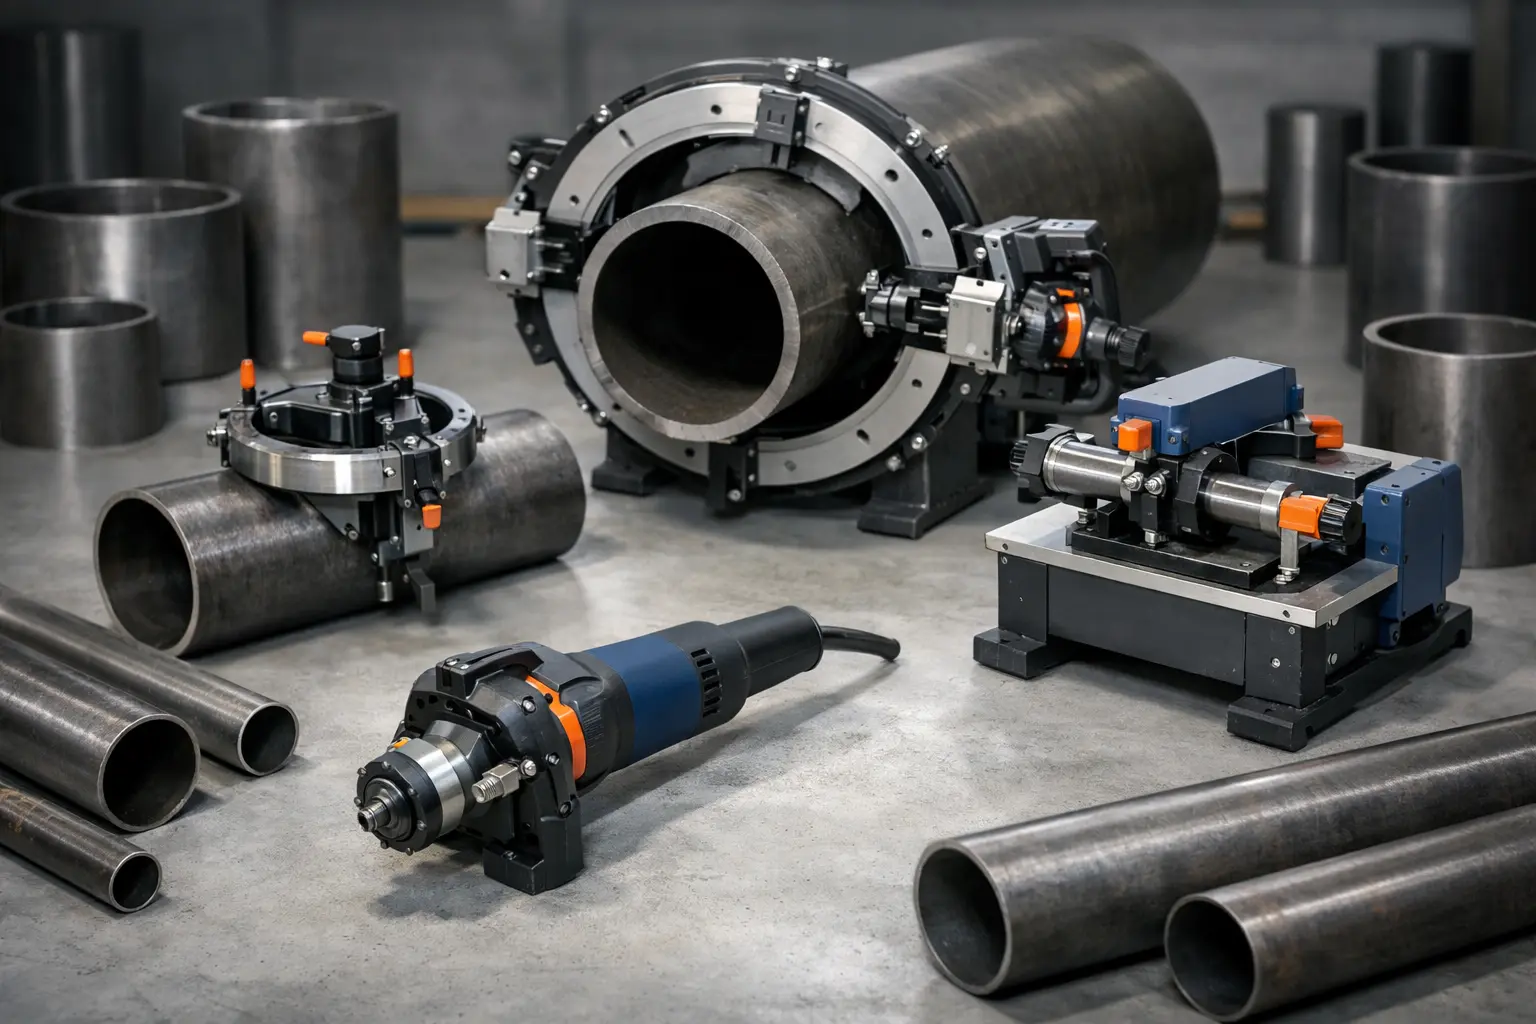
Best Pipe Beveling Machines 2026: Buyer's Guide by Pipe Size
Every 'best pipe beveling machine' article ranks machines by brand. That's useless. The right machine depends on your pipe size, wall thickness, where you're working, and what code you're welding to. Here's how to actually choose.
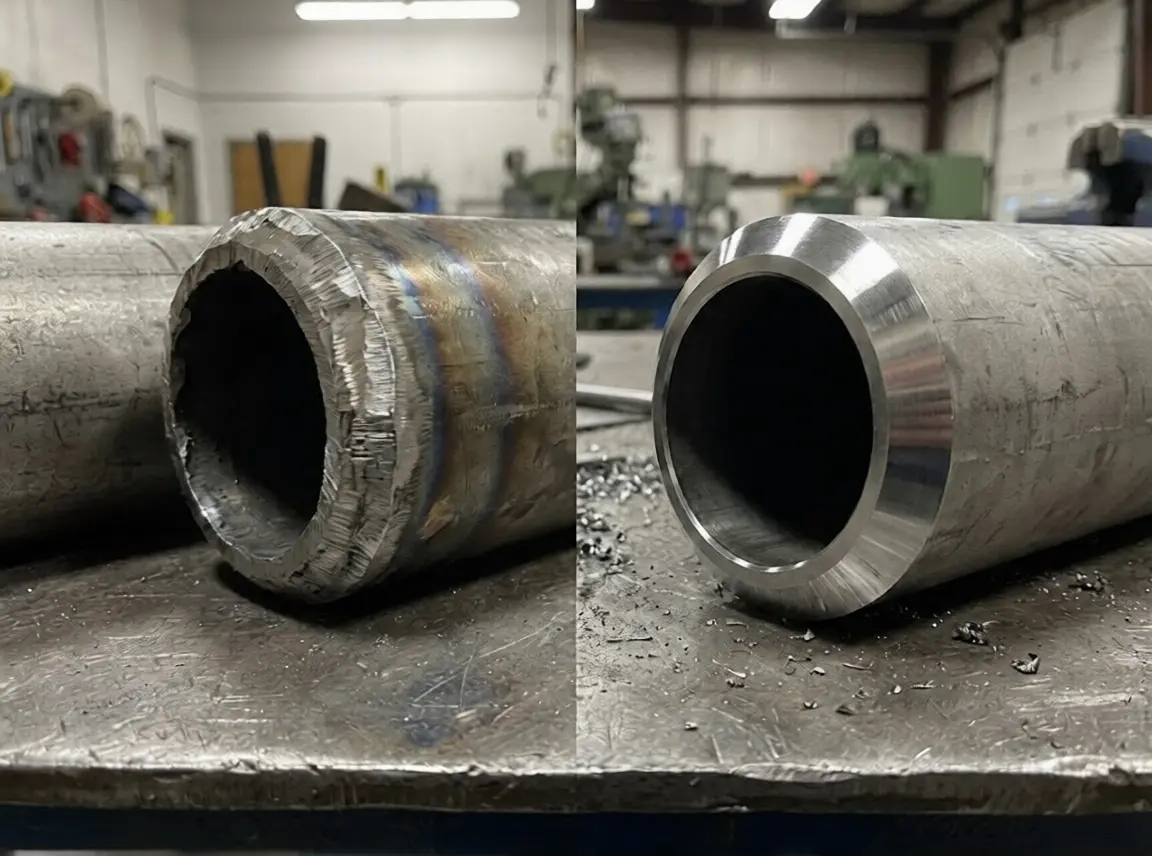
Angle Grinder vs Beveling Machine: Real Cost Comparison
Angle grinders are cheap and familiar. They're also the most expensive weld prep method you can choose—once you count the rework, the injuries, and the failed inspections.
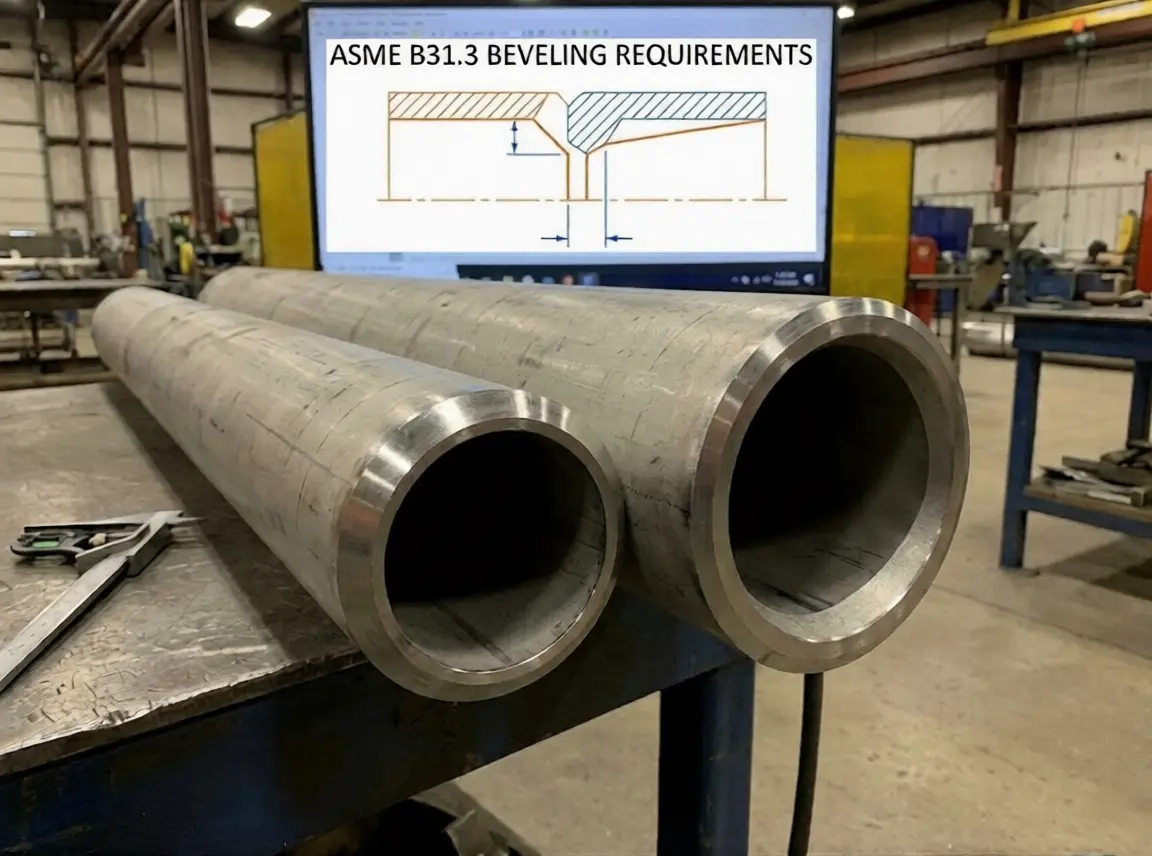
ASME B31.3 Beveling Requirements: The Complete Reference
Most shops think they know ASME B31.3 beveling requirements. Then they fail an X-ray and blame the welder. The real problem is upstream—at the bevel.
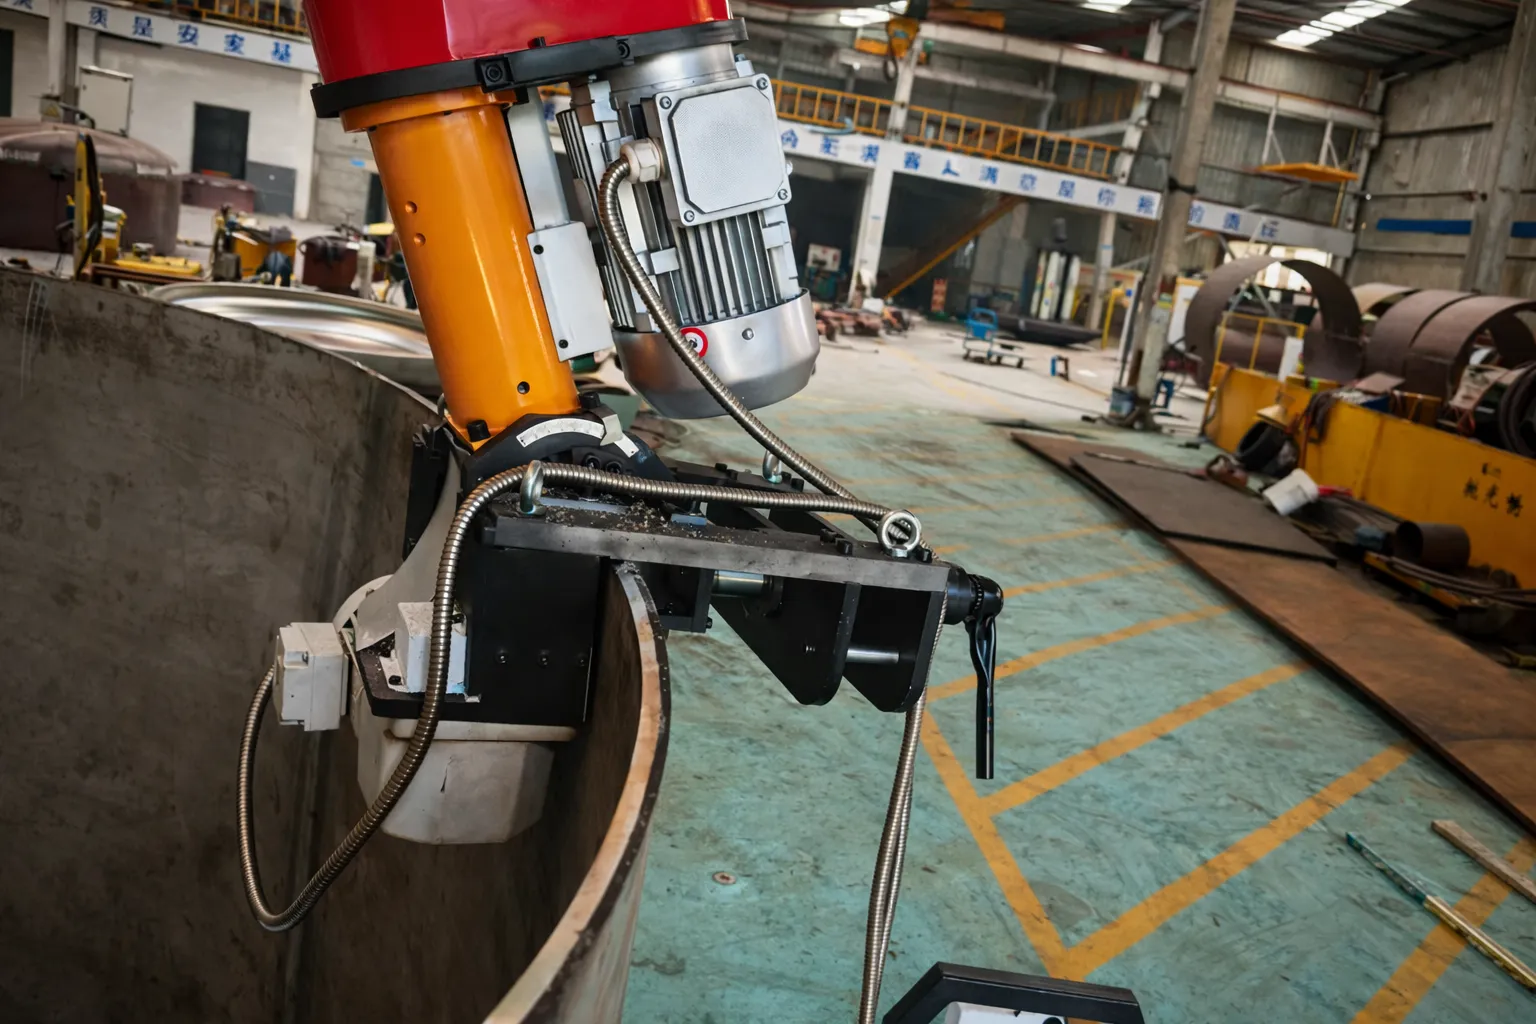
How a Pressure Vessel Factory Eliminated Manual Grinding on Large Cylinders with the DMM-YG-80
A pressure vessel factory switched from manual grinding to the DMM-YG-80 for large cylinder beveling. Here's what changed—and why I think most shops wait too long to make this switch.
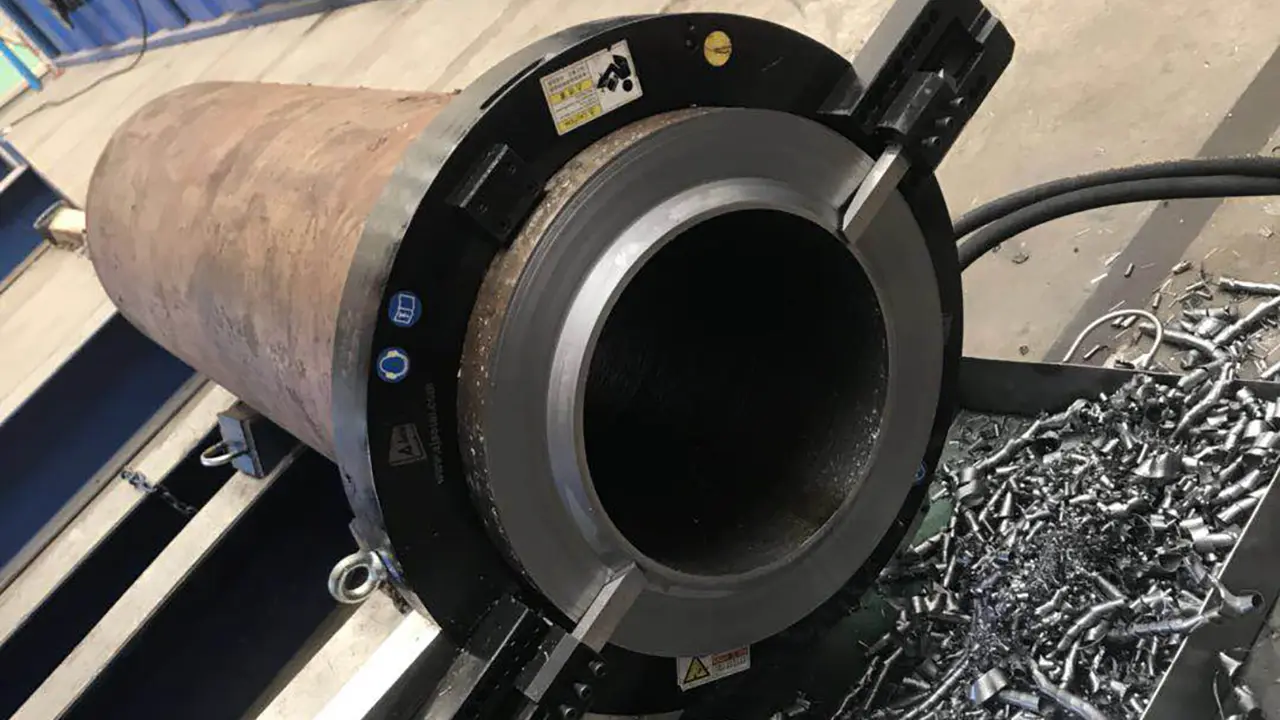
7 Pipe Bevel Types Compared: V, J, U, Compound & More
If you're cutting 37.5° V-grooves on every pipe regardless of wall thickness, you're probably wasting 30% on filler metal and doubling your welder's arc time.
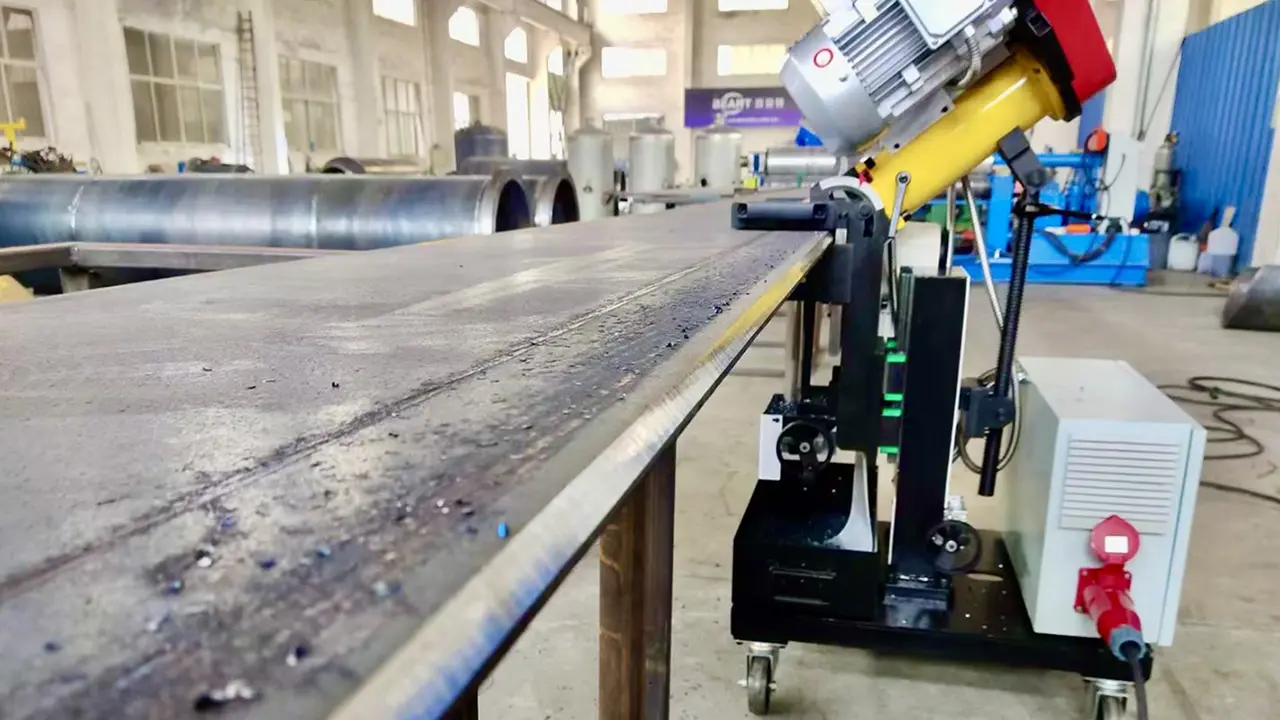
Plate Edge Milling Guide: Stop Grinding Your Profits Away
Walk into any traditional steel workshop and you hear angle grinders screaming. In 2026, that sound is just wasted money. Edge milling changes everything.
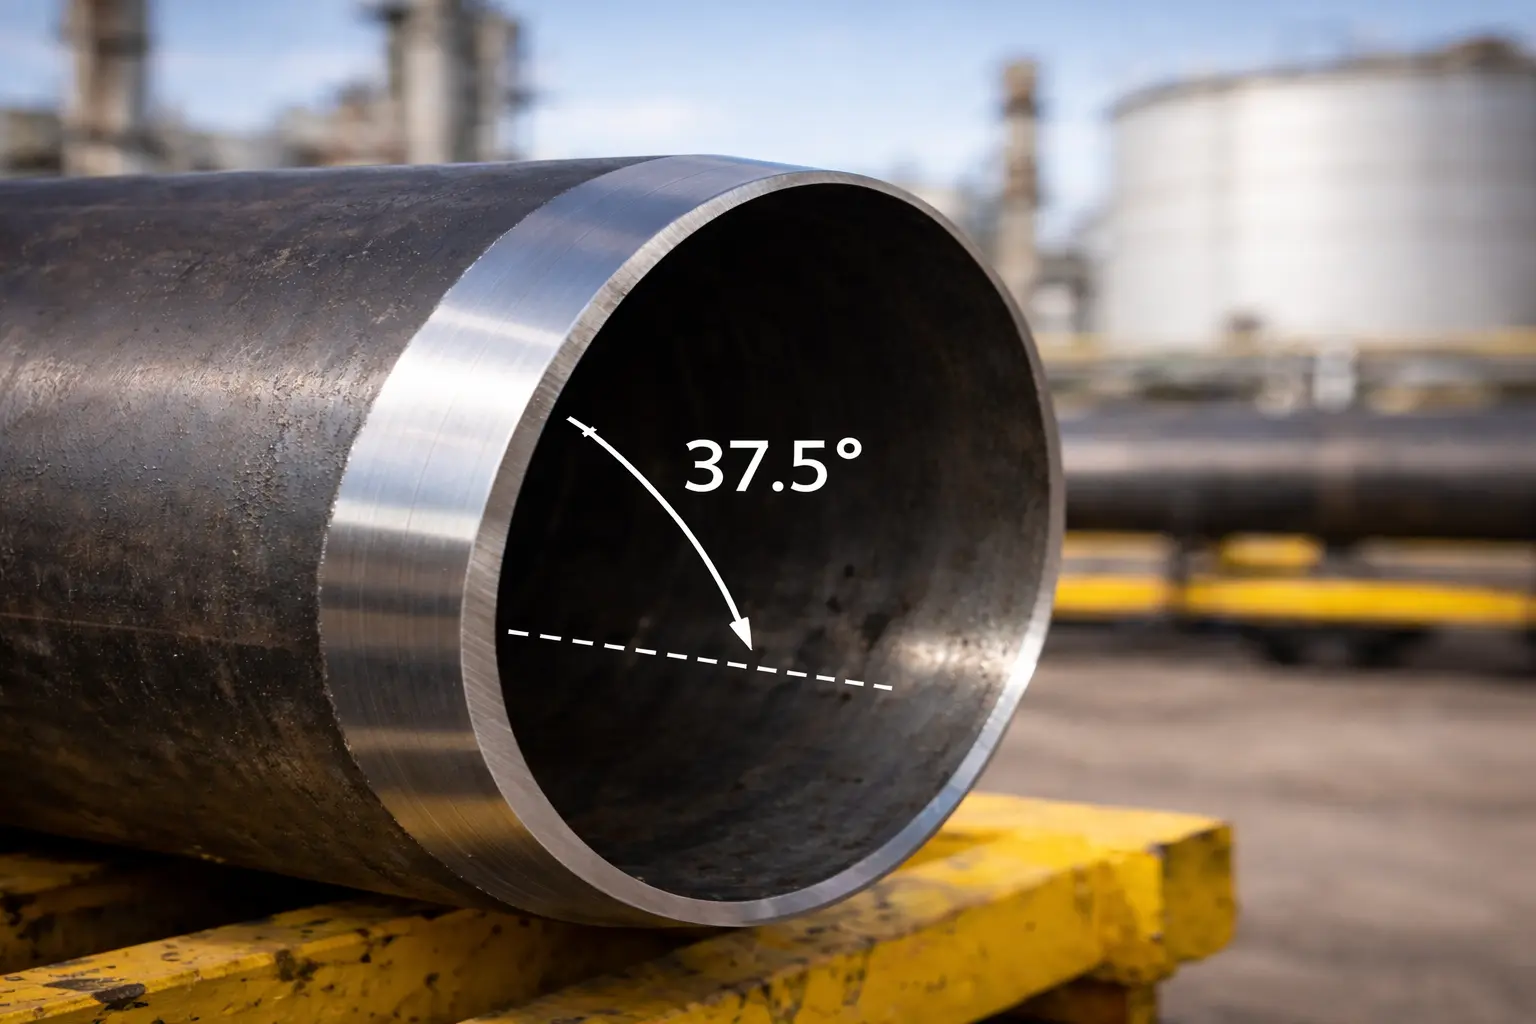
Pipe Bevel Angles by Code: ASME, AWS & API Cheat Sheet (2026)
37.5° isn't the answer to everything. Here's what your welding procedure actually requires—and why getting it wrong means expensive rework.
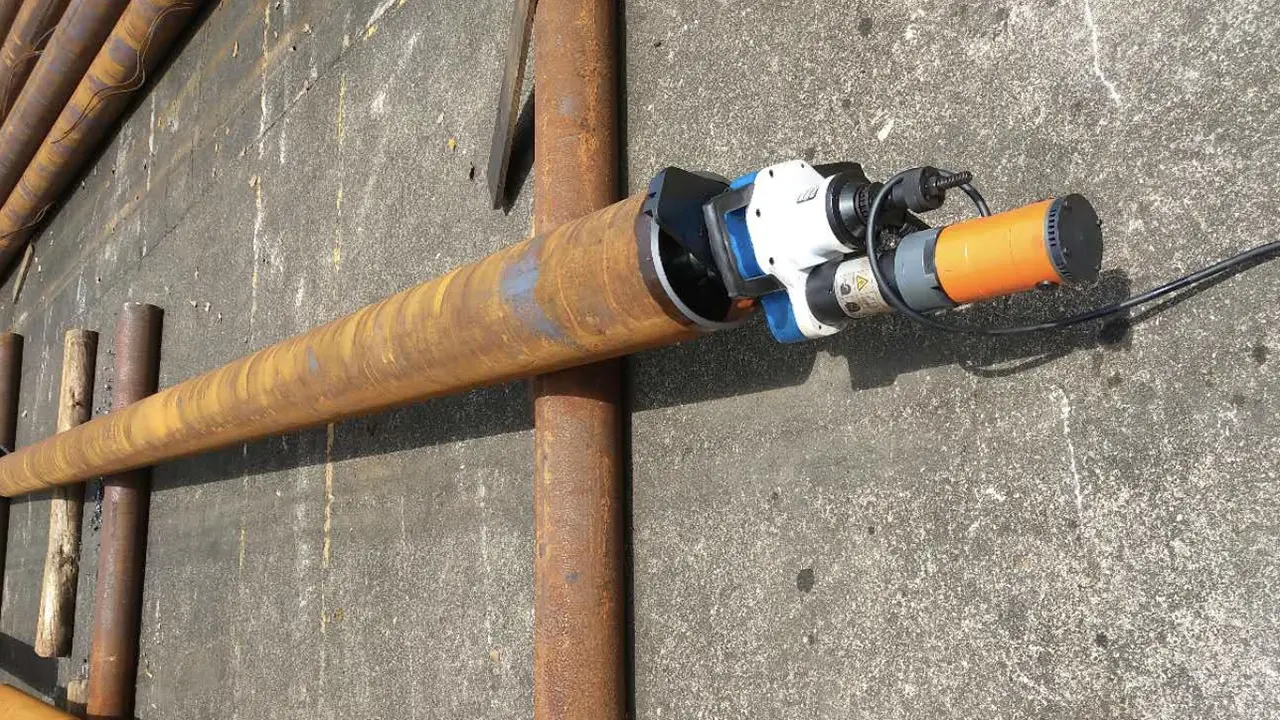
Portable vs Stationary Beveling Machines — Start With Where the Work Is
The 'portable vs stationary' question is usually asked the wrong way. Here's the right way to think about it.
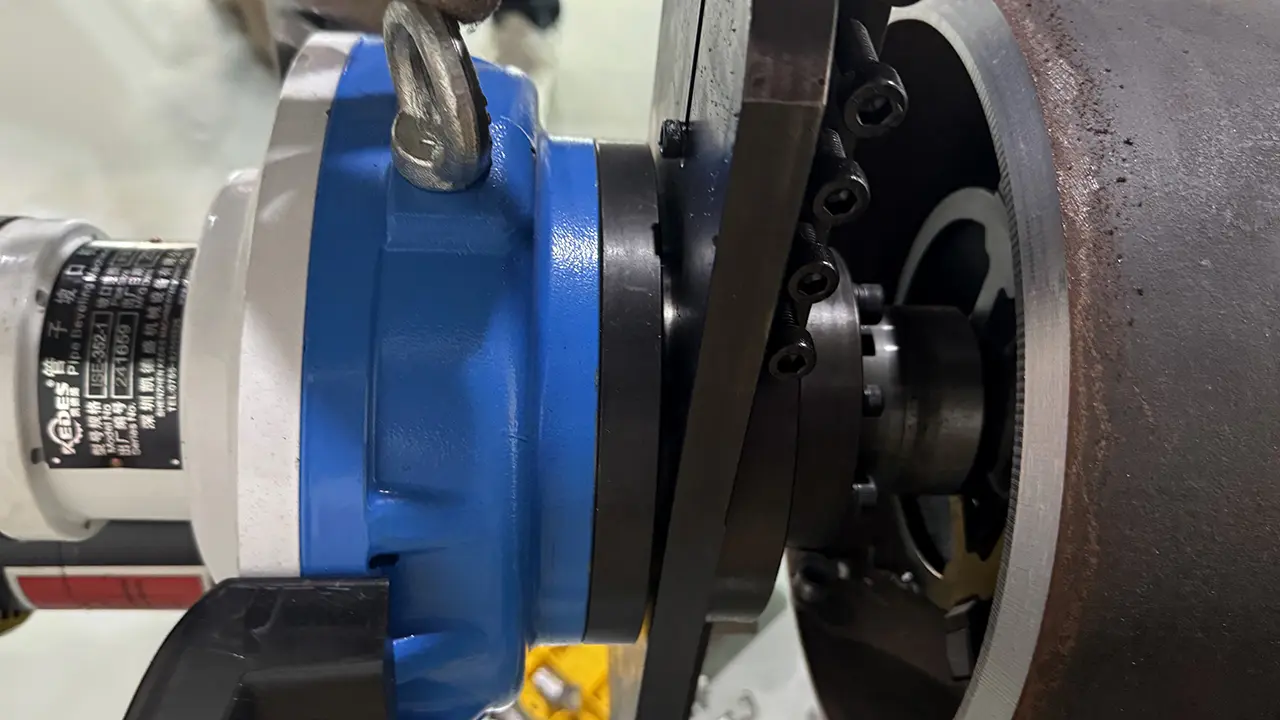
ID Mount vs OD Mount Pipe Bevelers: How to Choose the Right One
The real deciding factor between ID and OD mount bevelers isn't what most salespeople tell you. Here's what actually matters.
Get a quote within 24 hours.
Send us your spec sheet, pipe schedule, or drawing — our engineers reply with pricing, lead time, and recommended models.
- 01Send specs & drawings
- 02Receive quote within 24h
- 03Confirm & manufacture