
A Compound Bevel Is Two Angles Doing Two Jobs
Most people meet the compound bevel the wrong way: as “that weird double-angle thing on the drawing.” So they cut a single 37.5° V instead and hope the inspector doesn’t notice. On thick wall, the inspector always notices — in the filler-metal bill, if not on the RT film.
Here’s the mental model I give every customer. A weld prep has to satisfy two demands that fight each other:
- Open the root enough that the welder can reach in and fuse the first pass. That wants a steep angle (37.5°).
- Don’t open the cap any wider than necessary, because every extra degree at the top multiplies the volume the welder has to fill. That wants a shallow angle (10°).
A single-angle V can only pick one. A compound bevel picks both — 37.5° down low where the root lives, 10° up high where volume hides. That’s the whole idea. Everything else is dimensions.
If you want the full bevel-profile landscape first, my 7 pipe bevel types comparison puts compound next to V, J and counterbore. This page is compound-only, because the search data says people land on “compound bevel” without ever getting a straight answer on the angles.
Compound Bevel Angles and Dimensions
Here is the standard set per ASME B16.25. As always, your qualified WPS is the final word:
| Element | Standard Value | Notes |
|---|---|---|
| Lower (root) angle | 37.5° ± 2.5° | Keeps the root open for penetration — same as a normal V |
| Upper (cap) angle | 10° ± 1° | The volume-saver; runs from the transition to the OD |
| Transition point | ~19 mm from root face | Lower 37.5° section covers the first ¾ in of wall |
| Root face (land) | 1.6 mm ± 0.8 mm | Same role as on any bevel — controls burn-through |
| Root gap | 1.6 mm ± 0.8 mm | Per fit-up and WPS |
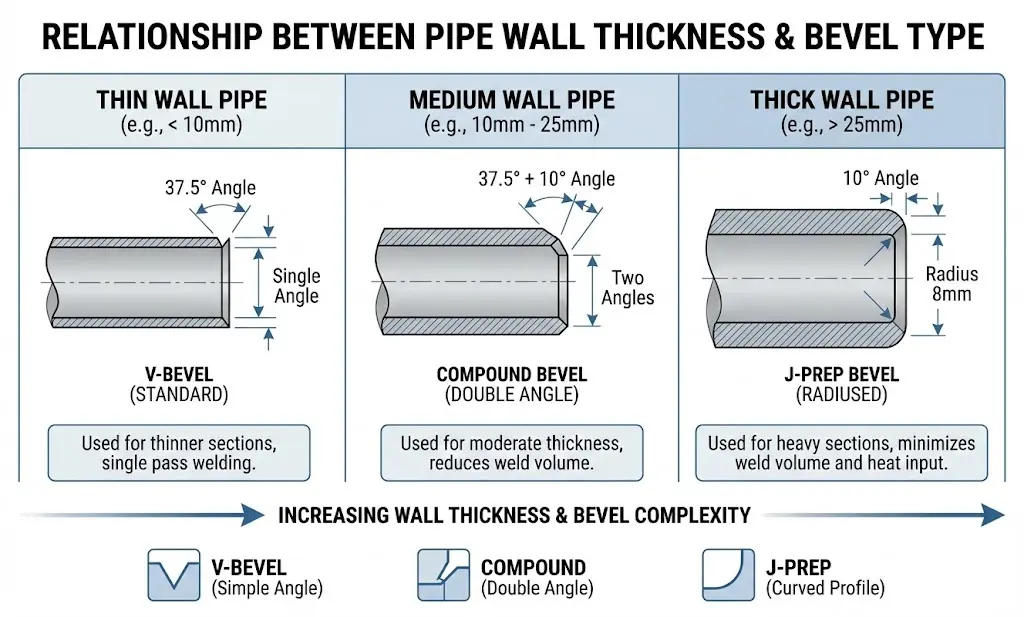 Wall thickness is the trigger: single V up to 22 mm, compound bevel above it
Two things I always flag:
- The transition point is not arbitrary. It’s set so the steep section covers the root and second pass; the 10° takes over only once the welder no longer needs wide access. Move it up and you waste metal; move it down and you choke root access.
- Compound is the “first upgrade,” not the last. It sits between a single V and a J-bevel — more savings than a V, less tooling cost than a J. For many shops it’s the sweet spot.
Compound Bevel vs V-Groove vs J-Prep
The three are points on one curve: how aggressively do you fight weld volume, and how much tooling will you pay for it?
| Prep | Geometry | Filler vs V | Tooling Cost | Best Wall Range |
|---|---|---|---|---|
| Single V | One angle (37.5°) | Baseline | Lowest | ≤ 22 mm |
| Compound | Two angles (37.5° + 10°) | −25 to −40% | Low (dual-angle head / 2 passes) | 22–40 mm |
| J-prep | Radius + near-vertical wall | −40 to −50% | Higher (J form tool) | > 25 mm, high joint count |
My position: on 22–40 mm wall with a moderate joint count, the compound bevel is usually the right call — it captures most of the volume savings without the J-prep form-tool investment or the tighter fit-up sensitivity. Above 40 mm wall or on big repeating runs of alloy pipe, the J-bevel starts to win. (The full V-vs-J volume math is in my bevel types guide.)
When to Use a Compound Bevel
Reach for it when:
- Wall thickness is 22–40 mm. This is the ASME B16.25 zone where a single V starts hemorrhaging filler but a full J-prep is overkill.
- You want savings without new form tooling. A compound bevel can be cut as two angle passes on a machine you already own — no special insert profile required.
- Root access still matters. The 37.5° lower section keeps the root as open as a standard V, so your existing root-pass procedure barely changes.
And skip it when:
- Wall is under 22 mm — a single V is cheaper and the volume savings are negligible.
- Wall is over 40 mm with hundreds of joints — the J-prep’s bigger savings justify its tooling.
- You have no machining access — like every quality bevel, a compound profile cannot be hand-ground to a repeatable transition.
How to Cut a Compound Bevel
There are two practical routes, and which one you use decides your machine choice:
- Dual-angle (compound) tool head — a single setup cuts both angles at once. Fastest in production; needs a machine built to hold a compound head rigidly through the full circumference.
- Two angle passes — cut the 37.5° lower section, then re-set the tool to 10° and cut the upper. Slower per joint, but it works on most adjustable-angle beveling machines without special tooling. This is why compound is the “no new tooling” upgrade.
Either way, the make-or-break is rigidity. A machine that bevels a single 37.5° all day can chatter when it’s holding two angles on 30 mm+ wall, because more of the tool is engaged. Our ISE-II heavy-duty ID-mount series is built for exactly this — it runs compound and J-prep tooling as stock options. For 3/4”–48” field work, the split-frame series is compound-capable too.
Not sure whether to mount inside or outside the bore? I broke that down in ID vs OD mount pipe bevelers.
Code Acceptance
The compound bevel isn’t a workaround — it’s in the standard:
| Code | Compound Bevel Status |
|---|---|
| ASME B16.25 | Explicitly specifies the 37.5° + 10° compound profile for wall thickness over 22 mm |
| ASME B31.3 / B31.1 | Joint geometry follows the qualified WPS; compound qualifies like any groove. See my ASME B31.3 beveling guide |
| AWS D1.1 | Compound-angle groove details are permitted within dimensional limits |
| API 1104 | Joint design qualified through the welding procedure, not a fixed geometry |
For where each code’s numbers actually come from, see the bevel angles by code reference.
Real Case: 30 mm Wall Vessel Nozzle
A pressure-vessel shop was welding 30 mm wall nozzles with a full 37.5° V — because their old machine couldn’t hold a second angle. We requoted the joint as a 37.5° + 10° compound, cut as two passes on an ISE-II:
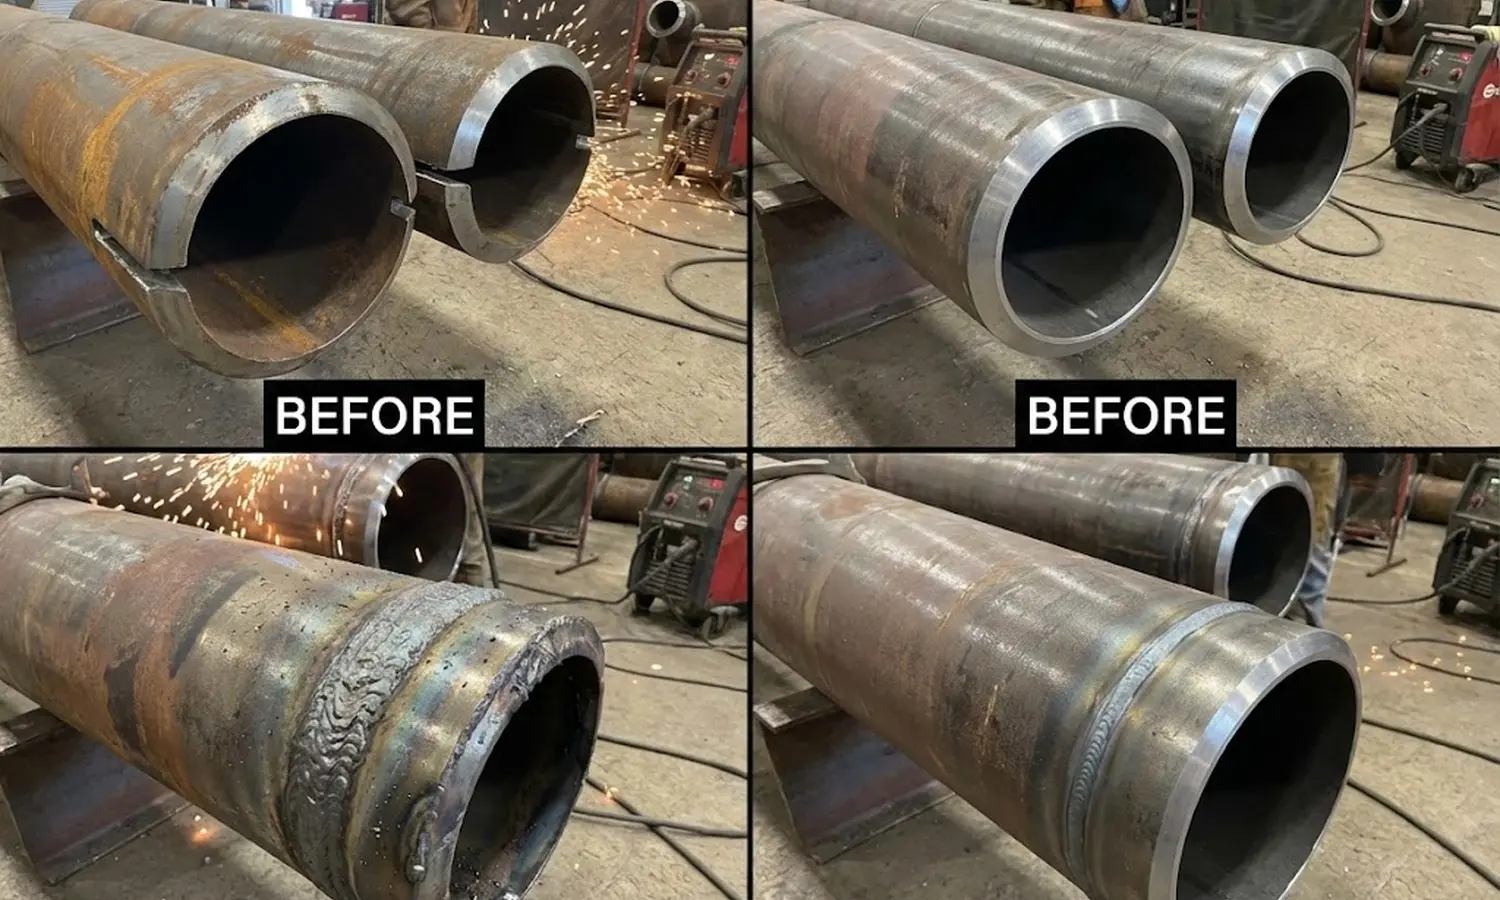 Same 30 mm joint: the full V-groove (left) carries far more weld volume than the volume-trimmed prep (right)
- Filler metal: −31%
- Passes: 14 → 10
- Arc time per joint: −28%
- Root procedure: unchanged (37.5° root section identical to the old V)
No new form tooling, no WPS root-pass change — just the second angle. The savings paid back the setup time inside the first shift.
Where to Go From Here
→ Heavy wall and want the upgrade without new tooling? Browse our pipe beveling machine lineup — the ISE-II and split-frame series cut compound profiles.
→ Tell me your wall thickness, material and joint count and I’ll tell you whether compound or J-prep is the right move for you. Contact us here.
→ Keep reading: 7 Pipe Bevel Types Compared · J-Bevel on Pipe: Dimensions & Angles · Pipe Bevel Angles by Code