Skip to content
Category 03 / 10

Flange Facing Machines

In-situ flange sealing-face resurfacing

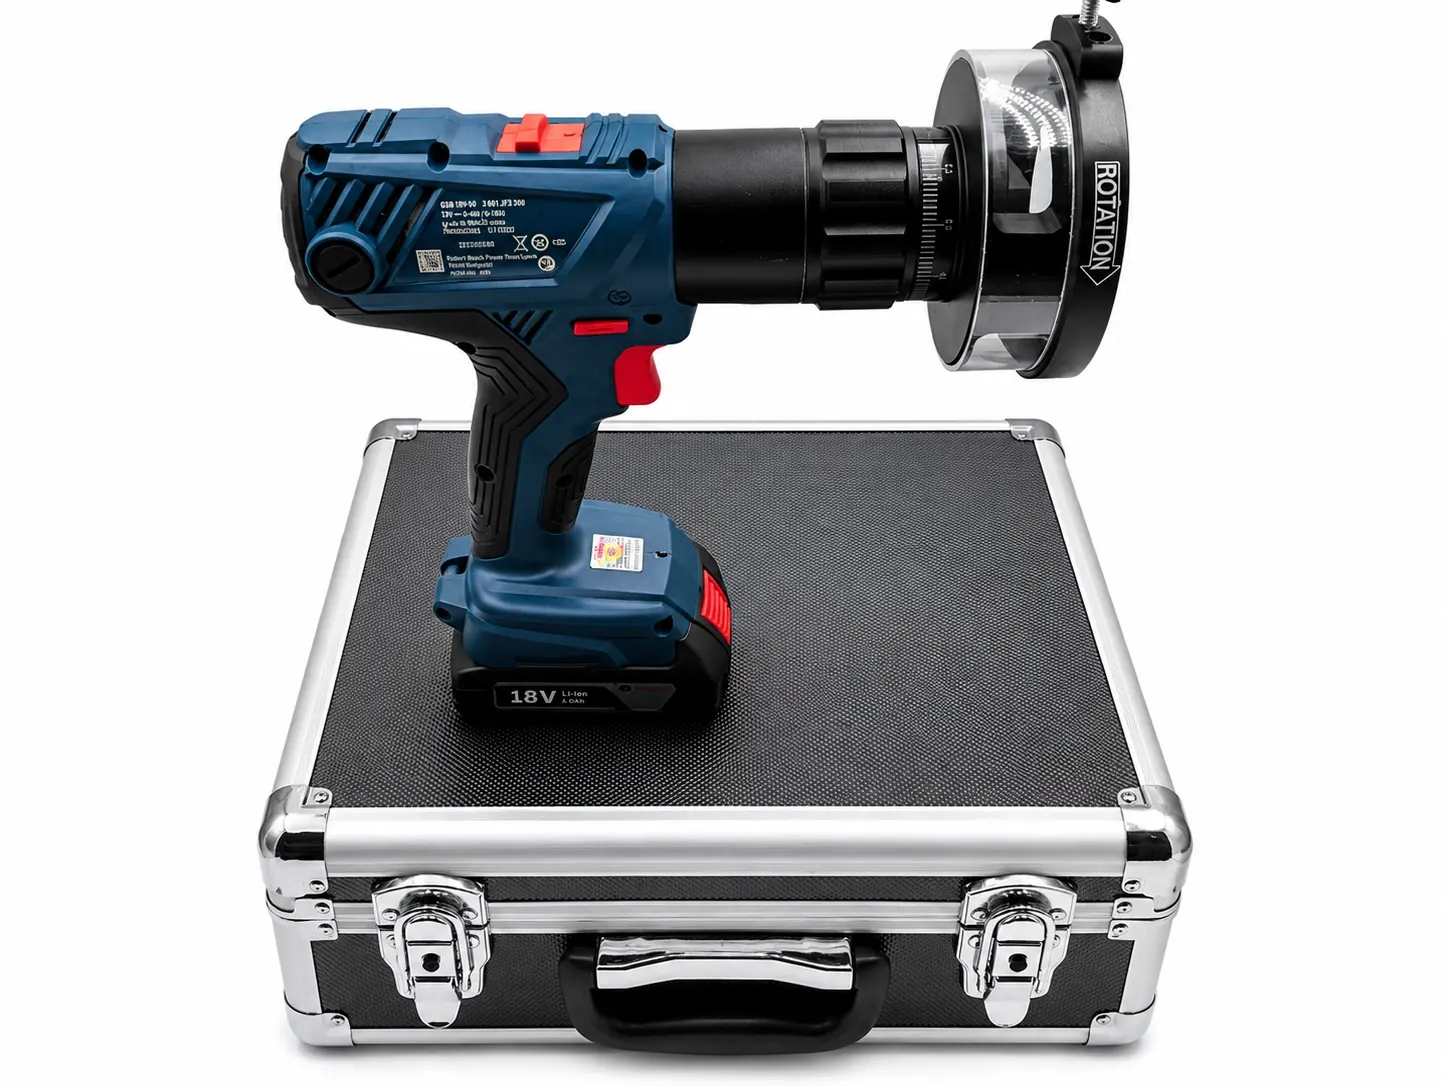
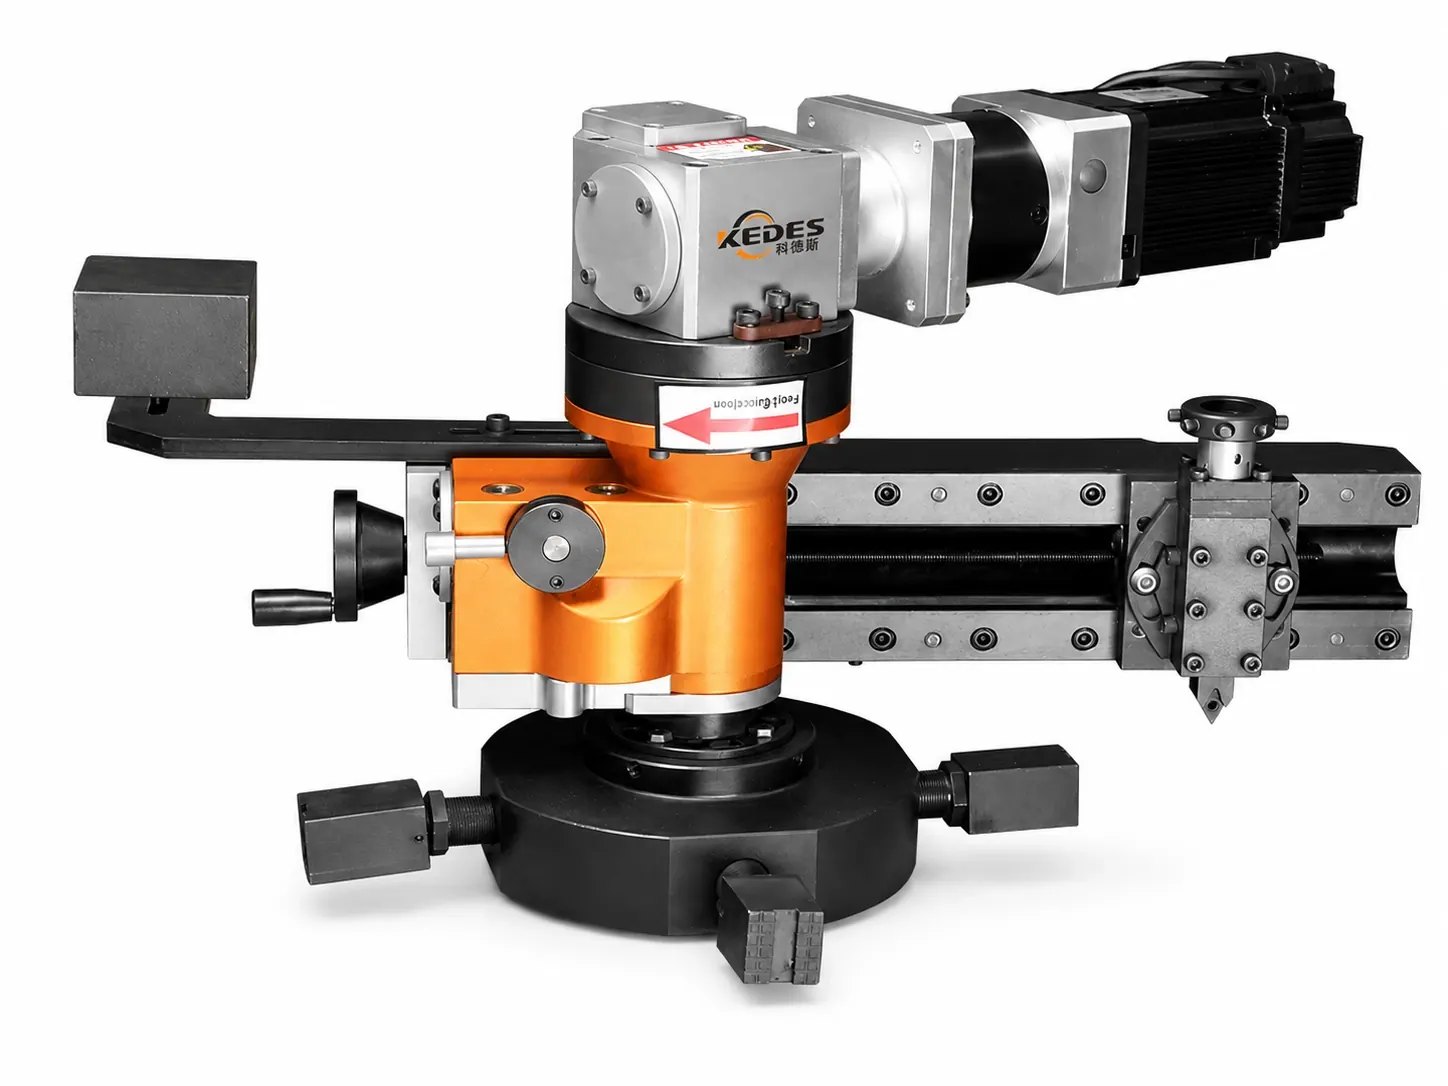
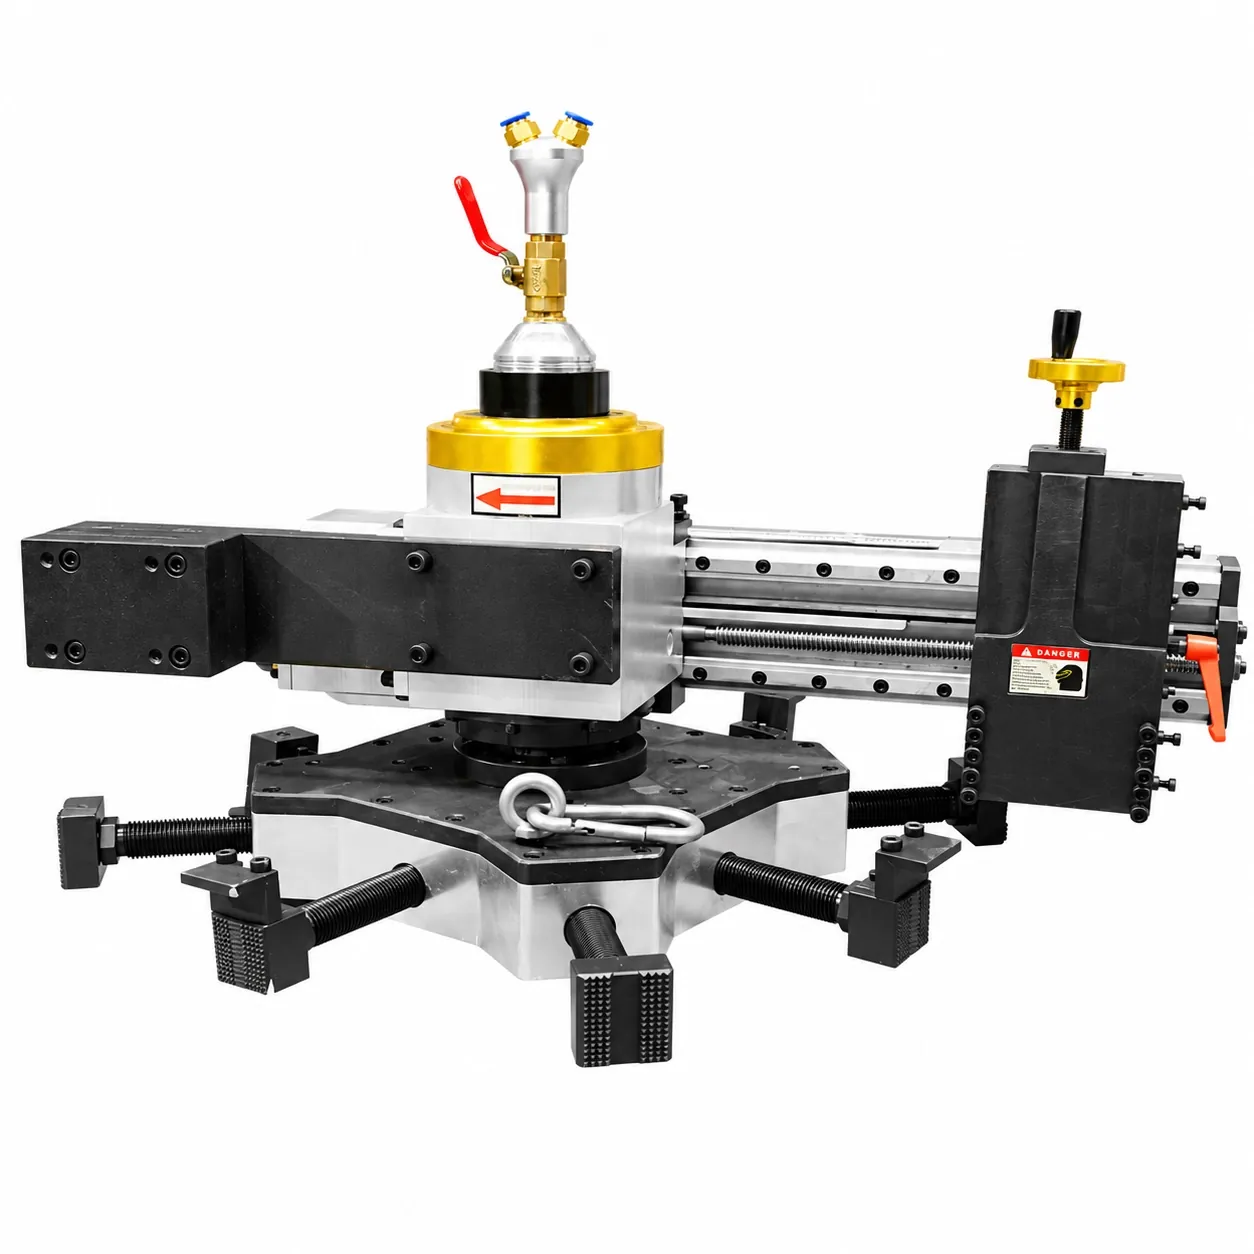
On-site rotational machining tools — portable flange facers that resurface damaged RF, FF and RTJ flange faces without removing the flange from the line. Cold cutting, mounted on the flange itself: the machine comes to the workpiece, not the other way round.

Talk to an engineer
Flange Facing Machines
02 Where it's used
Refinery valve & manifold flange resurfacing
LNG terminal flange refurbishment
Power plant valve seat & flange-face repair
Offshore platform shutdown maintenance
04 Applications in depth

Where these machines earn their keep.

01

Pipeline and pressure equipment flange maintenance

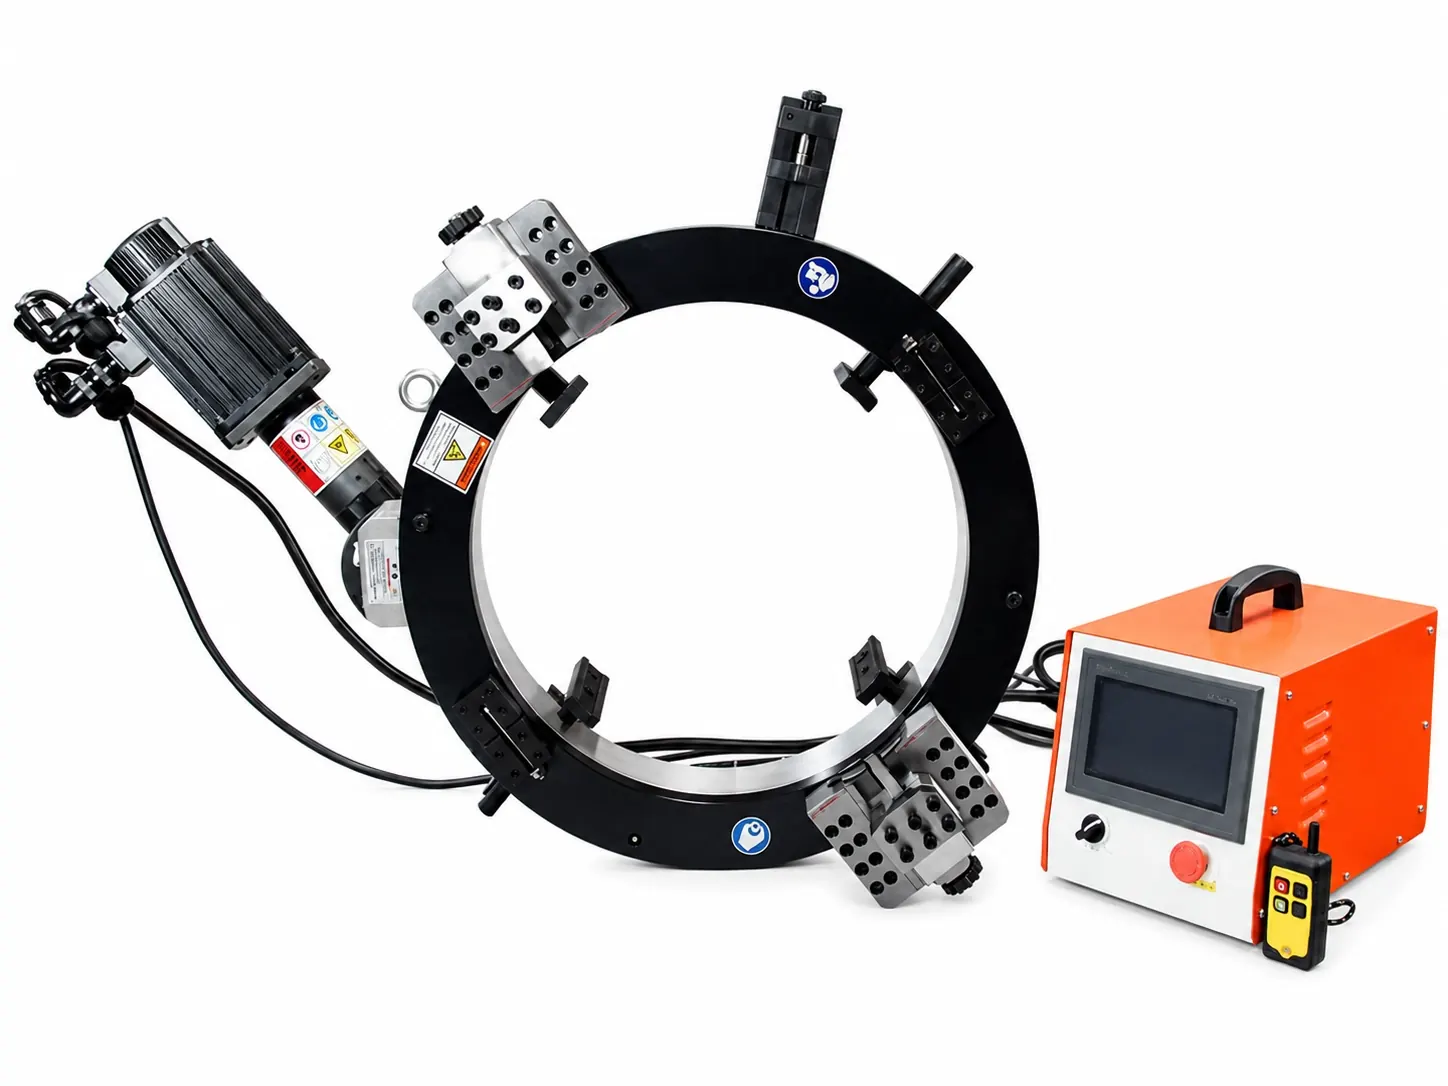
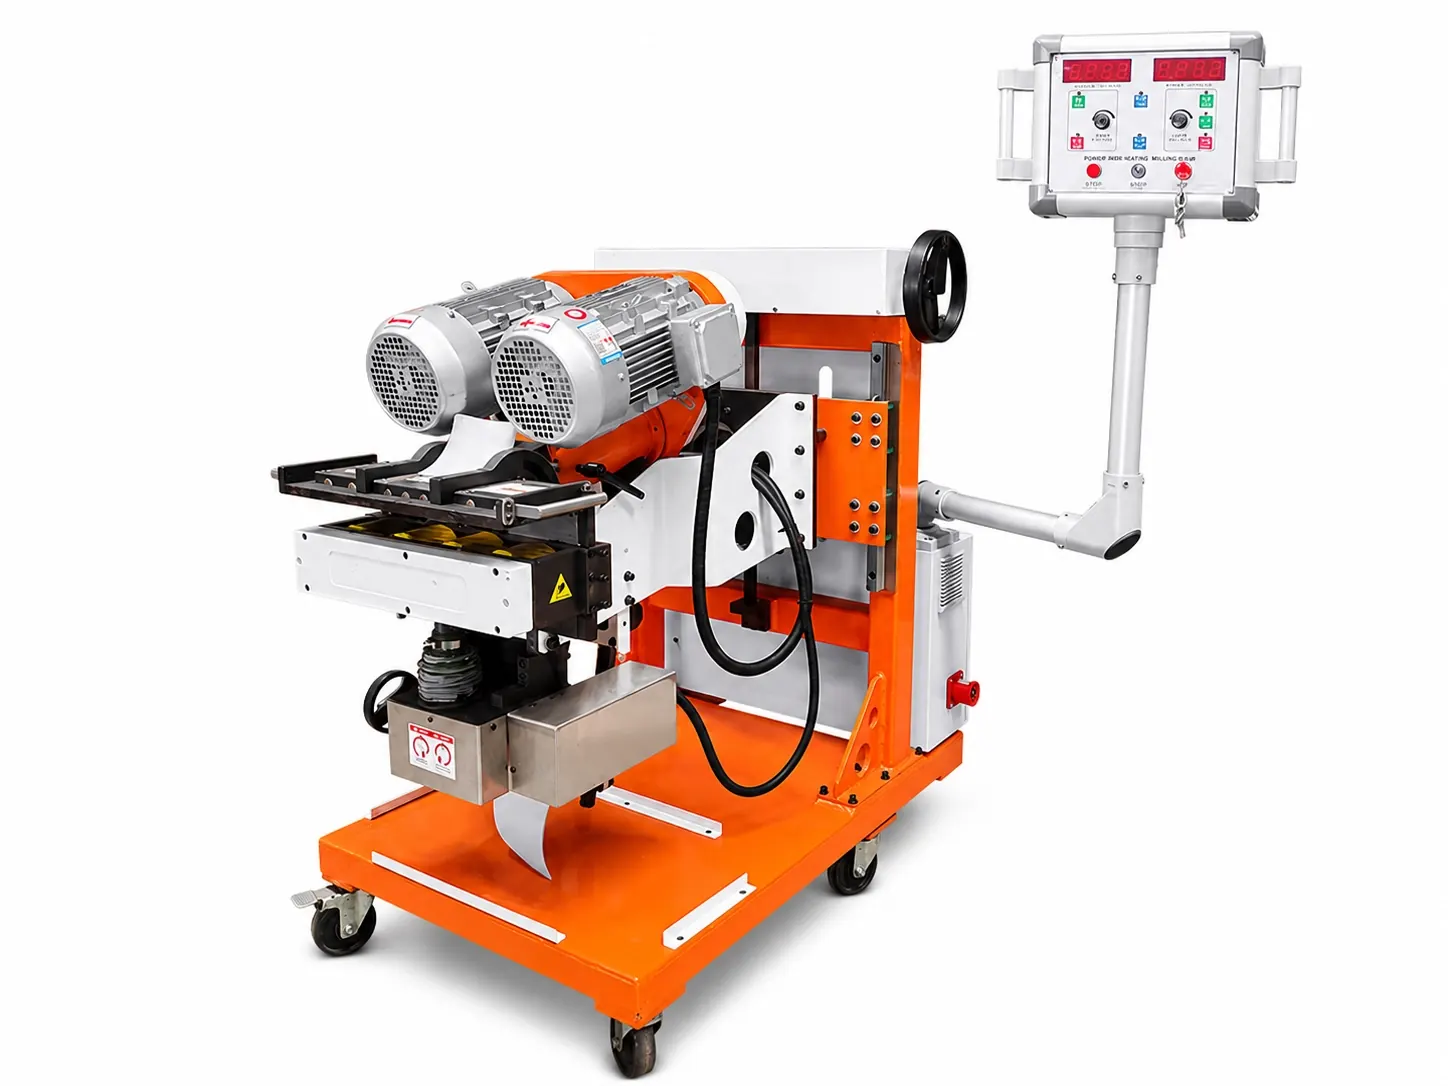
In-service flanges fail by face corrosion, gasket impingement, or RTJ groove wash. Removing the flange to a shop is rarely viable on a live pipeline — the line above it would have to come down too. The fix is an in-situ portable flange facer that mounts on the flange ID, resurfaces the face and re-cuts the groove in one setup.

For RTJ groove restoration the rules are non-negotiable: 23° walls within 0.5°, Ra ≤ 1.6 µm in the groove, concentric to the bore. For the full field procedure see how to machine RTJ grooves.
02

Sealing-face finish matched to the gasket

The flange face is not cosmetic — it is the sealing parameter. A smooth finish on a soft sheet gasket leaks; a stock finish under a smooth-face gasket leaks. Each combination has a finish band per ASME B16.5 / B16.20.

A portable flange facer controls the face finish through feed rate and insert geometry — Ra 6.3 µm for stock, Ra 1.6 µm for smooth, controlled spiral pitch for serrated. For the full gasket-to-finish matrix see flange surface finish explained.

03

Refinery turnaround and offshore shutdown work

During a TAR or offshore shutdown, every flange repair competes for hot-work permit time. Cold machining is permit-free, which on a live unit translates directly into more productive hours per shift — and sometimes the difference between hitting the start-up window and slipping it.

For the broader pneumatic-vs-electric drive decision in hazardous zones, see pneumatic machining in oil & gas safety. Bring the flange OD, groove type and area classification to the quote form and we will match a machine sized for the window you have to work in.

05 Frequently asked

Quick answers.

Can the machine refinish RTJ (ring-type joint) flanges in the field?
Yes. R, RX and BX groove tooling sets handle all three API 6A profiles on the same base unit with a tool swap. Each ships with a calibration certificate on the 23° wall angle and Ra finish. The full field procedure is in how to machine RTJ grooves.
What surface finish does the machine deliver?
Surface finish is controlled by feed rate and insert geometry: Ra 3.2–6.3 µm for stock raised-face flanges, Ra ≤ 1.6 µm for smooth and RTJ groove interiors, controlled spiral pitch for serrated faces. Always check the gasket spec — see flange surface finish explained for the gasket-to-finish matrix.
Does the flange need to come off the line for resurfacing?
No. The portable flange facer mounts on the flange ID (or OD on a damaged bore), resurfaces the face and re-cuts the groove without lifting the flange off the pipeline. Typical in-line refurbishment replaces a full removal-and-shop-repair cycle of days with a single shift on site.
What flange OD range and bolt sizes do you cover?
Our portable flange facers cover flange OD ranges from ~Ø 50 mm to Ø 2000+ mm, with model-specific bolt-pattern adaptations. Send the flange spec (size, class, groove type, area classification) and we will size the right unit.
Can the machines work in hazardous zones without hot-work permits?
Cold cutting is permit-free, which is the operational reason it dominates refinery TAR and offshore platform shutdown work. Pneumatic drive options remove the electrical ignition source for Zone 1 / Zone 2 areas — see pneumatic machining in oil & gas safety.
Next step

Get a quote within 24 hours.

Send us your spec sheet, pipe schedule, or drawing — our engineers reply with pricing, lead time, and recommended models.

  1. 01Send specs & drawings
  2. 02Receive quote within 24h
  3. 03Confirm & manufacture
Chat on WhatsApp
Chat on WhatsApp
Get a quote

Request a quotation.

Tell us pipe diameter, wall, material and country. We reply within one working shift.

WE REPLY WITHIN ONE WORKING SHIFT · GMT+8