Skip to content
Category 10 / 10

Orbital Welding Systems

Closed-head orbital welding — M200 series

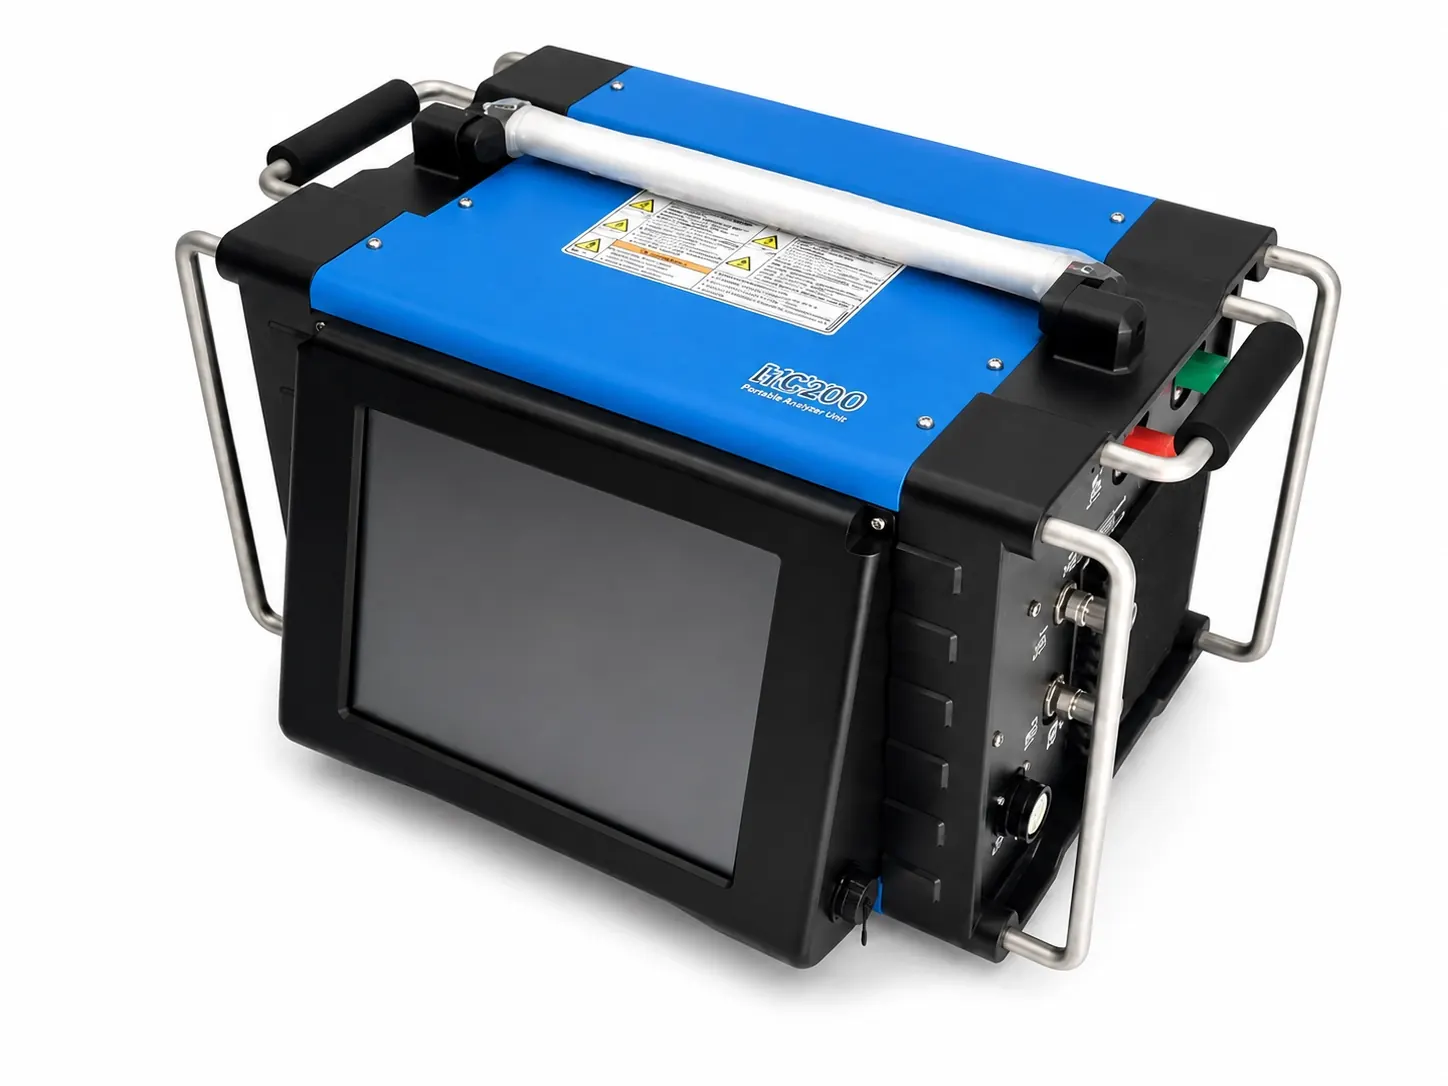
Closed-head orbital GTAW systems for repeatable, X-ray quality welds on small-bore tubing. The M200 family covers tube outer diameters used in semiconductor gas distribution, pharmaceutical process lines and aerospace hydraulics. Air-cooled and water-cooled head variants share the same programmable power source.

Talk to an engineer
Orbital Welding Systems
02 Where it's used
Semiconductor ultra-high-purity (UHP) gas systems
Pharmaceutical & biotech process tubing
Aerospace fluid & hydraulic systems
Instrumentation tubing for refineries & labs
04 Applications in depth

Where these machines earn their keep.

01

Semiconductor UHP gas distribution

Semiconductor fab gas lines (silane, ammonia, hydrogen) need contamination-free welds — any oxide on the ID can shed particles into the process. Closed-head orbital GTAW on the M200 power source meets the SEMI F70 / F78 specification.

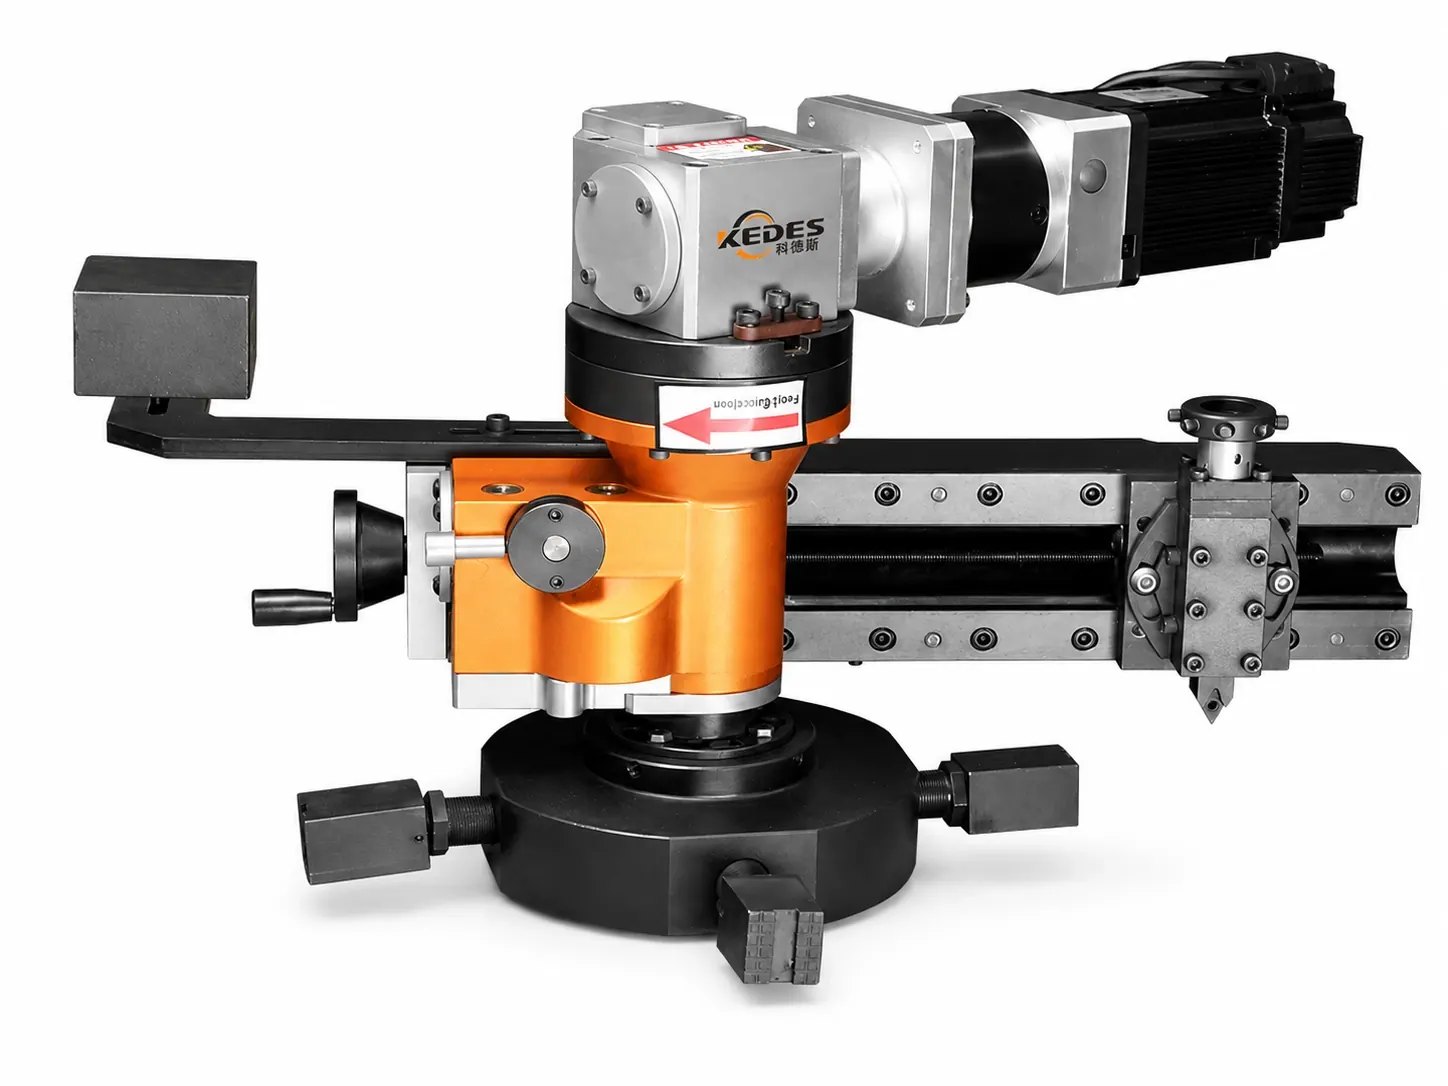
Orbital welding works only as well as the prep walking in. Pair the welder with a pipe facing machine — see orbital welding basics for the full prep-to-weld workflow.
02

Pharmaceutical and biotech process tubing

ASME BPE process tubing demands controlled finish, full CIP / SIP cleanability, and zero contamination from atmospheric oxygen at the weld. Closed-head orbital is the only process that holds all three reliably at production volume.

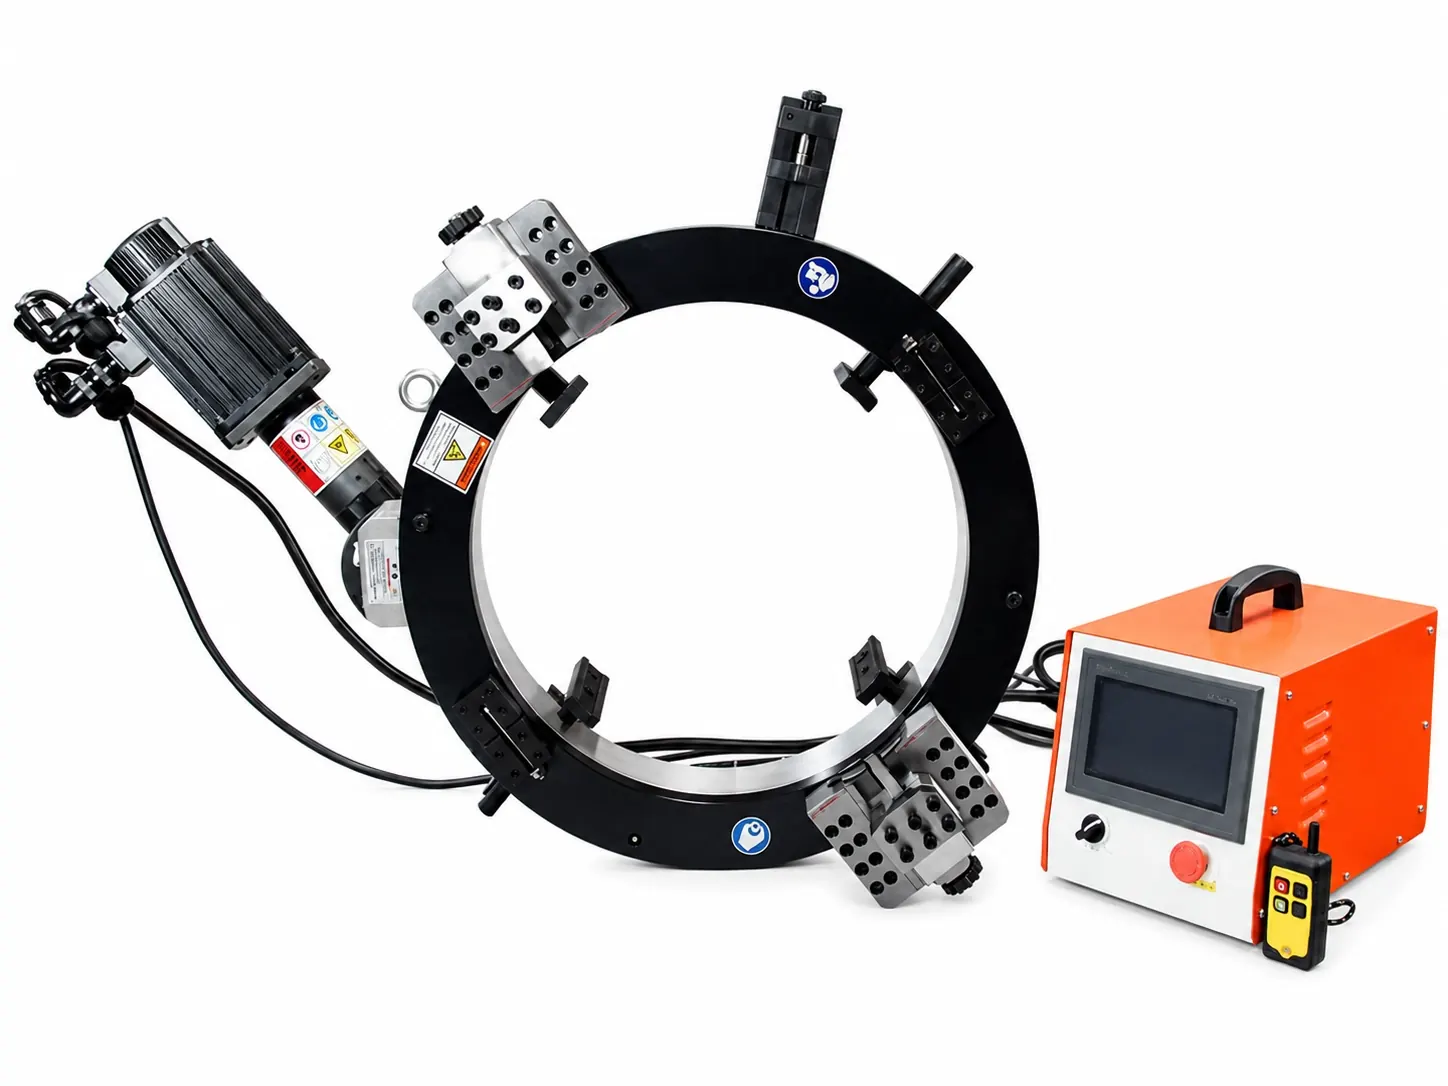
The bottleneck on these projects is rarely the welder — it is the prep machine. Bandsaw or abrasive cuts will not feed an orbital head. See choosing an orbital pipe cutter for the matching cutter selection.

03

Aerospace fluid and hydraulic systems

Aerospace hydraulics, fuel and oxygen lines run on small-OD tubing (typically 6 to 20 mm) at high inspection rate. Manual GTAW defect rate is too high for the volume — orbital makes the joint count economic.

The M200 air- and water-cooled heads cover the typical OD range. Bring the tube spec (OD, wall, material) to the quote form and we will match head and power source. For related stainless prep practice see beveling stainless without losing corrosion resistance.

04

Instrumentation tubing in refineries and labs

Instrumentation lines (impulse, sample, hydraulic control) run thousands of joints per project on small-bore tubing. Hand welding at the inspection rate required is uneconomic and the welder talent pool is shrinking.

The same closed-head orbital workflow scales down to the instrumentation OD range. Pair with a pipe facing machine for the squareness and the same M200 power source for the welds.

05 Frequently asked

Quick answers.

What sizes does the M200 cover?
The M200 family covers small-bore tubing typical of semiconductor and pharmaceutical applications. Air-cooled heads handle the lighter-duty range; water-cooled heads handle continuous-duty production. Send the tubing spec (OD, wall, material, weld program target) with the inquiry for exact head selection.
Closed-head vs open-head orbital — which do I need?
Closed-head for tubing where ID contamination is unacceptable — semiconductor UHP gas, ASME BPE sanitary, aerospace fluid systems. The head fully encloses the joint in argon. Open-head for larger process piping (above ~75 mm OD) where the absolute contamination requirement is lower. Full process detail in orbital welding basics.
How square does the tube end have to be before welding?
≤ 0.05 mm perpendicularity for closed-head welding on BPE / semiconductor work; ± 0.2 mm acceptable for open-head. A bandsaw cut delivers ± 0.5 mm — not square enough. The prep machine matters as much as the welder. Pair with a calibrated tube facing machine.
Do you supply the upstream cut and face machines as a matched set?
Yes. The standard high-purity workflow is cold cut → tube face → orbital weld, and we quote the package together. See choosing an orbital pipe cutter for the cutter selection and the pipe facing machines category for the matched facers.
What welding standards are the programs qualified to?
The program library targets ASME BPE, SEMI F70 / F78, AWS D18.2 (weld discolouration), and aerospace standards as required. Programs are qualified per OD / wall / material combination at install — generic library defaults are a starting point, not the final qualified program.
How long does it take to qualify a new tube spec?
Half a shift to a day depending on complexity. We supply program libraries with the head and walk through qualification on the specific OD / wall / material at install. After that, the same program holds quality joint after joint with no operator-dependence.
Next step

Get a quote within 24 hours.

Send us your spec sheet, pipe schedule, or drawing — our engineers reply with pricing, lead time, and recommended models.

  1. 01Send specs & drawings
  2. 02Receive quote within 24h
  3. 03Confirm & manufacture
Chat on WhatsApp
Chat on WhatsApp
Get a quote

Request a quotation.

Tell us pipe diameter, wall, material and country. We reply within one working shift.

WE REPLY WITHIN ONE WORKING SHIFT · GMT+8