
If You’re V-Grooving Everything, You’re Wasting Money
I get this inquiry every week: “Can your machine do a 37.5° V-groove?”
My answer is always: “Yes. But are you sure V-groove is the right choice for this wall thickness?”
Nine times out of ten, engineers pause. Because they’ve never calculated the cost. They learned “37.5° bevel” from their mentor, and that’s what they’ve always done.
Here’s the reality: On modern thick-wall piping, sticking to a standard V-groove is like driving a car with the parking brake on. It works, but it’s burning unnecessary fuel—or in your case, expensive filler metal and welder man-hours.
This guide will break down the four specific bevel types for pipe, and exactly when to switch to save costs.
The 4 Essential Pipe Bevel Types (2026)
Forget about plate terminology. In the piping world, where you usually only have access to the outside of the pipe (single-sided welding), these are the only four profiles that matter:
| Bevel Type | Shape | Best For Wall Thickness | Why Use It? (The ROI) |
|---|---|---|---|
| Standard V (Plain Bevel) | / (30° or 37.5°) | < 20mm (0.75”) | The Standard. Cheapest to machine and easiest to fit up. For thin-to-medium wall pipes, this is still your best bet. |
| Compound Bevel | // (37.5° + 10°) | > 20mm | The “Open Top”. Keeps the root open for good penetration but narrows the cap angle to reduce total weld volume. A great middle-ground upgrade from standard V. |
| J-Prep (U-Groove) | J (Radius) | > 25mm (1”) | The Money Saver. By keeping a consistent narrow gap all the way up, J-prep reduces filler metal consumption by 30-50% on heavy wall pipes. |
| Counterbore | /_ (ID Taper) | Any (Transition) | The Alignment Fixer. Machines the pipe ID to match mating pipe, eliminating Hi-Lo mismatch that causes failed X-rays. |
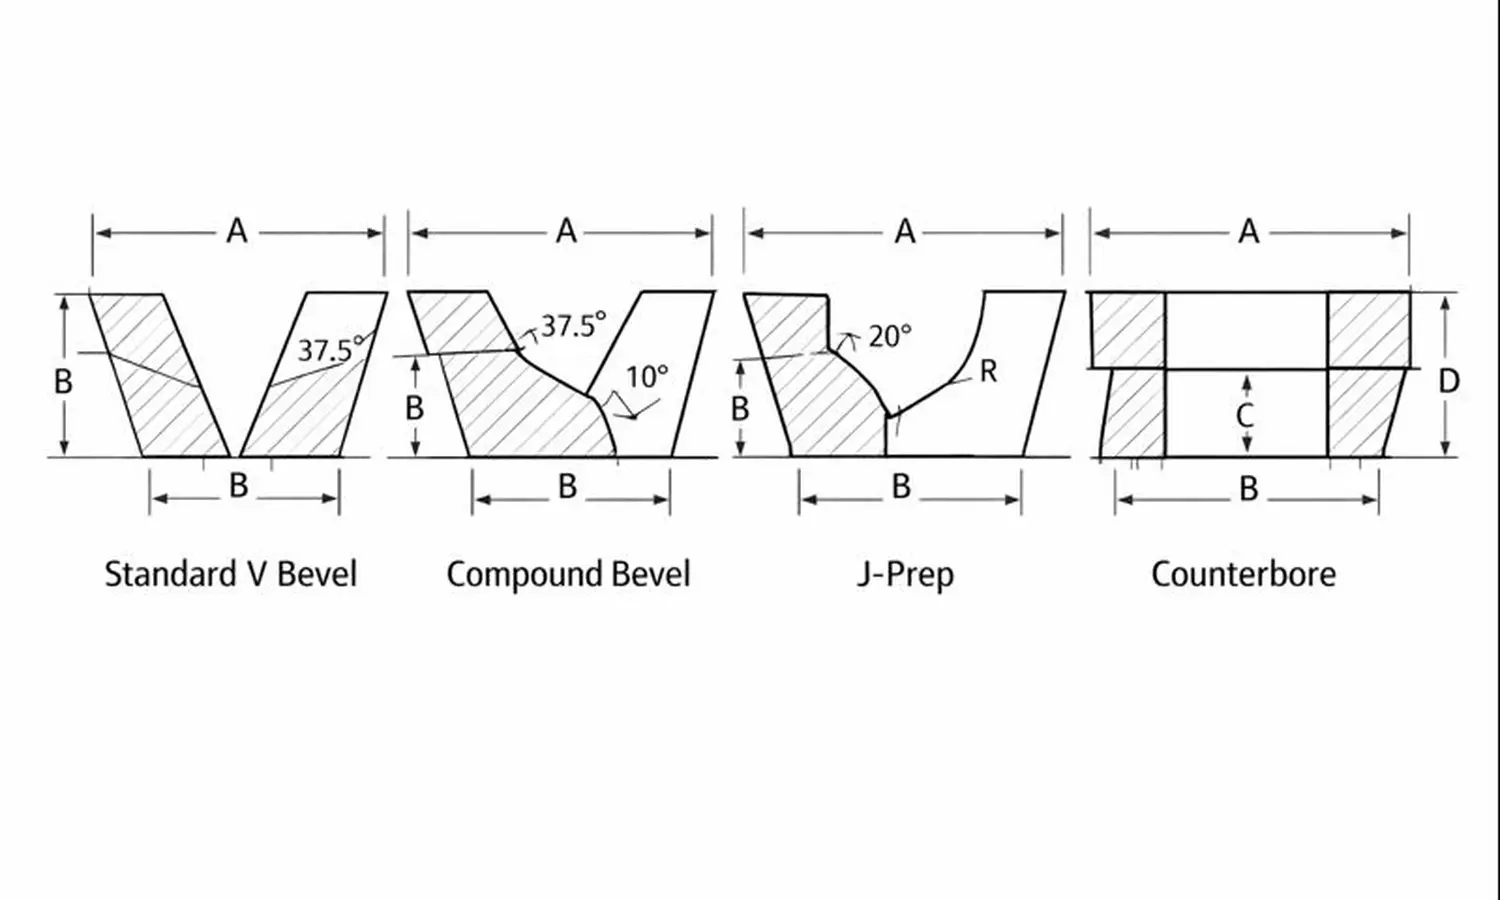 The four main pipe bevel types: Standard V-groove, Compound Bevel, J-Prep, and Counterbore
The “Hidden” Cost of V-Groove: The Volume Problem
Many people think bevel type is just about “shape.” It’s actually about Volume.
When pipe wall thickness exceeds 20mm, the volume of a standard 37.5° V-groove expands exponentially. You are essentially creating a massive triangular void that your welder has to fill, pass after pass.
- V-Groove: Wide top opening = Huge amount of filler metal
- J-Prep: Parallel or near-parallel side walls = Consistent, minimal filler metal
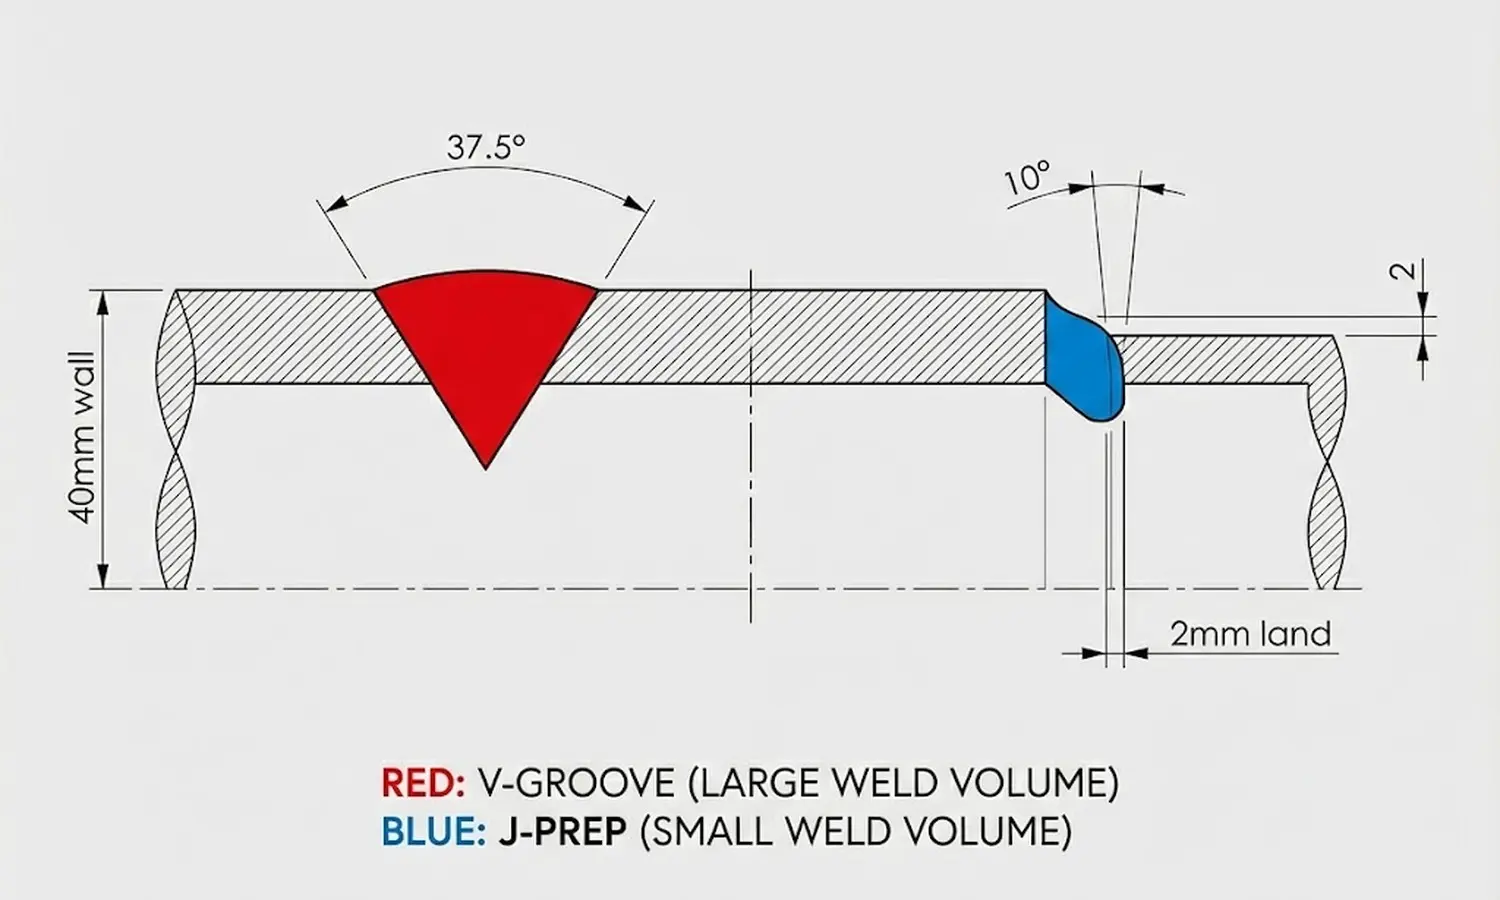 Same 40mm wall pipe: V-groove (left) requires nearly double the filler metal of J-prep (right)
The Rule of Thumb: If you are welding heavy wall pipes (Schedule 80, 160, or XXS), switching from V to J-prep isn’t just a technical tweak—it’s a financial rescue. I’ve written a full breakdown of J-bevel dimensions, angles and when the switch pays off if you want the exact numbers.
My experience: If your project has more than 100 meters of thick-wall pipe welding, the filler metal savings from switching to J-prep alone will pay for an ISE-II series beveling machine.
The “Missing” Link: Why Counterboring is Critical
Most beveling guides ignore this, but any field piper knows the pain of Hi-Lo (Internal Misalignment).
Seamless pipes are never perfectly round, and wall thickness often varies. When you fit two pipes together, the outer diameters might match, but the inner diameters (ID) often don’t. This creates a “step” or “ledge” inside the pipe.
The Result: Turbulent flow, corrosion points, and failed X-ray tests.
The Solution: Counterboring.
Using an ID-mounted machine (like our ISE Series) allows you to machine the inside of the pipe wall to a perfect circle, matching the ID of the mating pipe. This ensures a seamless transition and a perfect root pass every time.
My advice: Never rely on grinding to fix ID mismatch—it’s inaccurate and slow. If you’re working on critical piping systems (nuclear, petrochemical, subsea), counterboring capability is non-negotiable.
Cold Cutting vs. Thermal: It’s About More Than Just Geometry
Geometry saves you money, but Process saves you rework.
If you are working with high-performance materials like P91, Stainless Steel, or Duplex, using a torch or plasma cutter creates a Heat Affected Zone (HAZ). This “burnt” layer changes the metallurgy of the pipe end and must be ground off manually before welding.
Cold Cutting (Milling)—which is what our beveling machines do—cuts the metal without generating heat.
| Cold Cutting Advantage | What It Means For You |
|---|---|
| No HAZ | Material properties remain unchanged. No metallurgical rejection. |
| No Grinding | Surface is machine-finish and weld-ready immediately. Save 2+ hours per joint. |
| Safety | No sparks. Work safely in oil & gas environments where hot work permits are restricted. |
My stance: If you’re still using thermal cutting on P91 or Duplex, you’re not just risking quality—you’re guaranteeing rework.
Equipment Selection Guide
Don’t buy a machine based on maximum diameter alone. Buy it based on the Joint Design you need.
For Thin Wall (< 20mm) & Standard V-Groove
Stick to lightweight, portable tools. They are fast, cost-effective, and get the job done.
→ ISE-T Series - Lightweight ID mount, perfect for standard V on medium pipes
For Heavy Wall (> 25mm) & J-Prep/Compound
You need rigidity. Heavy-duty machines are built to handle the torque required for cutting J-preps and compound bevels without vibration.
→ ISE-II Series - Heavy-duty design, supports J-prep tooling, handles up to 75mm wall
For Critical Alignment (Hi-Lo Issues)
Ensure your machine is equipped with Counterboring Attachment.
→ ISC Block Type - Internal mount with counterbore capability for perfect ID matching
For Large Diameter & Field Work
When pipes are too big for ID-mount machines, or you need maximum portability:
→ Split Frame Series - OD clamping, handles 3/4”-48” pipes, ideal for field work
| Your Situation | Recommended Equipment | Why |
|---|---|---|
| Thin wall (< 20mm), standard V | ISE-T Series | Lightweight, fast, cost-effective |
| Heavy wall (> 25mm), J-prep | ISE-II Series | Heavy-duty, supports J-prep tooling |
| ID mismatch / Hi-Lo issues | ISC Block Type | Counterbore capability |
| Large diameter field work | Split Frame Series | OD mount, portable, 3/4”-48” range |
Real Case: ROI in 3 Months
A petrochemical client was welding 40mm thick P91 steam pipes. They were using standard V-grooves and grinding the HAZ manually.
I asked one question: “Have you calculated your total cost per joint?”
They went back and ran the numbers—and were shocked.
We helped them switch to a Cold Cutting J-Prep process.
| Metric | V-Groove + Thermal | J-Prep + Cold Cut | Savings |
|---|---|---|---|
| Filler per meter | 4.2 kg | 2.7 kg | 35% |
| Manual grinding | 2 hours/joint | 0 hours | 100% |
| Number of passes | 18 | 11 | 39% |
| Welding time per meter | 4.5 hours | 3.2 hours | 29% |
The savings on P91 filler wire alone paid for their new beveling machine fleet in the first quarter.
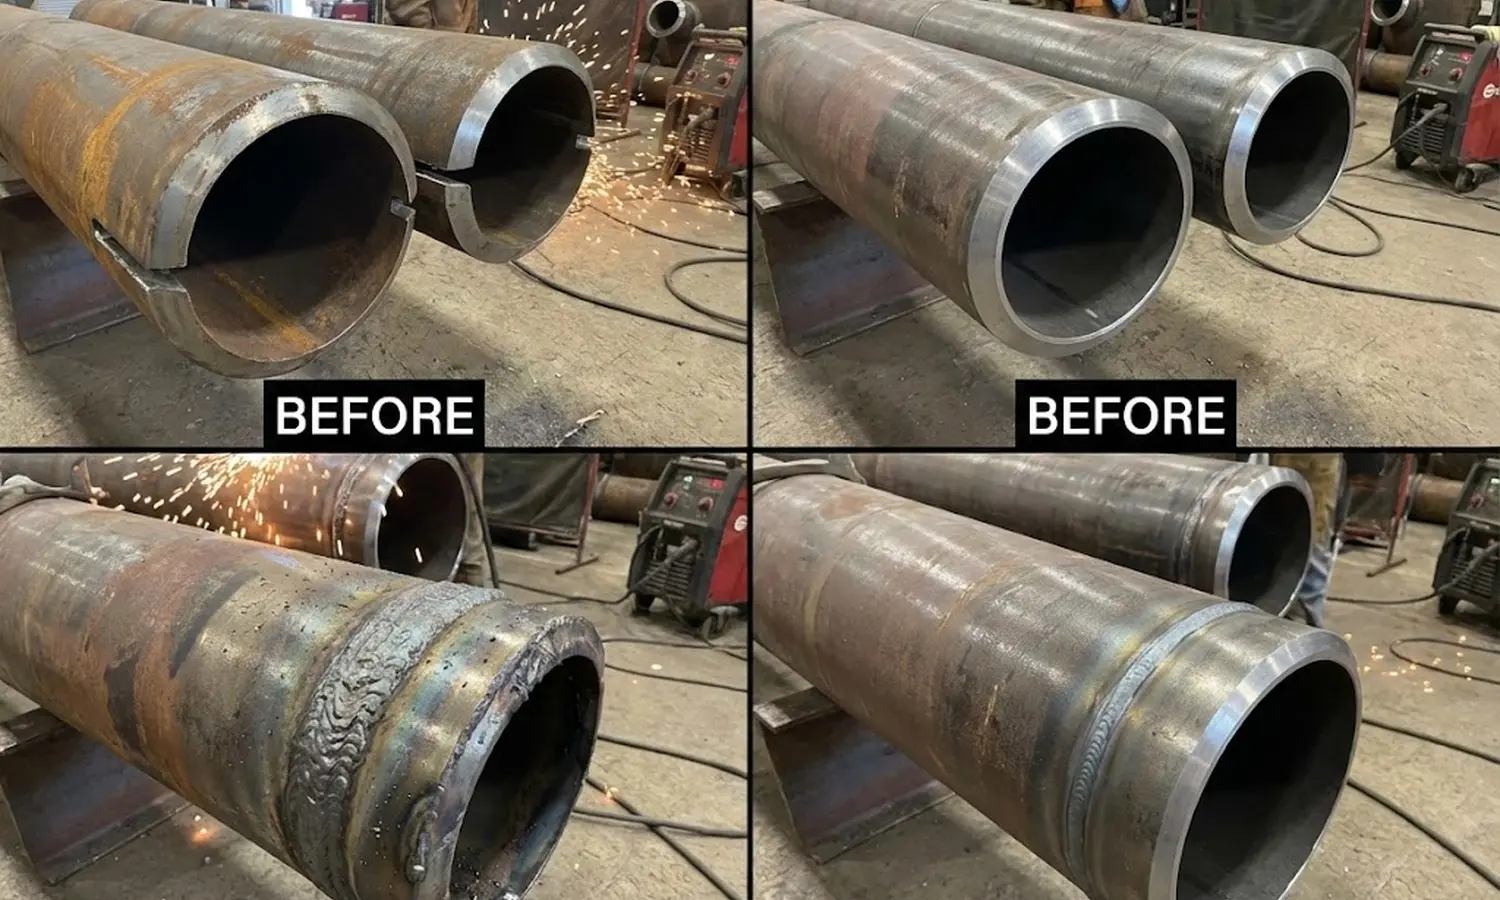 Left: V-groove before; Right: J-prep after
Summary: Stop Guessing, Start Calculating
- < 20mm Wall: V-Groove is fine. Don’t overthink it.
- > 20mm Wall: J-Prep or Compound Bevel is mandatory for cost control.
- High-Spec Material (P91, Duplex, SS): Cold cutting is non-negotiable to avoid HAZ.
- Mismatched ID: Always Counterbore. Never grind.
Still Not Sure Which Bevel Type Fits Your WPS?
Send me:
- Pipe diameter and wall thickness
- Material grade
- Welding process (if known)
I’ll run a free “Weld Volume Savings Calculation” to show you exactly how much money switching to J-prep could save you on your next project.
→ Browse All Pipe Beveling Machines → Plate Edge Milling Guide (Related Reading) → Pipe Bevel Angles & Code Requirements (Related Reading)