
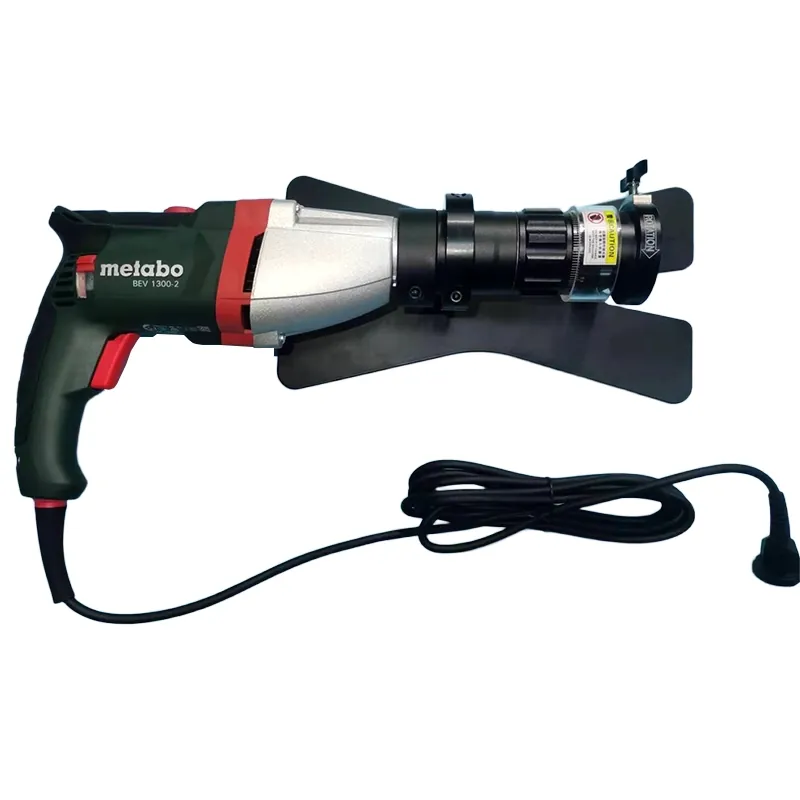
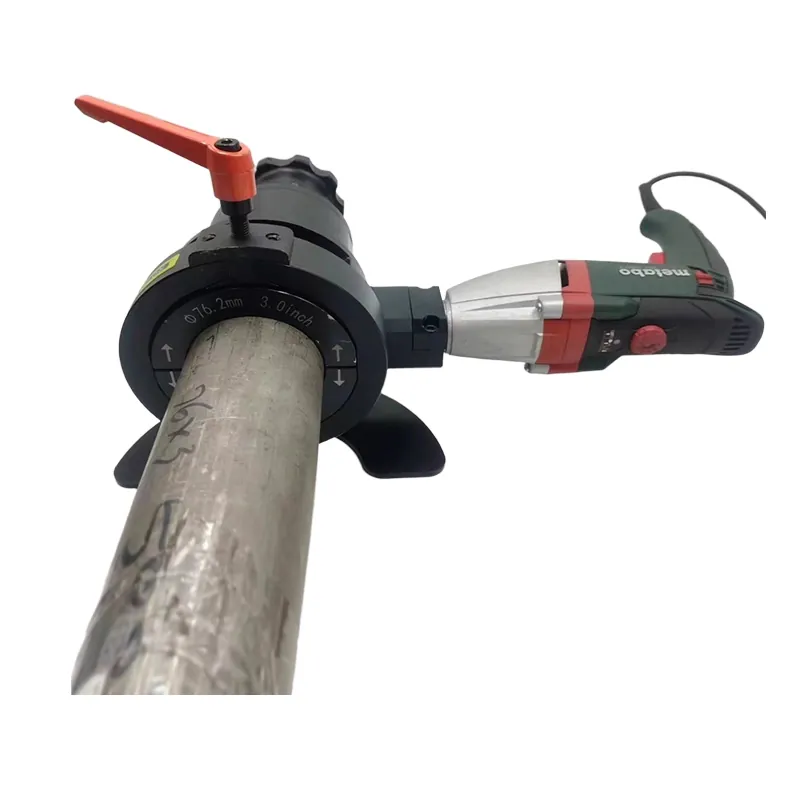
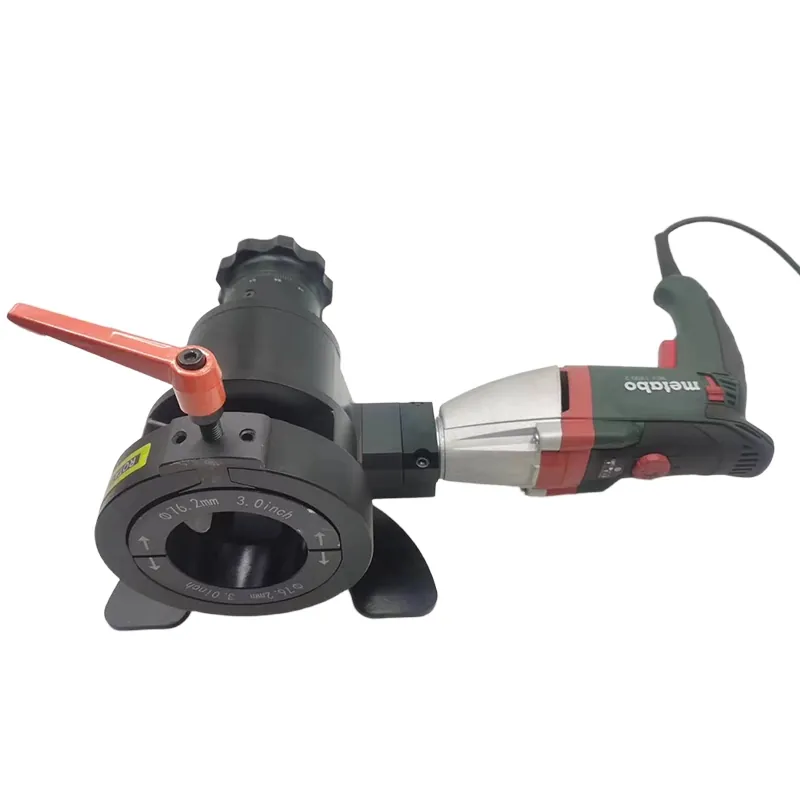
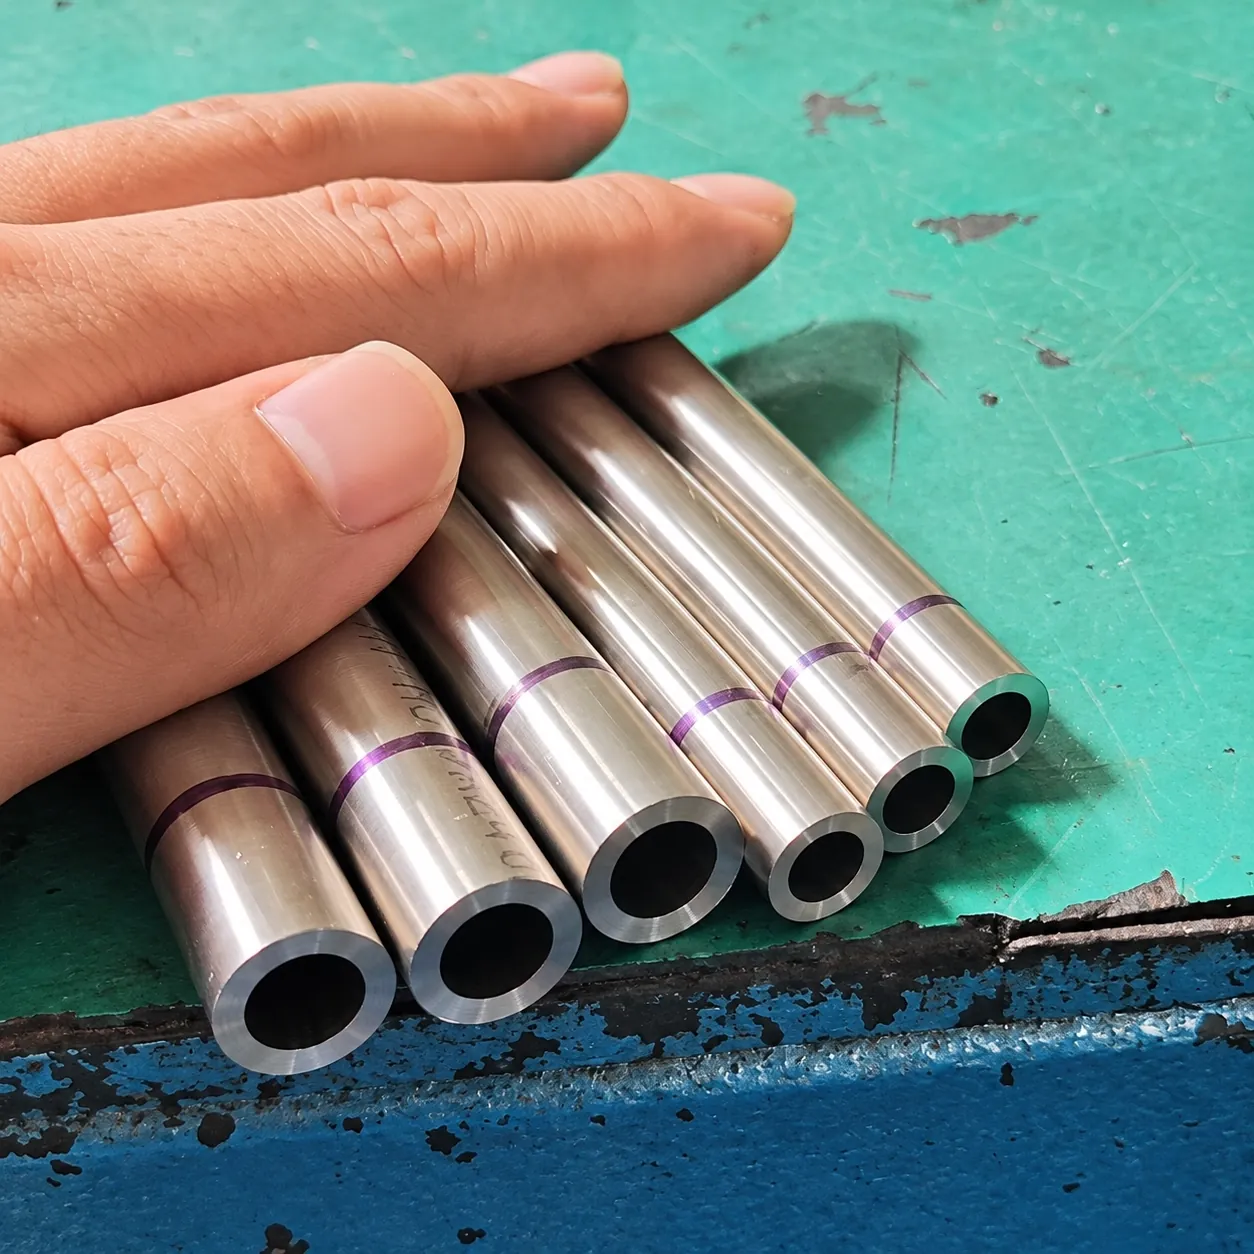
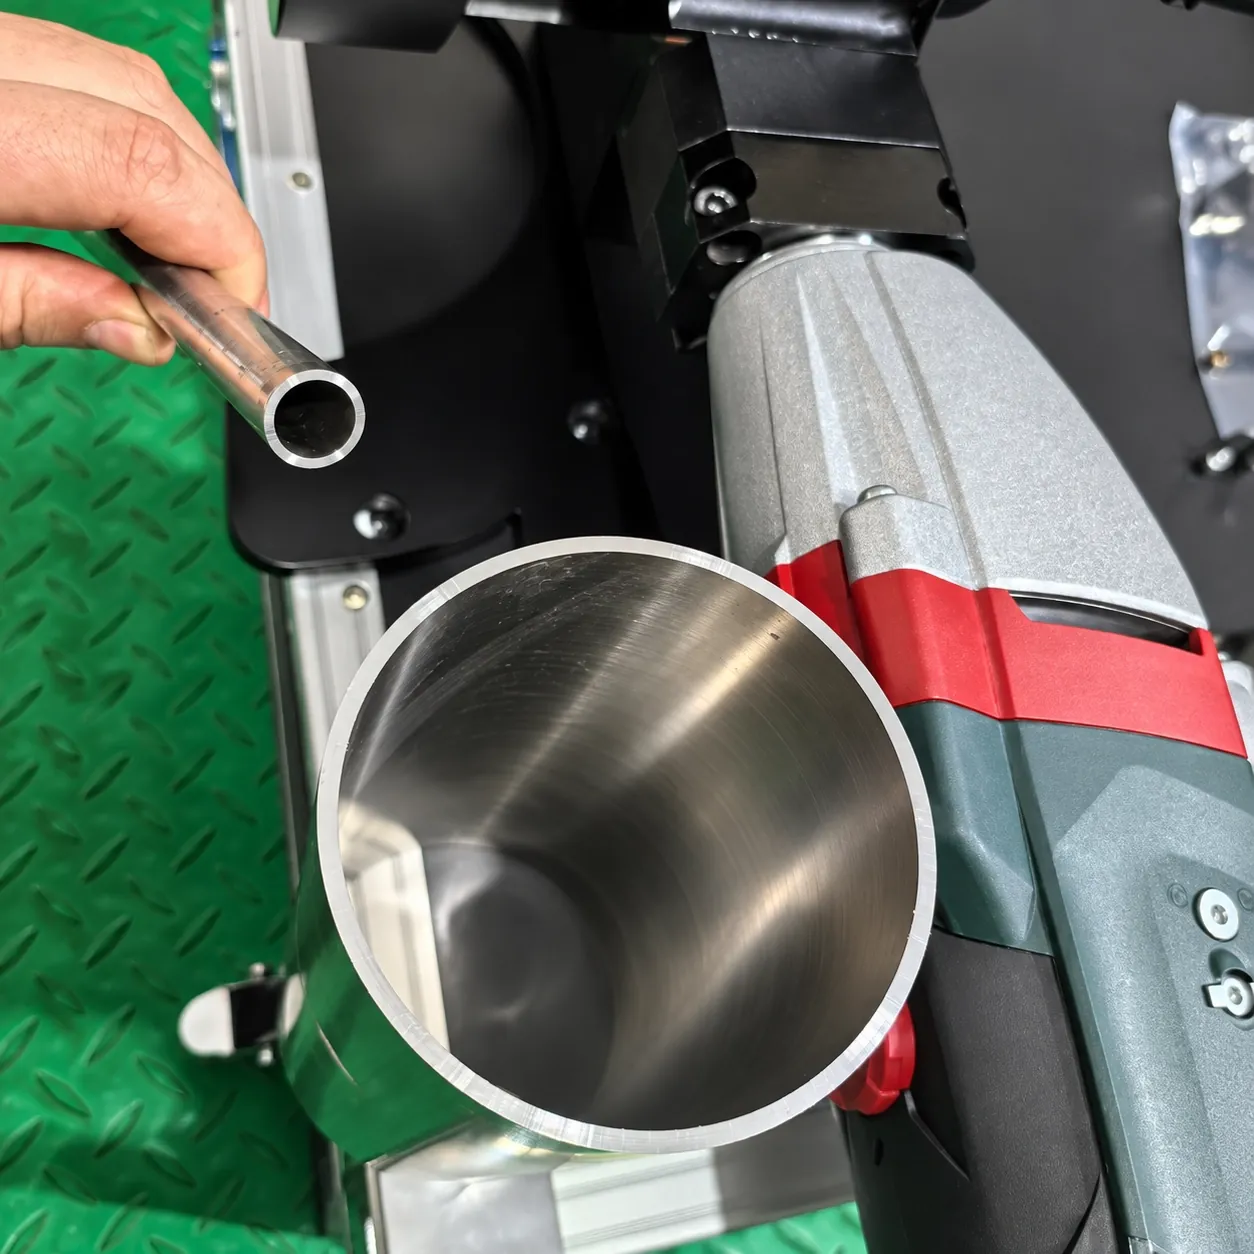
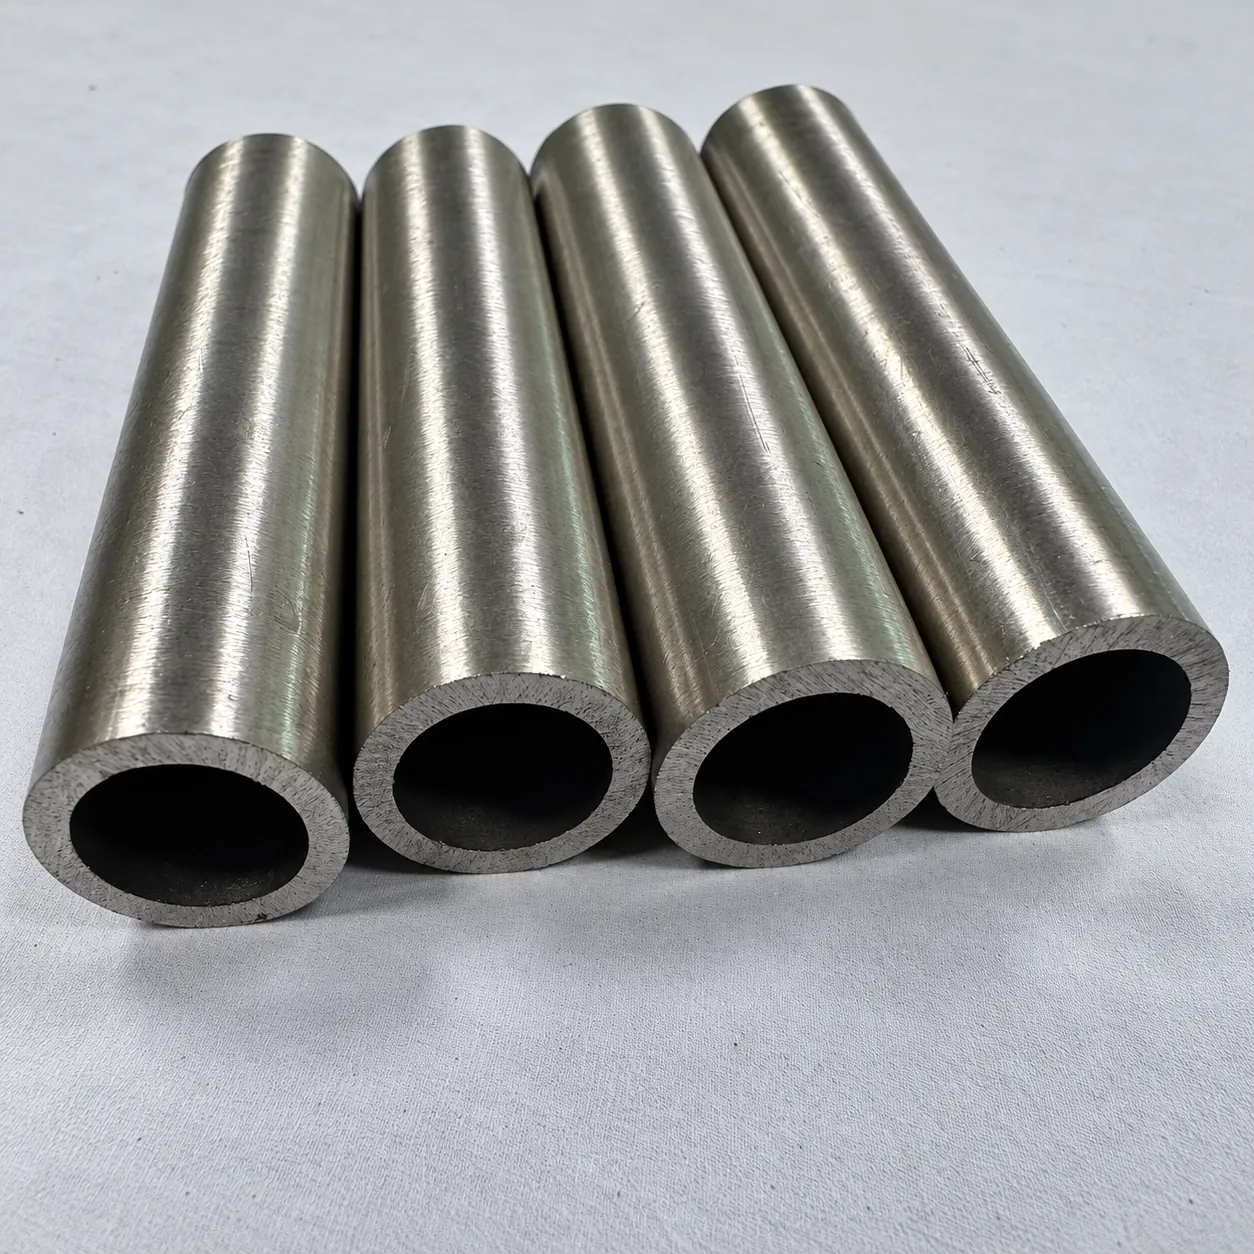
LPM Electric Tube Facing Machine (AC, High-Torque)
1300 W Metabo-driven benchtop tube facer for sustained production. Constant torque indefinitely, planetary gear reduction on larger models for low-RPM finish on thick-wall sanitary tube. Faces tube Ø 3.17 – 114.3 mm with wall up to 5 mm — the production-shop standard for high-purity tube fabrication.
Pick your size — 5 models in the series.
| LPM-1.0 AC Ø 3.17 – 25.4 mm · 10 kg | LPM-1.5 AC Ø 6 – 38.1 mm · 11 kg | LPM-2.5 AC Ø 9 – 63.5 mm · 13 kg | LPM-3.5 AC Ø 12.7 – 88.9 mm · 35 kg · geared | LPM-4.5 AC Ø 19 – 114.3 mm · 45 kg · geared | |
|---|---|---|---|---|---|
| Tube OD range | 3.17 – 25.4 mm | 6 – 38.1 mm | 9 – 63.5 mm | 12.7 – 88.9 mm | 19 – 114.3 mm |
| Wall thickness | 0.5 – 5 mm | 0.5 – 5 mm | 0.5 – 5 mm | 0.5 – 5 mm | 0.5 – 5 mm |
| Cutter speed | 420 r/min | 420 r/min | 420 r/min | 150 r/min (geared) | 150 r/min (geared) |
| Motor power | 1300 W | 1300 W | 1300 W | 1300 W | 1300 W |
| Net weight | 10 kg | 11 kg | 13 kg | 35 kg | 45 kg |
| Standard collets supplied | 6.35 / 9.52 / 12.7 / 19.05 / 25.4 mm | 9.52 / 12.7 / 19.05 / 25.4 / 38.1 mm | 25.4 / 31.8 / 38.1 / 50.8 / 63.5 mm | 25.4 / 38.1 / 50.8 / 63.5 / 76.3 mm | On specification |
| Collet system | Full-contact SS | Full-contact SS | Full-contact SS | Full-contact SS | Full-contact SS |
| Quote this model |
Why planetary gear reduction matters on large-OD sanitary tube
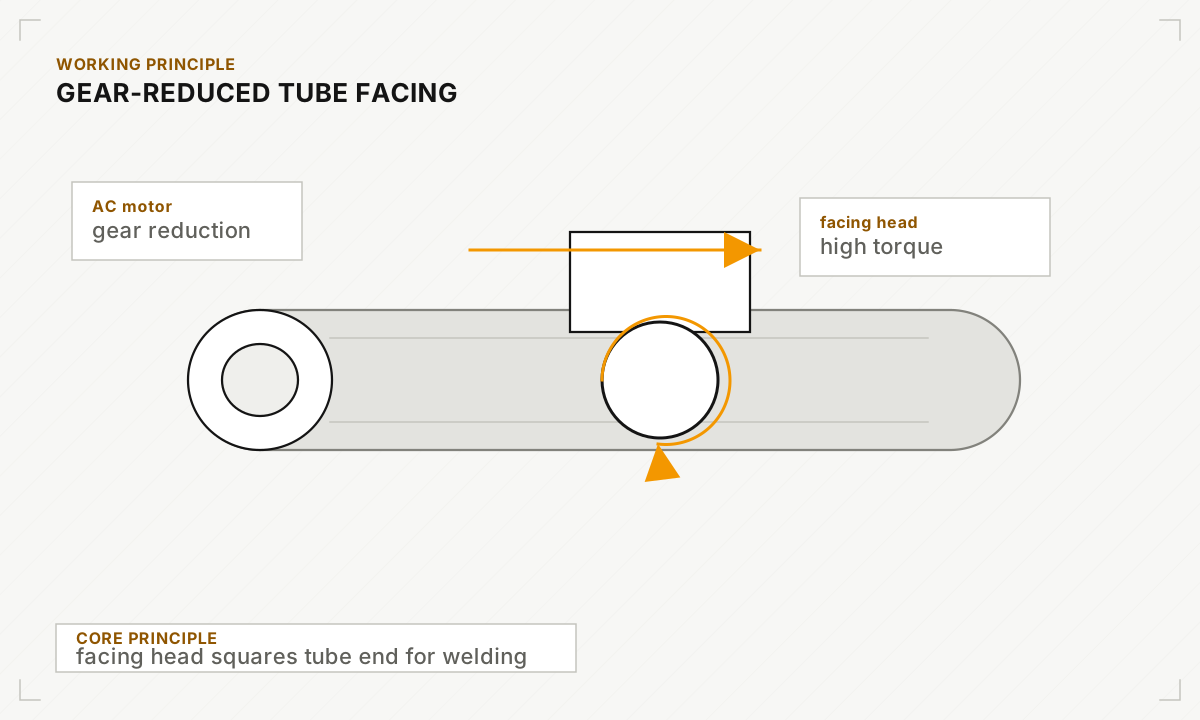
Cutter linear speed at the workpiece is RPM × π × diameter. On a small 1/4" tube at 420 RPM, the linear speed is moderate; on a 4.5" tube at the same RPM, linear speed quadruples — exceeding the carbide tooling's optimal Vc and causing premature insert wear and a poor surface finish. The LPM-3.5 AC and LPM-4.5 AC use planetary gear reduction to drop cutter speed to 150 RPM while preserving torque from the 1300 W Metabo motor. This puts the cutting interface back in the optimal Vc window for stainless and Cr-Mo work — sustaining insert life and producing the burr-free surface finish required for ASME BPE orbital welding.
Built for the job site.
Where this series earns its keep.
Pharmaceutical & bio-process tube fab
High-volume facing of stainless WFI, CIP and process tubing in batch production. Geared LPM-4.5 AC for larger 3" and 4" fermenter and storage-vessel piping.
Food, dairy & brewery production
Sanitary stainless tube prep for dairy CIP loops, brewery wort lines and food-grade process. Constant torque handles long fab runs typical of new-plant builds.
General stainless tube prefab
Industrial stainless tube prefab for chemical, gas-handling and general process piping where AC bench mounting is preferred over portable cordless operation.
Common questions about the LPM · AC Series.
Can't find your answer?
My tube size is not in the collet list — can the machine still face it?
AC or DC LPM — which should I order?
When do I need the geared LPM-3.5 or LPM-4.5 specifically?
Does it work on Cr-Mo and Inconel as well as stainless?
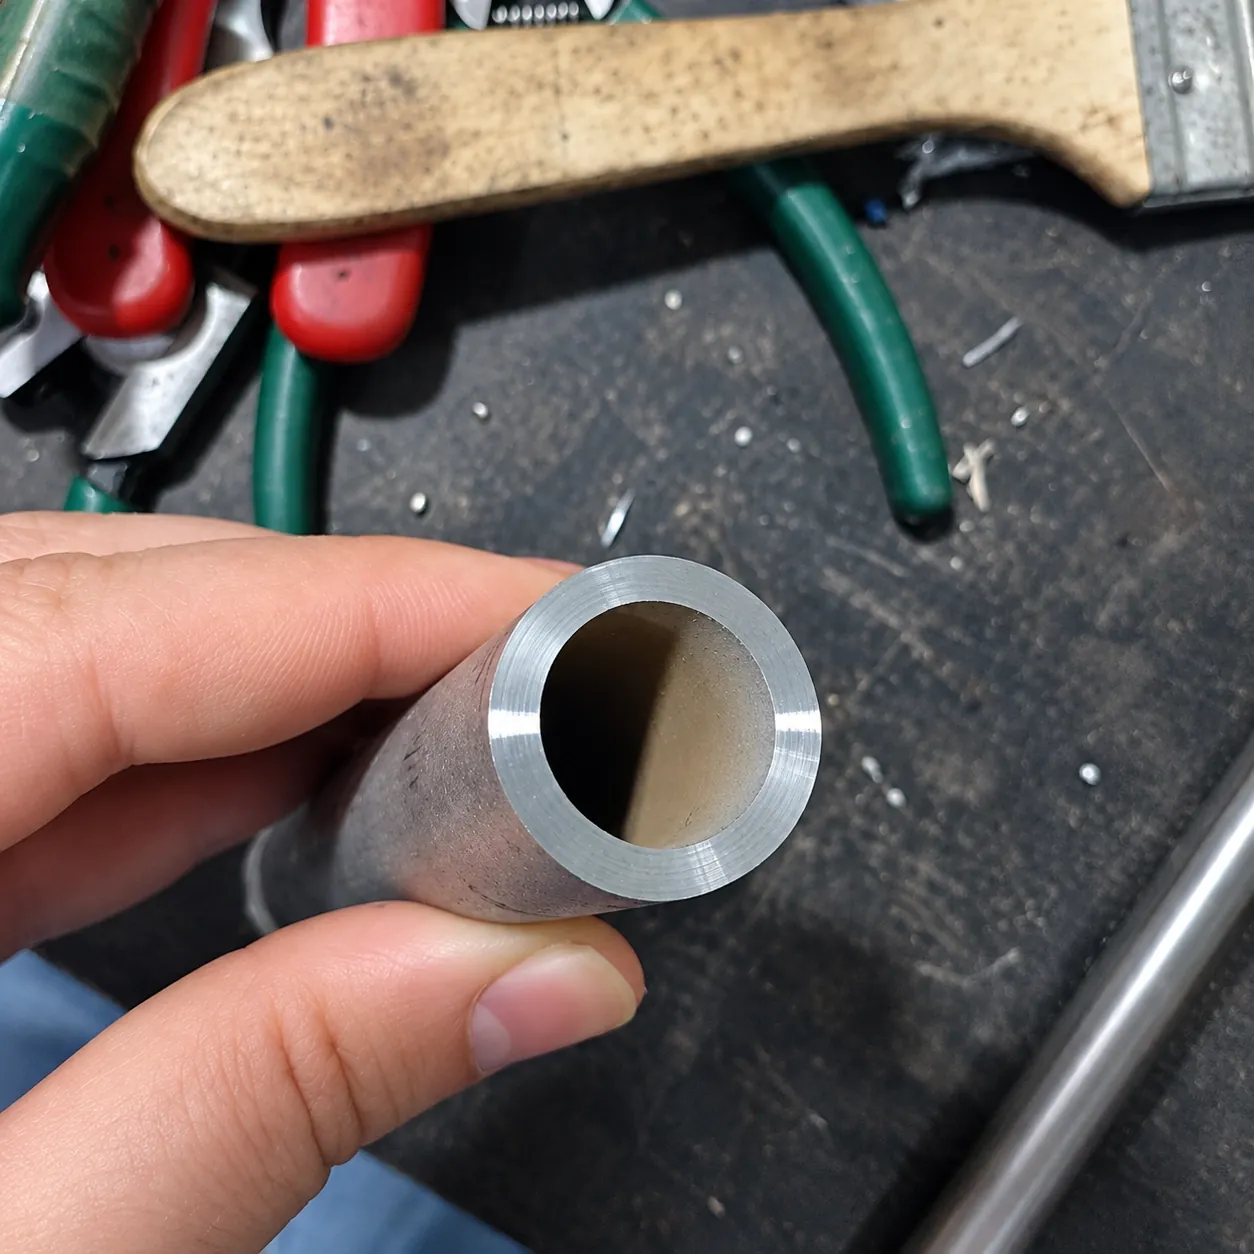
Is the face finish compatible with orbital welding fit-up?
Other pipe facing machines.
Get a quote within 24 hours.
Send us your spec sheet, pipe schedule, or drawing — our engineers reply with pricing, lead time, and recommended models.
- 01Send specs & drawings
- 02Receive quote within 24h
- 03Confirm & manufacture