
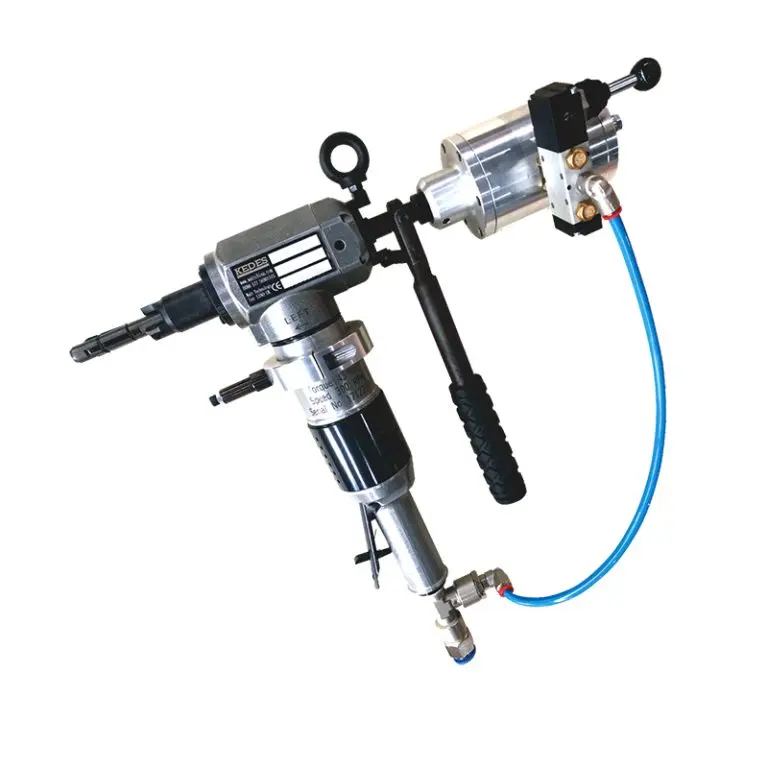
KD Pneumatic High-Speed Tube Squaring Machine
Compact ID-mounted tube squarer engineered for heat-exchanger and pressure- vessel manufacturing — where thousands of tube ends must be faced, chamfered and de-burred in a single shift. Pneumatic one-touch clamping, 59 mm head width fits into densely-packed tube sheets.
Pick your size — 4 models in the series.
| KD-24 Ø 12.4 – 28 mm · manual feed | KD-24A Ø 12.4 – 28 mm · auto feed | KD-48 Ø 20 – 48 mm · manual feed | KD-48A Ø 20 – 48 mm · auto feed | |
|---|---|---|---|---|
| Tube ID range | 12.4 – 28 mm | 12.4 – 28 mm | 20 – 48 mm | 20 – 48 mm |
| Feed method | Manual | Automatic | Manual | Automatic |
| No-load speed | 300 r/min | 300 r/min | 100 r/min | 100 r/min |
| Max torque | 43 Nm | 43 Nm | 110 Nm | 110 Nm |
| Air motor | 1.3 HP | 1.3 HP | 1.3 HP | 1.3 HP |
| Net weight | 7 kg | 8 kg | 8 kg | 13 kg |
| Head width | ≤ 59 mm | ≤ 59 mm | ≤ 59 mm | ≤ 59 mm |
| Quote this model |
Why pneumatic one-touch clamping matters on tube sheets
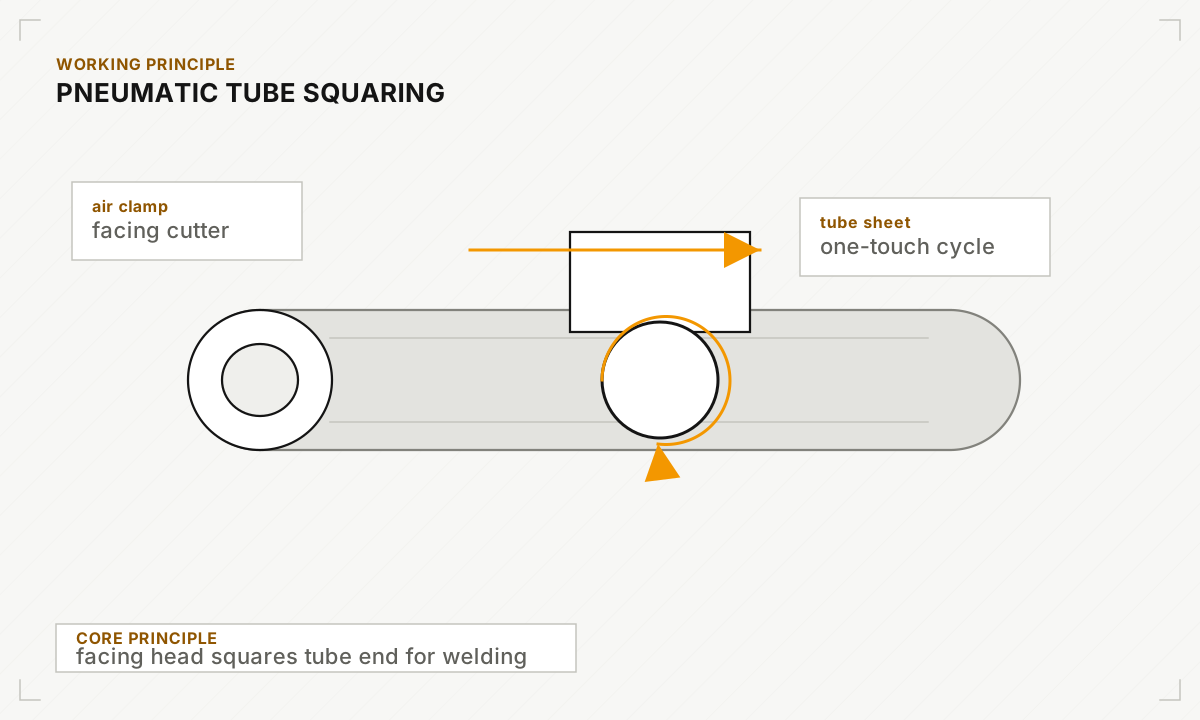
A typical shell-and-tube exchanger has several hundred to several thousand tube ends penetrating each tube sheet, spaced on a triangular or square pitch as tight as 1.25 × OD. Conventional thread-clamp tube facers take 20 – 40 seconds per tube to mount, square, and dismount; on a 2000-tube bundle that becomes 11 – 22 hours of setup time alone. The KD's one-touch pneumatic mandrel engages in under a second per tube — the same operation completed in 30 – 60 minutes. The narrow head (≤ 59 mm) accepts the tightest TEMA pitch without fouling adjacent tubes.
Built for the job site.
Where this series earns its keep.
Heat-exchanger tube-bundle manufacturing
New-build shell-and-tube exchanger fabrication — rapid squaring and chamfering of bundle tube ends to unified protrusion length. The single defining application.
Boiler & condenser re-tubing
In-service exchanger and condenser re-tubing during planned outages, where the narrow head accesses tube sheets that a chuck-type facer cannot reach.
Refinery exchanger maintenance
On-site re-tube and tube-end repair on refinery process exchangers and fired-heater coils during turnaround windows.
Common questions about the KD Series · Pneumatic.
Can't find your answer?
When is this faster than an LPM electric facer?
What air supply is needed?
Can it remove a previously welded tube end (re-tube application)?
Other pipe facing machines.
Get a quote within 24 hours.
Send us your spec sheet, pipe schedule, or drawing — our engineers reply with pricing, lead time, and recommended models.
- 01Send specs & drawings
- 02Receive quote within 24h
- 03Confirm & manufacture