
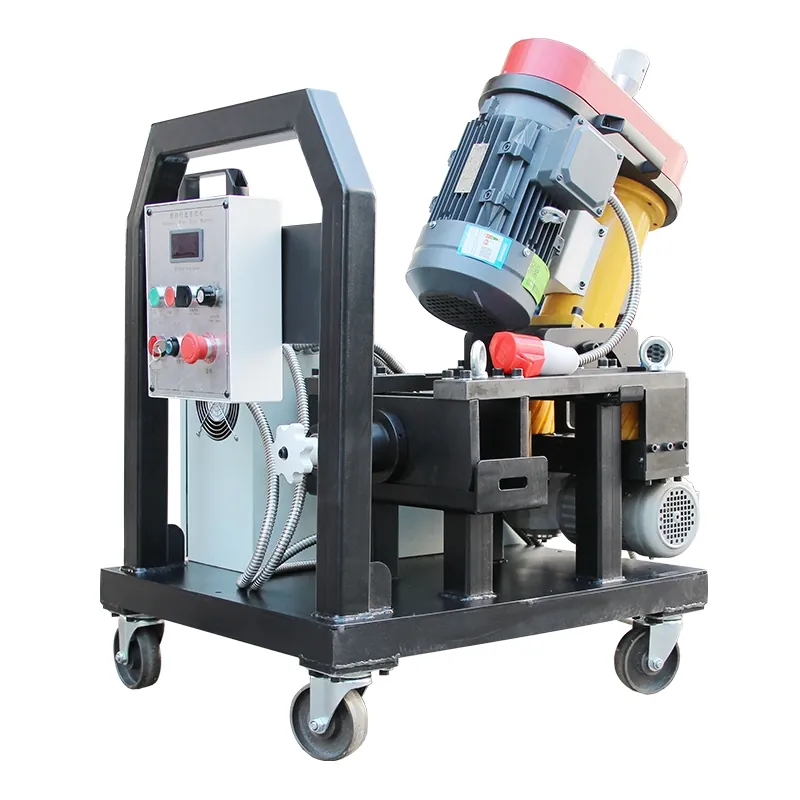
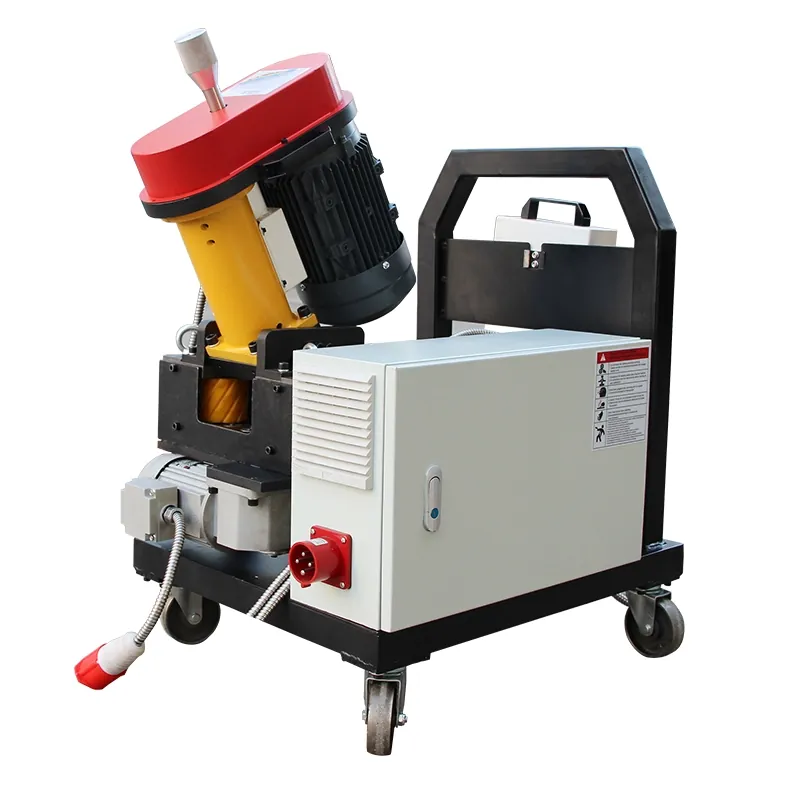
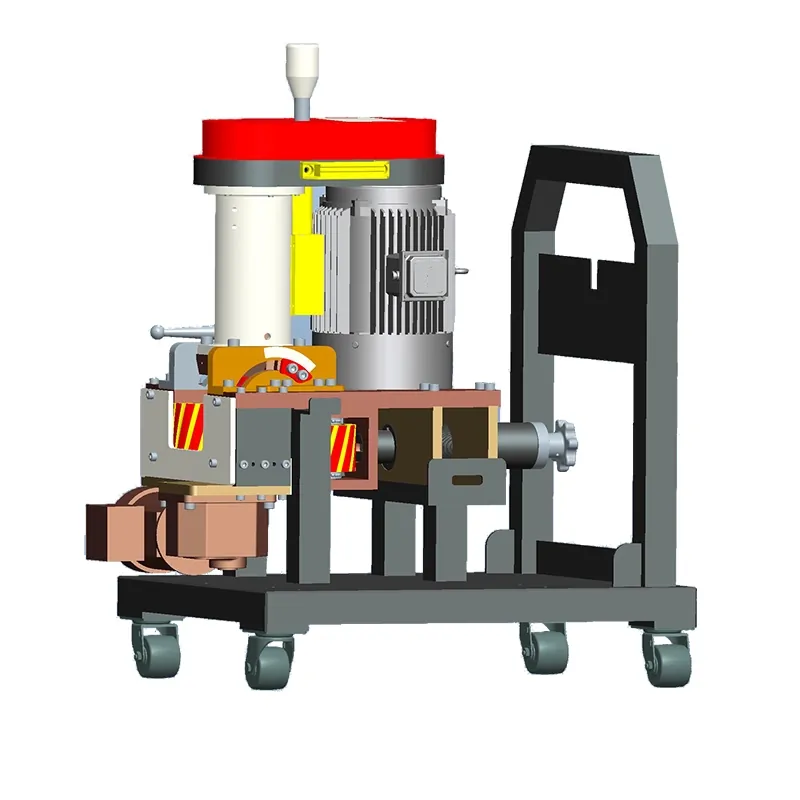
DMM-YG Large-Diameter Pipe & Vessel Edge Miller
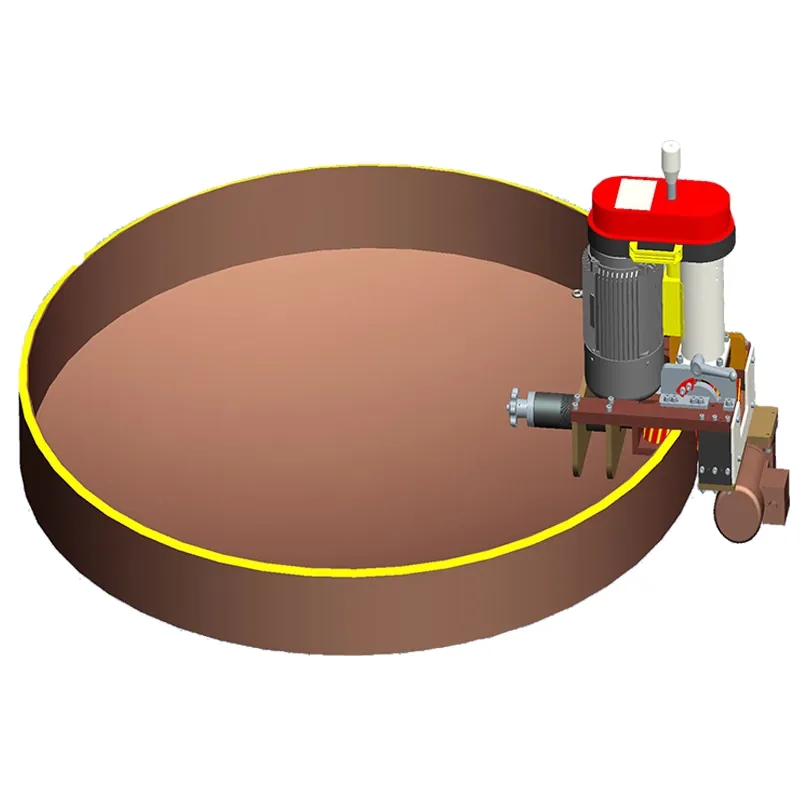
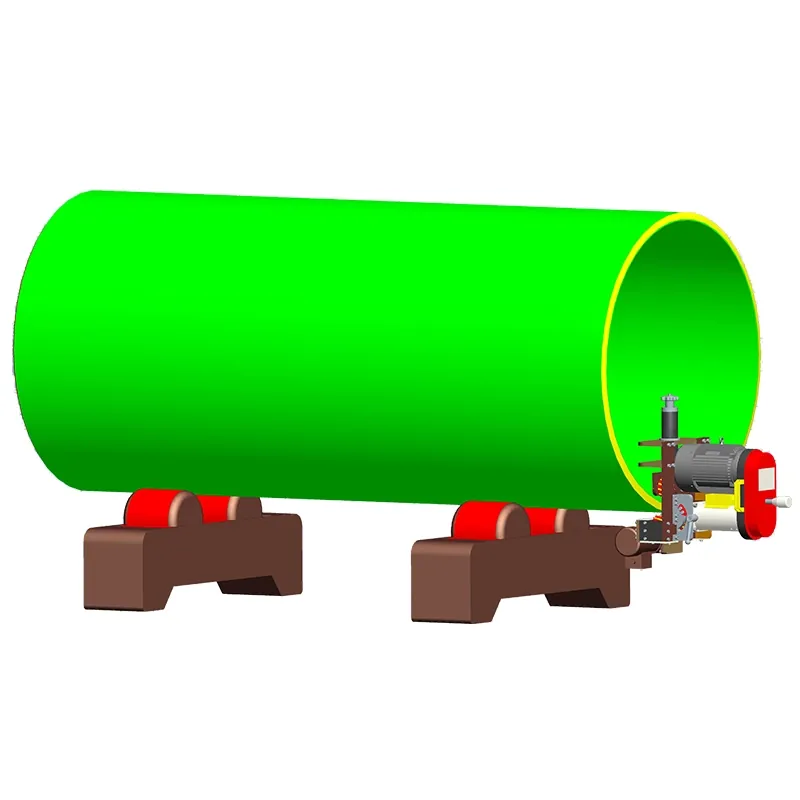
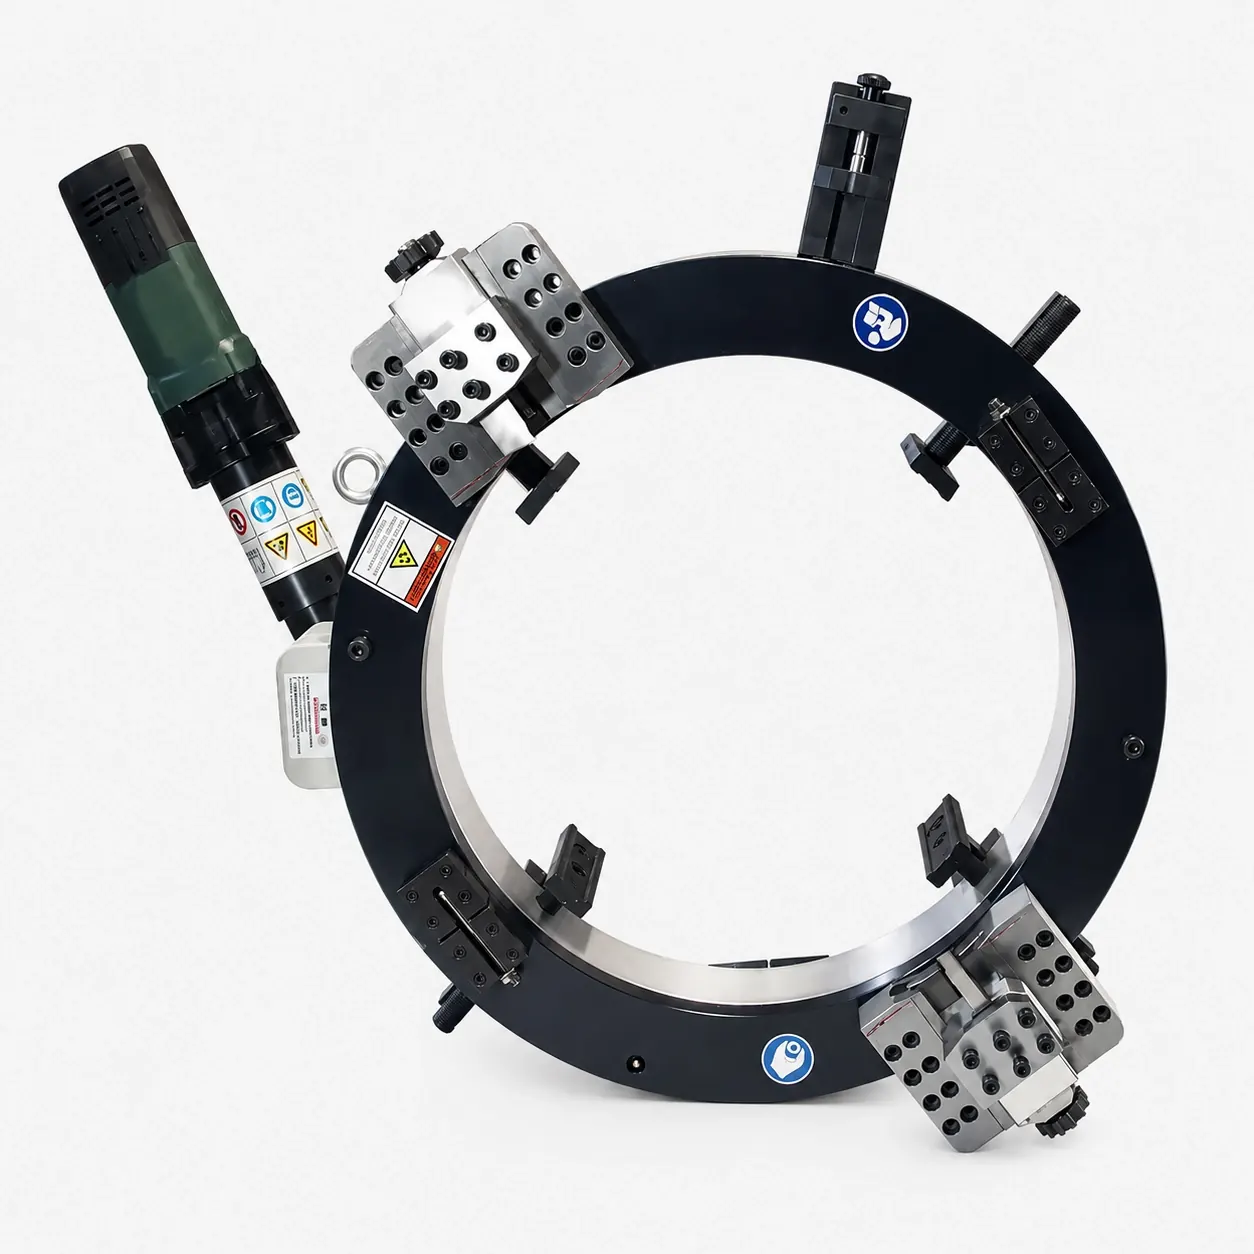
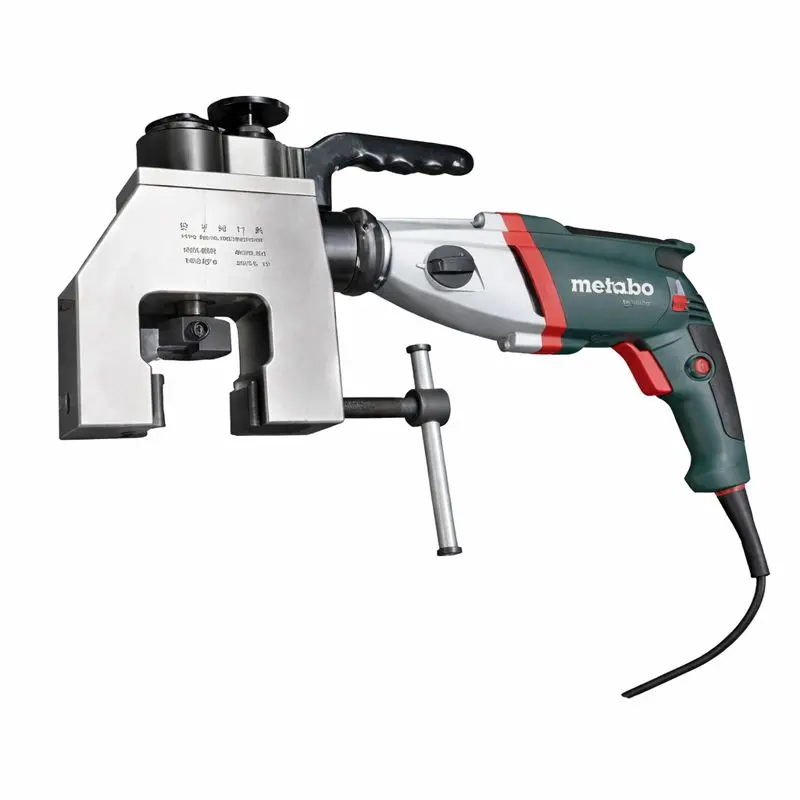
Self-propelled edge miller that travels around the circumference of large-diameter pipe and pressure-vessel shells (OD > 600 mm). Specialized clamping system tracks curved surfaces while the cutter prepares longitudinal or circumferential weld seams up to 100 mm wall. Cold milling, Ra 3.2 – 6.3 μm directly off the tool.
Pick your size — 2 models in the series.
| DMM-YG-60 Standard · Ø > 600 mm · wall ≤ 45 mm | DMM-YG-80 Heavy vessel · Ø > 800 mm · wall ≤ 100 mm | |
|---|---|---|
| Pipe / vessel OD | > 600 mm | > 800 mm |
| Wall thickness | 5 – 45 mm | 6 – 100 mm |
| Bevel angle range | 0° – 60° | 25° – 70° |
| Max bevel width | 30 mm | 65 mm |
| Motor power | 4000 W | 6000 W |
| Operation | Self-propelled circumferential | Self-propelled circumferential |
| Bevel direction | Inside + outside | Inside + outside |
| Net weight | 310 kg | 330 kg |
| Surface finish | Ra 3.2 – 6.3 μm | Ra 3.2 – 6.3 μm |
| Quote this model |
How a curved-surface tracking miller works
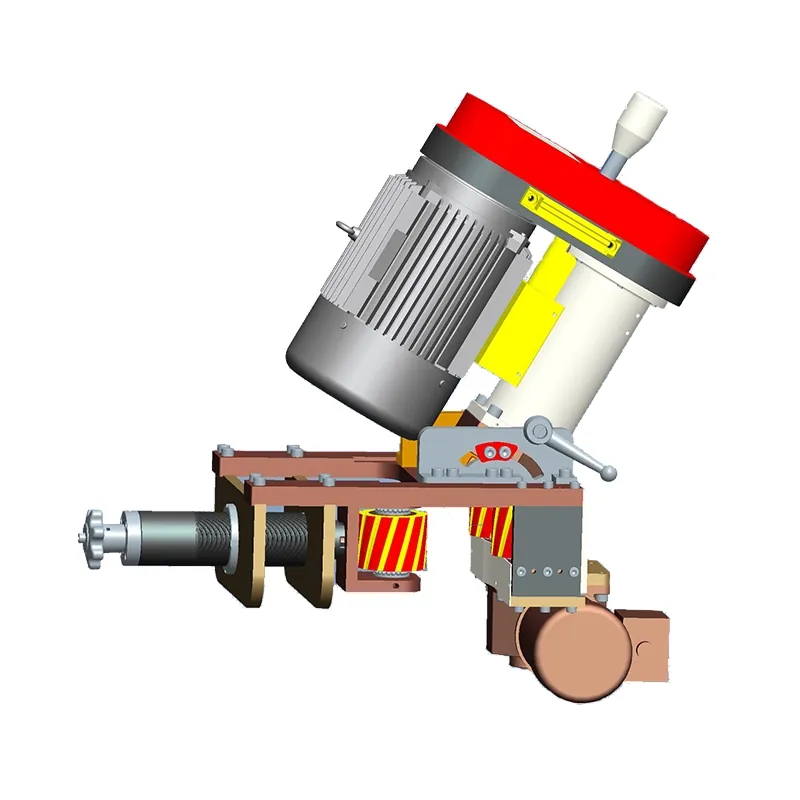
Large pressure vessels, storage tanks and wind-tower sections cannot be rotated like a workpiece on a lathe — they're too heavy to spin and typically supported on cradles or pads. The work must come to the cutter. The DMM-YG addresses this with a clamp-and-travel architecture: a magnetic or chain-and-pad clamping system grips the curved shell surface, and the cutter assembly walks itself around the circumference on a tracked carriage. The milling head pivots inward or outward to address either inside-bore or outside-OD bevels — required when the weld geometry calls for compound prep on heavy wall (typical of nuclear and HP-steam vessel construction). Cold milling on carbide inserts delivers production-machine surface quality on workpieces that cannot be moved.
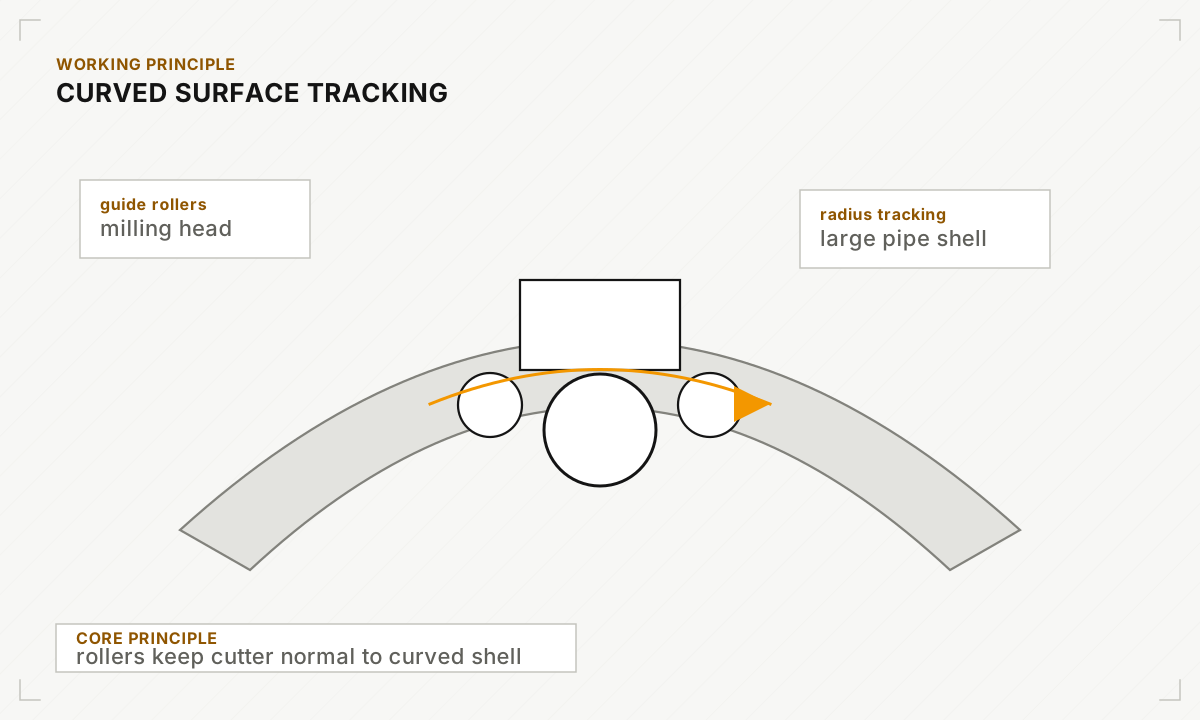
Built for the job site.
Where this series earns its keep.
Large-diameter pipeline & storage tank
Circumferential bevel prep on transmission-line pipe and storage-tank shell courses where wall exceeds the range of split-frame and chuck-type pipe bevelers. Standard tool for tank field-fab.
Pressure vessel, nuclear & wind-tower
Heavy-wall vessel-shell prep for nuclear, HP-steam and large pressure-vessel construction. Wind-tower section longitudinal-seam prep on Q345 / S355 structural plate.
Reactor & process-vessel shell fabrication
Reactor shell, hydrocracker and column vessel beveling — Cr-Mo and quenched-and-tempered grades where cold cutting is mandatory for code-compliant welds.
Common questions about the DMM-YG Series.
Can't find your answer?
How is this different from the split-frame clamshell beveler?
When do I need this over SKF-150L capless?
Inside-bore beveling — how does it work on a closed vessel?
Magnetic vs chain clamping — when to use which?
Other pipe beveling machines.
Get a quote within 24 hours.
Send us your spec sheet, pipe schedule, or drawing — our engineers reply with pricing, lead time, and recommended models.
- 01Send specs & drawings
- 02Receive quote within 24h
- 03Confirm & manufacture