
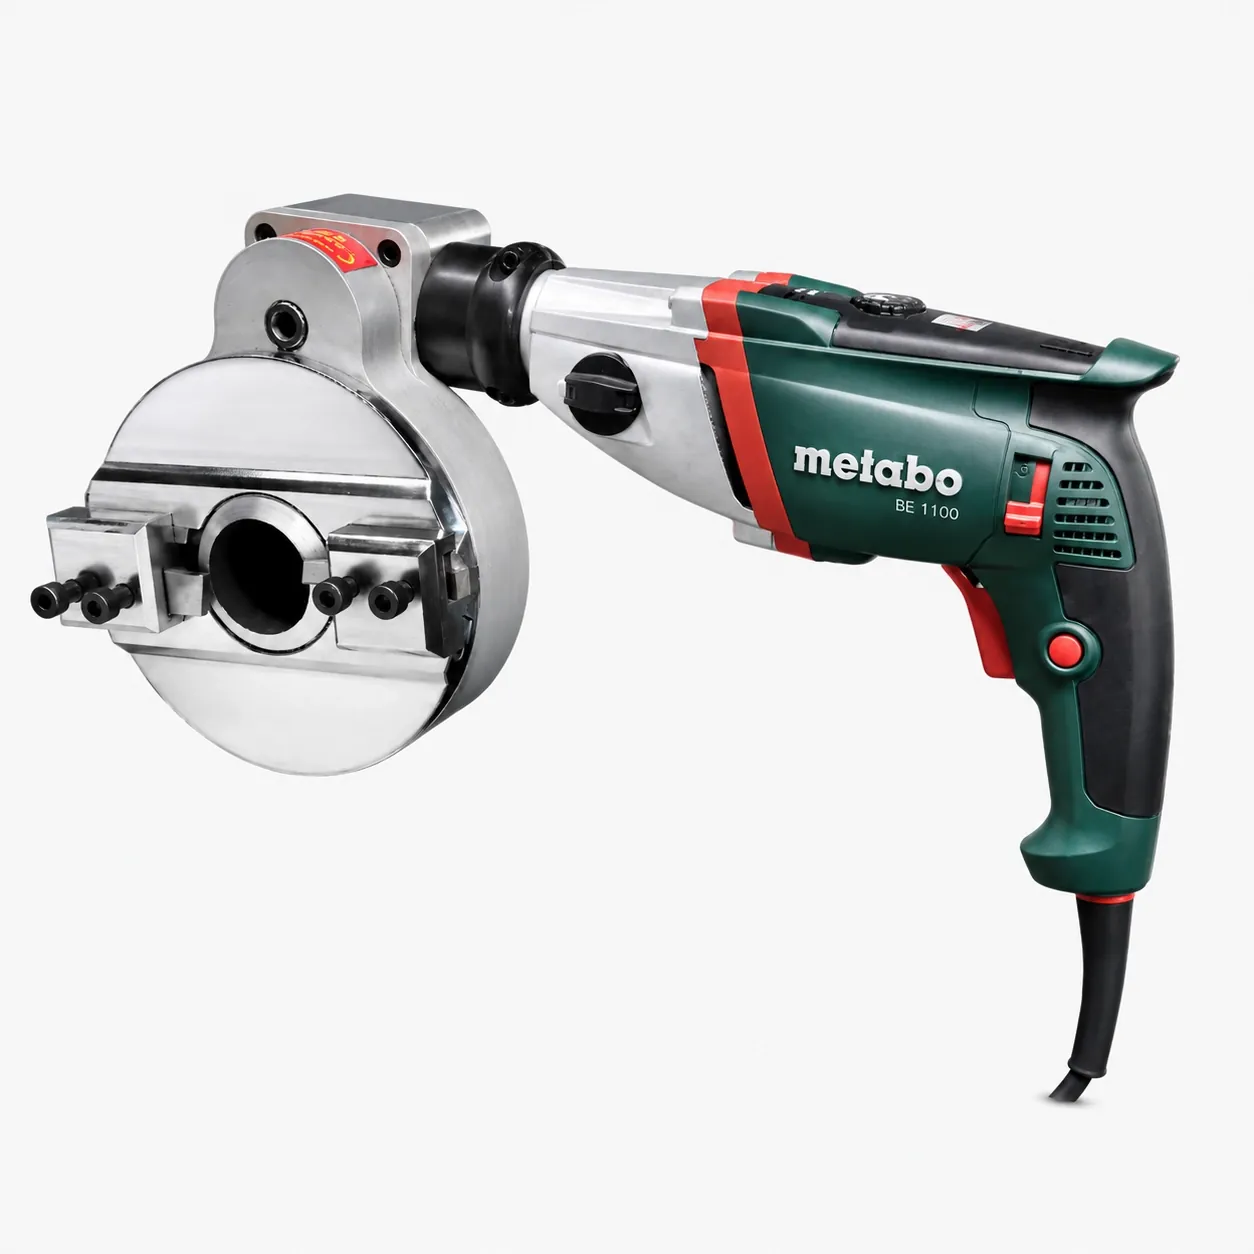
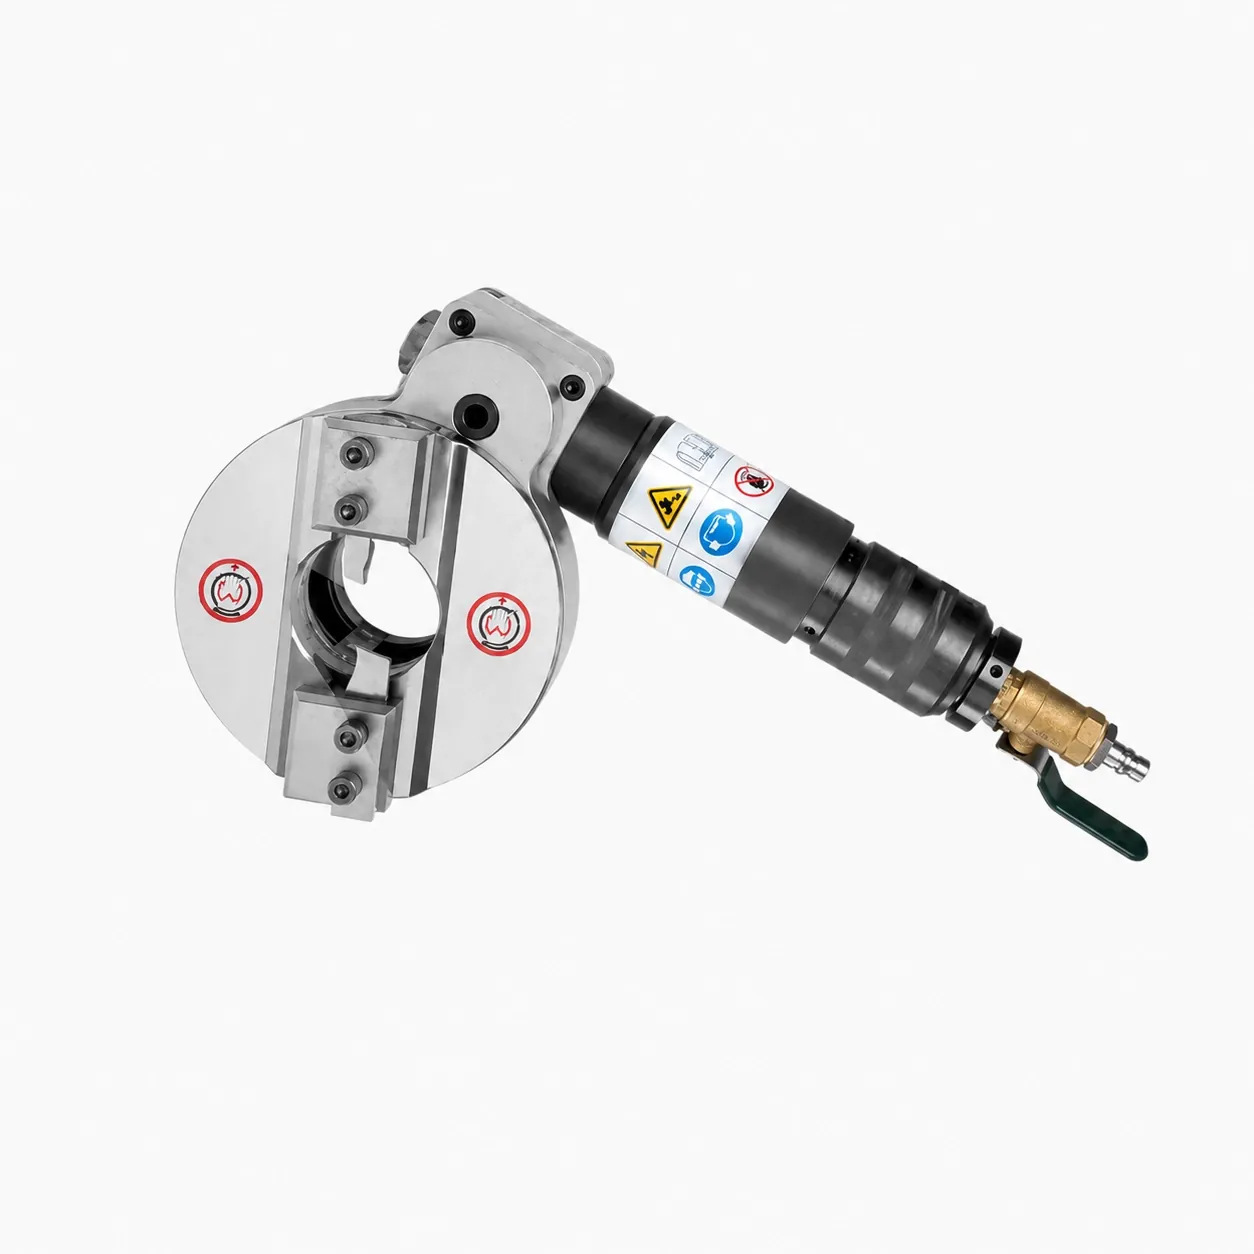
Cam-Type Self-Centering Pipe Beveling Machine
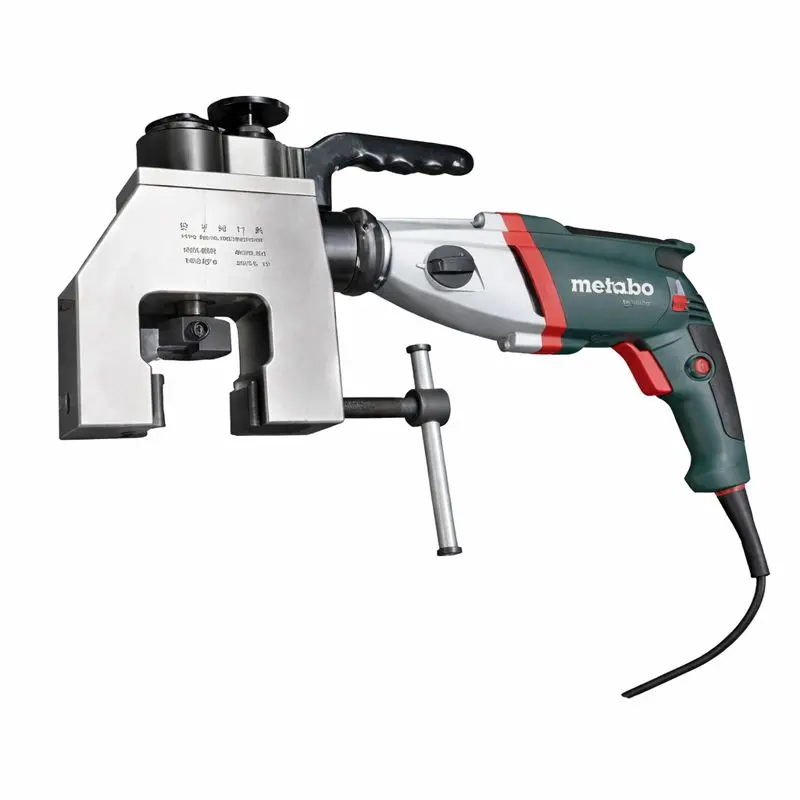
Lightweight aluminum-body cold beveler for small to mid-bore pipe (Ø 14 – 114 mm). Cam-lock self-centering clamp engages in one lever stroke; synchronous feed produces a code-grade weld prep without HAZ.
Pick your size — 2 models in the series.
| SCB / SCP-63 Small bore — 14 to 63 mm | SCB / SCP-114 Mid bore — 57 to 114 mm | |
|---|---|---|
| Pipe OD range | 14 – 63 mm | 57 – 114 mm |
| Wall thickness | ≤ 12 mm | ≤ 12 mm |
| Rotation speed | 30 – 120 r/min | 30 – 120 r/min |
| Drive options | Electric · Pneumatic | Electric · Pneumatic |
| Bevel geometry | V / Y / J | V / Y / J |
| Net weight | 13 kg | 18 kg |
| Recommended use | Overhead, tight access | Service pipe, light HVAC |
| Quote this model |
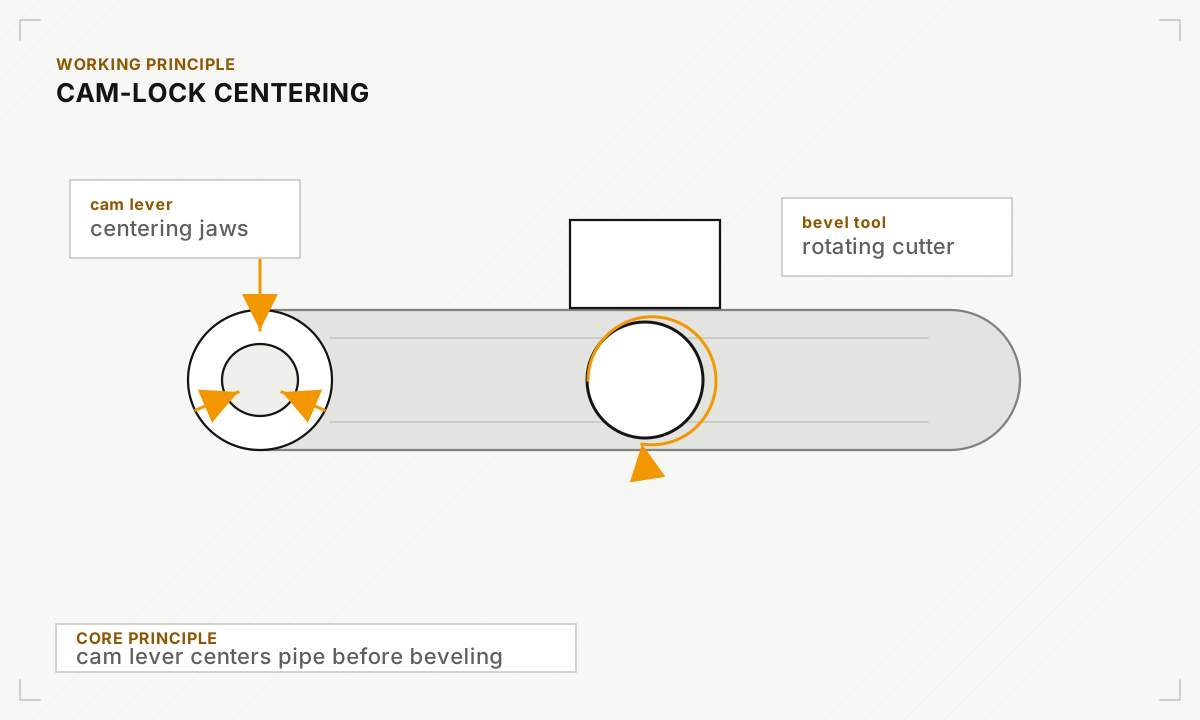
How cam-lock self-centering works
A cam disc rotates around the clamp axis; four contact jaws ride the cam profile and converge on the pipe OD in a single lever stroke. Because all jaws are driven by the same cam surface, the cutting head is concentric to the pipe within ±0.15 mm — without manual indication, even on ovalized or out-of-round service pipe. Feed is mechanically synchronous: 0.05 – 0.20 mm of tool advance per spindle revolution, giving consistent chip load and predictable carbide insert life.
Built for the job site.
Where this series earns its keep.
Chemical & process plant maintenance
On-site weld-prep for small-bore process and instrumentation tubing during shutdown and tie-in work.
Boiler tube replacement
Fast beveling of heat-exchanger and superheater tubes during planned outages, where access windows are measured in hours.
HVAC, plumbing & light fabrication
Production-line bevel prep for small-bore copper, carbon and stainless tube in shop and module-build environments.
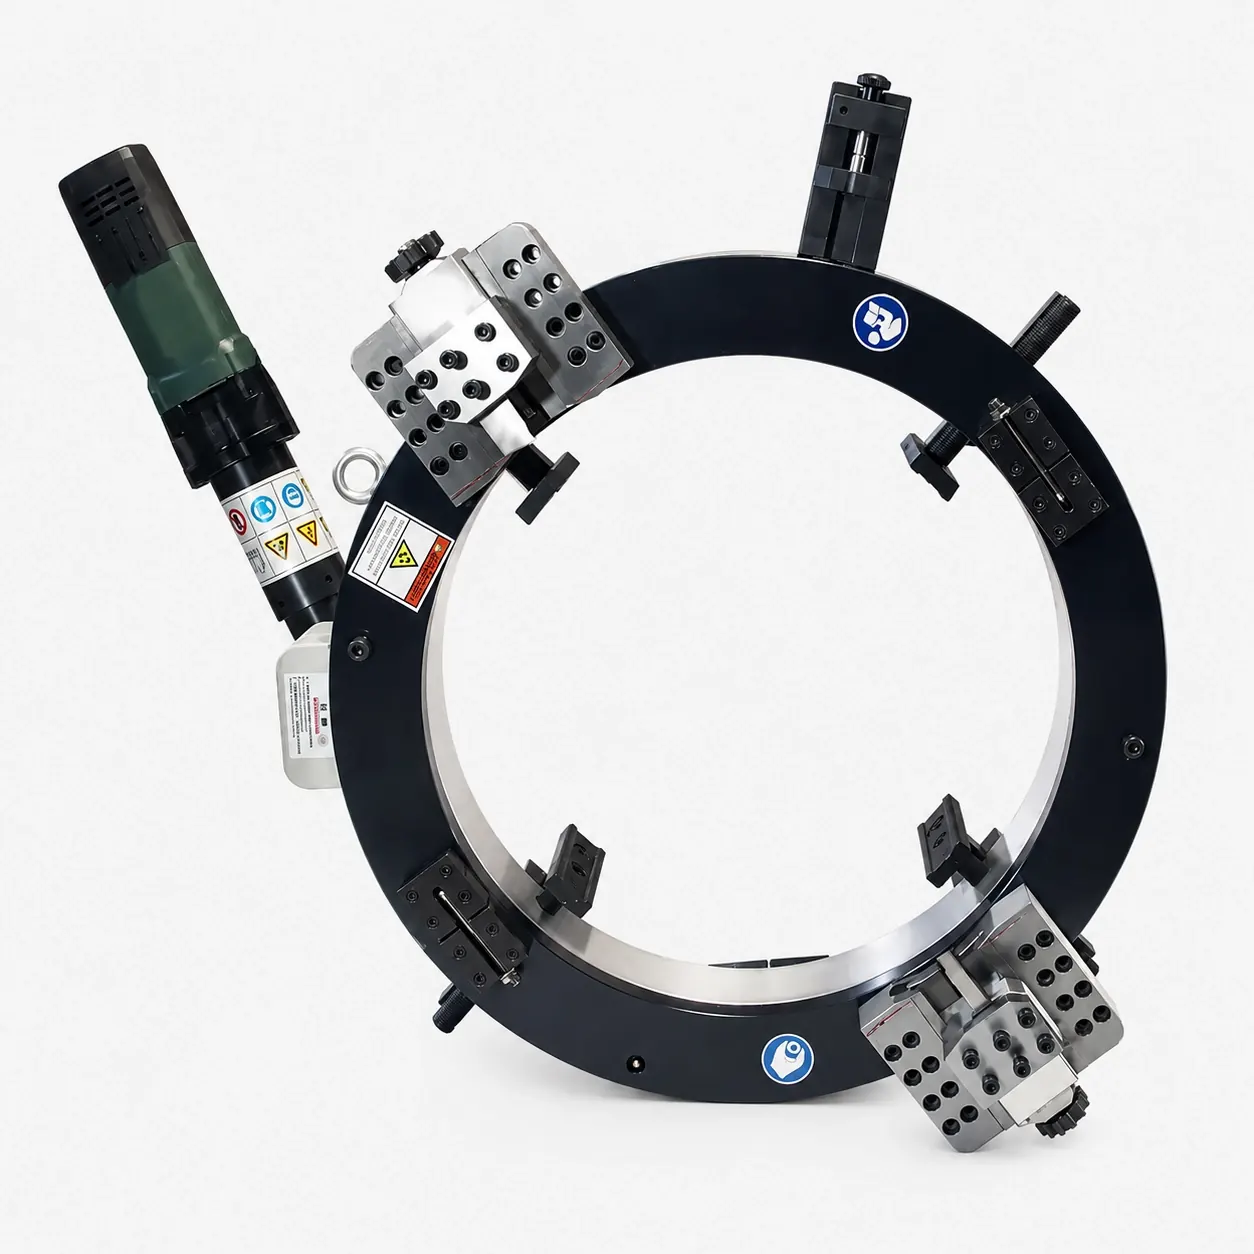
Other pipe beveling machines.
Get a quote within 24 hours.
Send us your spec sheet, pipe schedule, or drawing — our engineers reply with pricing, lead time, and recommended models.
- 01Send specs & drawings
- 02Receive quote within 24h
- 03Confirm & manufacture